Glycine, a crucial amino acid widely used in pharmaceuticals, food additives, and chemical synthesis, often requires efficient and reliable material handling during processing. Pneumatic conveying is a common method for transporting fine powders like glycine, and two primary approaches are widely adopted: negative pressure (or vacuum) conveying and positive pressure conveying. This article provides a detailed comparison of the advantages and disadvantages of these two systems, helping industries select the most suitable option for their glycine handling needs.
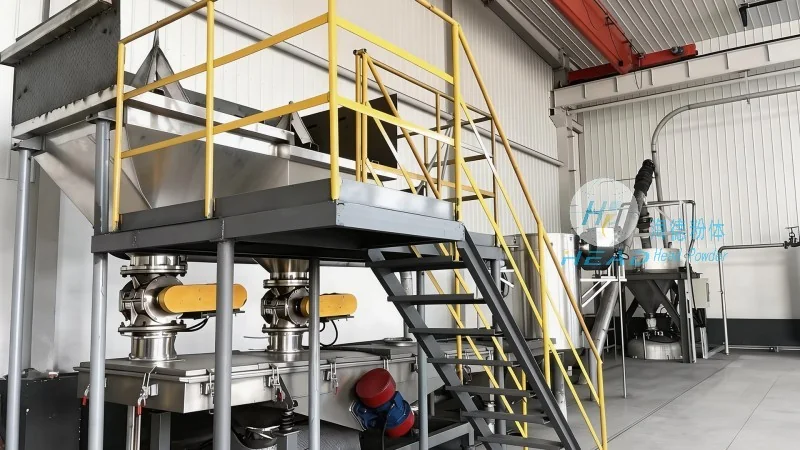
As a leading engineering company in the powder handling industry, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying solutions. With a focus on precision and efficiency, HeadPowder provides customized systems tailored to the unique requirements of clients, including those handling glycine and other fine chemicals. The company’s expertise lies in optimizing material flow, ensuring product integrity, and enhancing operational safety in industrial applications.
Negative pressure conveying, also known as vacuum conveying, operates by creating a low-pressure environment at the receiving end, drawing the material from the source into the conveying line using a vacuum pump. This method is particularly effective for transporting fine powders over moderate distances, as it minimizes product degradation and maintains a clean conveying environment. One of the key advantages of negative pressure systems is their ability to handle sensitive materials like glycine without causing agglomeration or particle breakage. The gentle handling reduces the risk of product contamination and preserves the chemical properties of the material.
However, negative pressure conveying has its limitations. The system typically requires a closed loop, which can be more complex to install and maintain compared to positive pressure systems. Additionally, the vacuum pump must be powerful enough to overcome the resistance of the conveying line and the material’s particle size, potentially leading to higher energy consumption. For long-distance or high-volume transport, the cost and operational complexity may increase, making it less suitable for large-scale glycine production facilities.
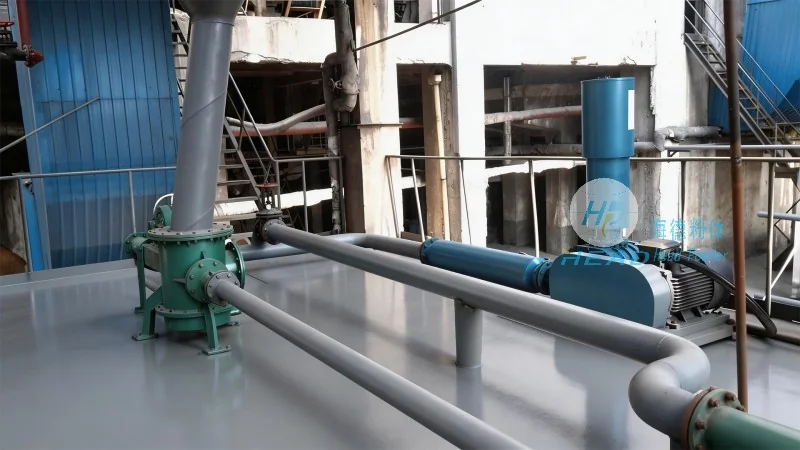
Positive pressure conveying, on the other hand, uses a blower or compressor to generate high-pressure air that pushes the material through the conveying line. This method is ideal for transporting bulk quantities of glycine over longer distances, as it can handle larger particle sizes and higher flow rates. The high-pressure air ensures consistent material flow, reducing the risk of blockages and improving system reliability. A significant advantage of positive pressure systems is their ability to handle abrasive or sticky materials, which are common in glycine processing, without causing excessive wear on the equipment.
Despite its benefits, positive pressure conveying also has drawbacks. The high-pressure air can lead to increased product degradation, especially for heat-sensitive glycine, as the material may be exposed to higher temperatures during transport. Additionally, the system generates more noise and requires regular maintenance of the blower components to prevent wear and tear. The higher energy consumption compared to negative pressure systems is another consideration, as it may increase operational costs for large-scale operations.
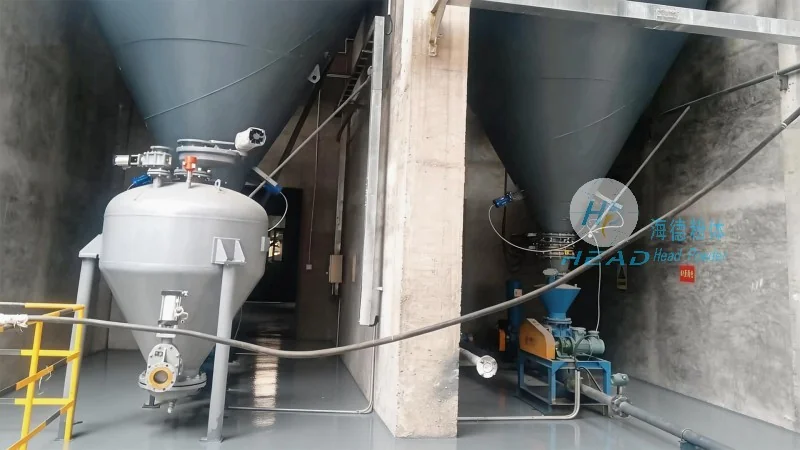
When comparing negative and positive pressure pneumatic conveying for glycine, several factors must be considered. The choice between the two systems depends on the specific application, such as the distance of transport, the volume of material, and the sensitivity of the product. For short-distance transport of fine glycine powders, negative pressure conveying is often preferred due to its gentle handling and low risk of product degradation. Conversely, for long-distance or high-volume transport of bulk glycine, positive pressure conveying may be more economical and efficient.
Cost is another critical factor. Negative pressure systems generally have lower initial installation costs, as they do not require high-pressure blowers. However, the energy consumption and maintenance costs may offset these savings over time. Positive pressure systems, while more expensive to install, can offer lower operational costs for high-volume applications due to their higher efficiency in material handling. The choice also depends on the available space and infrastructure, as negative pressure systems require a closed loop, while positive pressure systems can be more flexible in layout.
Both negative pressure and positive pressure pneumatic conveying systems have their unique advantages and disadvantages when used for glycine handling. The optimal choice depends on the specific requirements of the application, including the distance of transport, the volume of material, and the sensitivity of the product. Shandong HeadPowder Engineering Co., Ltd. offers customized solutions that can be tailored to these needs, ensuring efficient and reliable material handling for glycine and other fine chemicals. By understanding the pros and cons of each system, industries can make informed decisions to enhance their operational efficiency and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top