For industrial applications requiring efficient and reliable coal ash handling, the pneumatic conveying system offers a robust solution. This system is designed to transport coal ash from source points to designated disposal or processing locations with minimal human intervention and optimal performance. The following overview details the key components, operational principles, and benefits of such a system, tailored for clients seeking advanced material handling solutions.
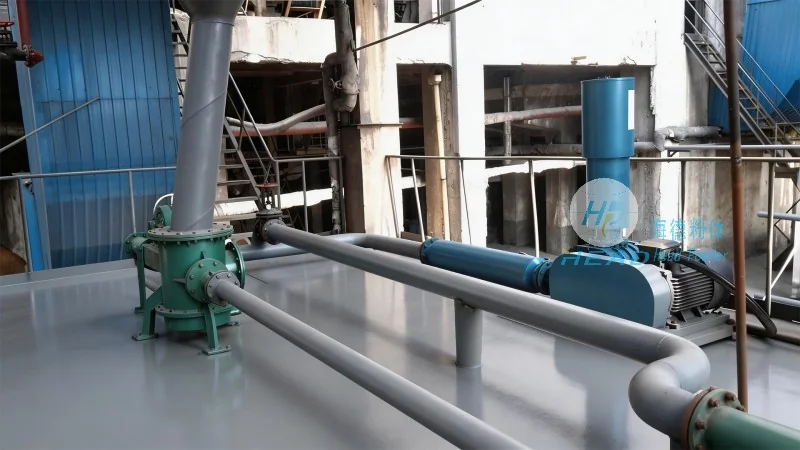
The coal ash pneumatic conveying system comprises several critical components that work in tandem to ensure seamless material transport. At the core is the ash collection hopper, which serves as the initial storage and feeding unit. This hopper is equipped with a rotary valve or feeder that regulates the flow of coal ash into the system, preventing blockages and maintaining consistent feed rates. The feeder ensures that the material is introduced into the conveying line at a controlled pace, which is essential for preventing system overload and optimizing air usage.
Next in the system is the air compressor or blower, which generates the necessary pressure to move the coal ash particles through the pipeline. The choice of compressor depends on the system's capacity and the specific characteristics of the ash, such as particle size and moisture content. High-pressure blowers are commonly used for long-distance or high-capacity applications, while lower-pressure systems may be suitable for shorter distances or less demanding tasks. The compressor is typically equipped with a filter to remove any contaminants from the air, ensuring that the conveying medium remains clean and free from debris that could damage the system or affect performance.
The conveying pipeline itself is a critical component, constructed from materials that can withstand the abrasive nature of coal ash. Common materials include stainless steel, carbon steel, or specialized plastic liners, depending on the system's requirements. The pipeline is designed with smooth, rounded bends and transitions to minimize friction and pressure losses. This design reduces the energy required to move the material and prevents the buildup of ash on the pipe walls, which could lead to blockages or reduced efficiency.
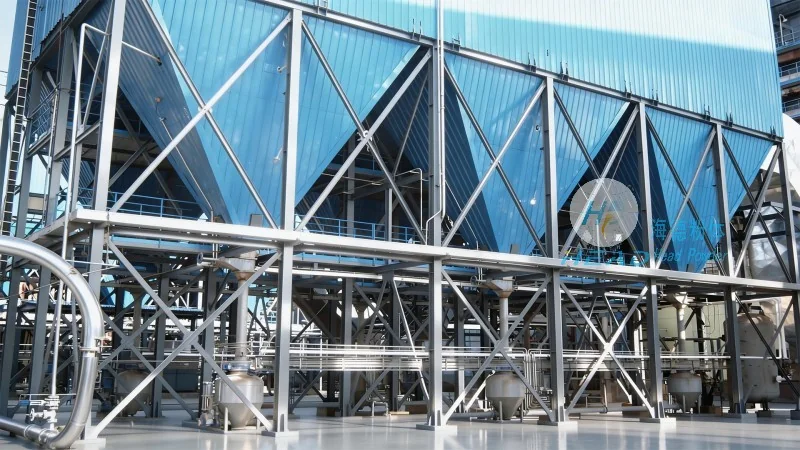
At the receiving end of the system, a dust collector or separator is used to capture the ash particles from the air stream and deposit them into a collection bin or storage container. This component is essential for maintaining air quality and complying with environmental regulations. The dust collector may use cyclonic separation, bag filters, or electrostatic precipitators, depending on the system's capacity and the ash's properties. The collected ash is then transferred to the final disposal or processing facility, completing the material handling cycle.
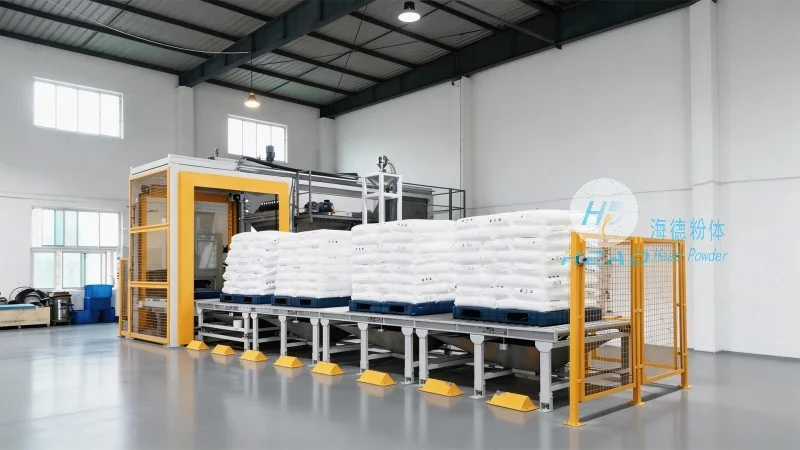
The pneumatic conveying system operates on the principle of air movement, where the ash particles are suspended in a stream of air and propelled through the pipeline. This method is known as dense-phase or dilute-phase conveying, depending on the air-to-material ratio. Dense-phase conveying uses a higher air volume and lower pressure, resulting in a slower, more controlled flow that minimizes particle breakage and reduces wear on the system components. Dilute-phase conveying, on the other hand, uses a lower air volume and higher pressure, allowing for faster transport over longer distances but with a higher risk of particle degradation.
The efficiency of the coal ash pneumatic conveying system is influenced by several factors, including the system's design, the ash's characteristics, and the operational parameters. Proper sizing of the compressor, pipeline diameter, and feeder is crucial for achieving optimal performance. For example, a larger pipeline diameter reduces friction losses and allows for higher material throughput, while a smaller diameter may be more suitable for shorter distances or lower capacity applications. The air pressure and flow rate must be carefully calibrated to match the system's requirements, ensuring that the ash particles are adequately suspended and transported without causing excessive wear or energy consumption.
Regular maintenance is essential to maintain the system's efficiency and longevity. This includes inspecting and cleaning the feeder and pipeline to prevent ash buildup, checking the compressor and filters for wear or contamination, and monitoring the dust collector's performance. By adhering to a regular maintenance schedule, the system can operate at peak efficiency, reducing downtime and minimizing operational costs.
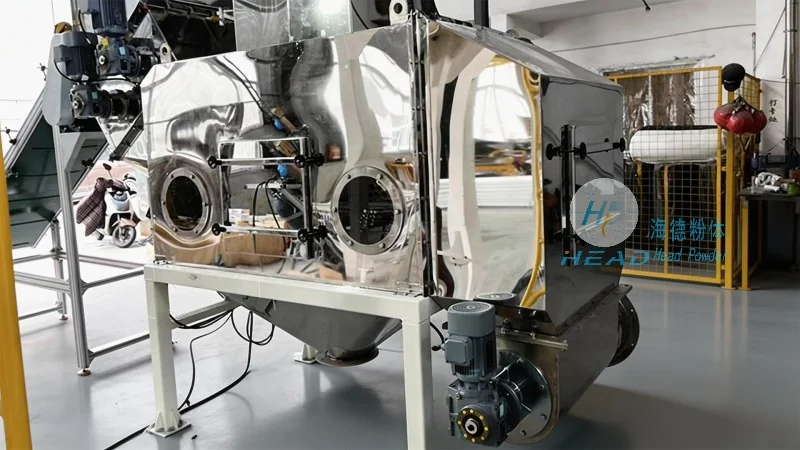
The coal ash pneumatic conveying system offers several advantages over traditional material handling methods, such as belt conveyors or bucket elevators. One of the primary benefits is the ability to transport ash in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important in environments where dust can pose health risks or interfere with other operations. The closed system also helps to maintain the quality of the ash, preventing contamination from external sources and ensuring that the material is handled in a controlled manner.
Another key benefit is the flexibility of the system, which can be adapted to various industrial applications. The system can be used to transport ash from power plants, industrial facilities, or waste management sites to disposal sites, processing plants, or recycling facilities. It can also be integrated with other systems, such as ash dewatering or pelletizing equipment, to create a comprehensive material handling solution. The modular design of the system allows for easy expansion or modification as the client's needs change, providing long-term value and adaptability.
The system's efficiency and reliability also contribute to cost savings for the client. By reducing labor requirements and minimizing downtime, the system can lower operational costs and increase productivity. The closed system also reduces the need for additional dust control measures, such as wet scrubbers or air filters, which can be expensive to install and maintain. Overall, the coal ash pneumatic conveying system provides a cost-effective and sustainable solution for handling coal ash, aligning with the client's operational and environmental goals.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of industrial material handling solutions, including coal ash pneumatic conveying systems. With headquarters in Shandong, China, the company has extensive experience in designing, manufacturing, and installing advanced material handling equipment for various industries. The company's team of engineers and technicians specializes in customizing systems to meet the specific needs of each client, ensuring that the solution is both efficient and cost-effective.
headpowder is committed to providing high-quality products and services, with a focus on innovation and customer satisfaction. The company adheres to international standards and quality control measures to ensure that all products meet the highest industry standards. With a strong reputation for reliability and performance, headpowder has earned the trust of clients worldwide, serving a diverse range of industries including power generation, waste management, and manufacturing.
The company's expertise in coal ash handling systems is a result of years of research and development, as well as practical experience in the field. By leveraging the latest technologies and engineering principles, headpowder has developed systems that are not only efficient but also environmentally friendly. The company's commitment to sustainability and environmental responsibility is reflected in its products, which are designed to minimize the impact on the environment while maximizing operational performance.
For clients seeking a reliable and effective coal ash pneumatic conveying system, headpowder offers comprehensive solutions tailored to their specific requirements. The company's team of experts works closely with clients to understand their needs, design a suitable system, and provide installation and maintenance services. With a focus on quality, innovation, and customer satisfaction, headpowder is the ideal partner for industrial material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top