HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for cereal material handling. This article delves into the fundamental principles behind these systems and highlights key working scenarios where they excel in industrial applications.
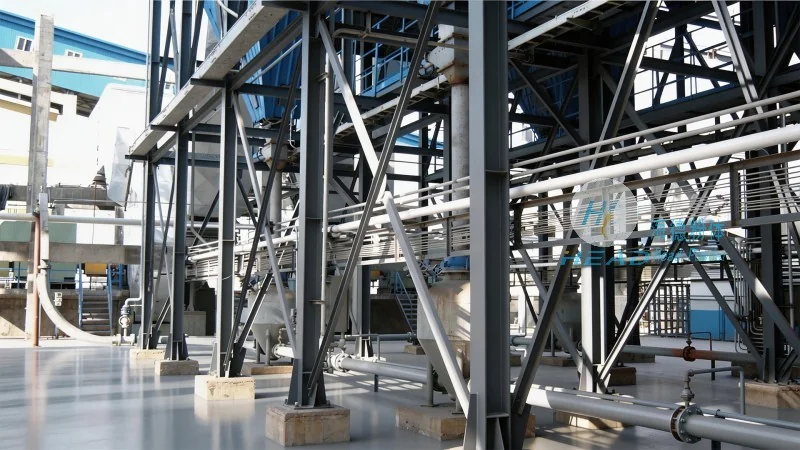
Pneumatic conveying systems utilize air or gas to transport bulk materials like cereal products through a pipeline network. The core principle involves creating a pressure differential that propels the material from the source to the destination. There are primarily two types of pneumatic conveying: pressure and vacuum systems. Pressure systems operate by compressing air and pushing material through the pipeline, while vacuum systems draw material into the system using a vacuum pump. For cereal materials, which often require gentle handling to preserve texture and quality, the choice of system type and design parameters is critical.
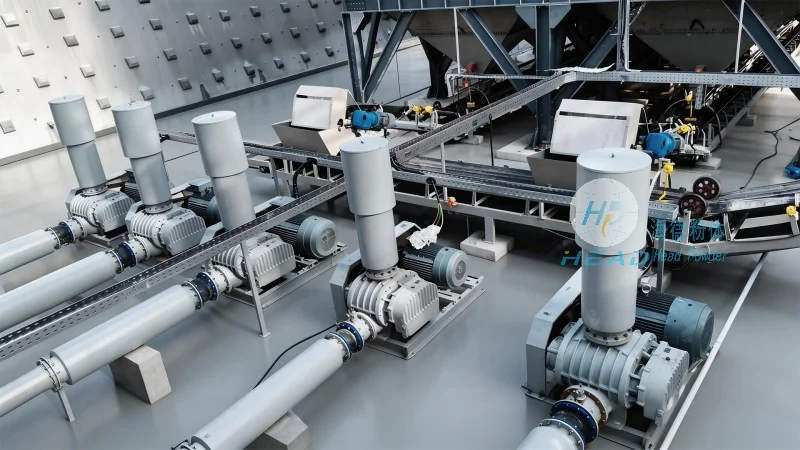
The versatility of cereal material pneumatic conveying systems makes them suitable for a wide range of industrial settings. One common application is in food processing facilities where they are used to transfer raw ingredients such as oats, wheat, or corn from storage silos to production lines. This method ensures a hygienic and efficient transfer process, minimizing contamination risks and maintaining product integrity. Another scenario involves bulk handling in grain elevators and storage facilities, where large volumes of cereal are moved between different storage units or processing stages. The systems can also be integrated into packaging lines, where they transport finished cereal products from packaging machines to storage or shipping areas. Additionally, in agricultural and feed processing industries, these systems are employed to handle raw feed ingredients and transport them to mixing or processing units, supporting efficient livestock feed production.
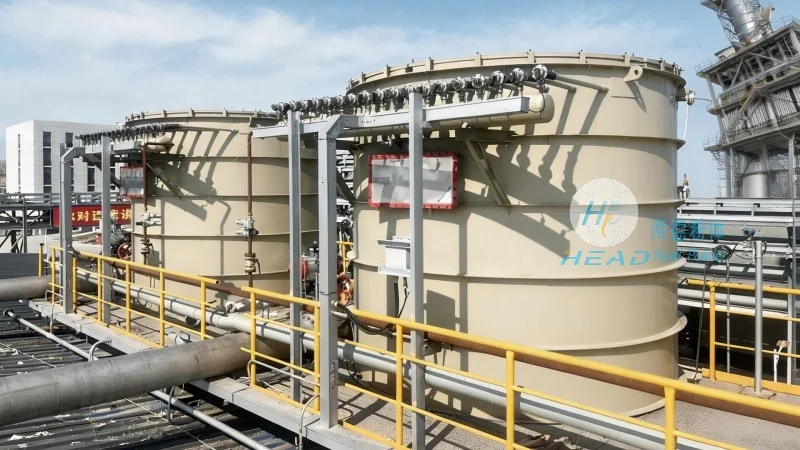
Implementing pneumatic conveying systems for cereal materials offers several distinct advantages. Firstly, they provide a dust-free and enclosed transfer process, which is essential for maintaining product quality and adhering to food safety regulations. Unlike traditional belt or bucket elevators, pneumatic systems minimize exposure to airborne particles, reducing the risk of contamination and improving overall hygiene. Secondly, these systems offer high efficiency in material transport, capable of moving large volumes of cereal over significant distances with minimal energy consumption compared to other bulk handling methods. The gentle handling of materials by air flow helps preserve the texture and nutritional value of cereals, which is particularly important for products like oats or whole grain items. Furthermore, the modular design of pneumatic conveying systems allows for easy integration with existing production lines and flexible adjustments to accommodate varying material flow rates. This adaptability makes them suitable for both new installations and retrofits in existing facilities.
The successful operation of cereal material pneumatic conveying systems depends on careful consideration of several technical factors. Material properties, such as particle size, density, and moisture content, play a crucial role in determining the appropriate system design. For example, finer particles may require higher air velocities to prevent blockages, while larger or denser particles might need more robust pipeline and valve components. The system's pressure and vacuum levels must be optimized to ensure efficient transport without causing excessive wear on components or compromising material quality. HeadPowder's engineering expertise ensures that each system is tailored to the specific characteristics of the cereal material being handled, incorporating the latest technologies to enhance performance and reliability. The company's design process involves detailed analysis of the material's flow characteristics, system layout, and operational requirements to deliver customized solutions that meet the unique needs of each client.
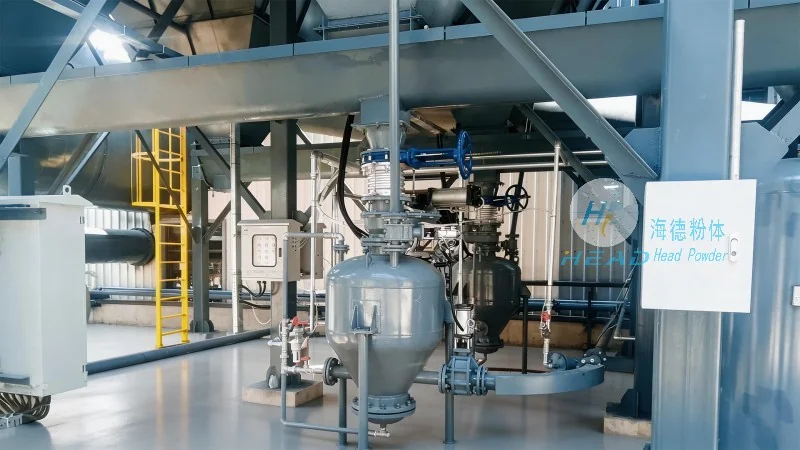
HeadPowder's pneumatic conveying systems for cereal materials represent a sophisticated solution for efficient and hygienic bulk handling in various industrial applications. By leveraging the principles of pneumatic transport, these systems offer significant advantages in terms of product quality preservation, operational efficiency, and system flexibility. As a trusted manufacturer based in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving demands of the food processing and agricultural industries. The company's commitment to quality and customer satisfaction ensures that its pneumatic conveying systems remain a reliable choice for businesses seeking to optimize their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top