Carbon fiber pneumatic conveying systems represent a sophisticated solution for material handling, particularly in industries requiring high efficiency and precision. These systems utilize compressed air to transport bulk materials through a network of pipes and components, offering a clean and efficient alternative to traditional mechanical conveying methods. The design and functionality of such systems are critical to their performance, making an understanding of their structure and operational principles essential for potential users and industry professionals.
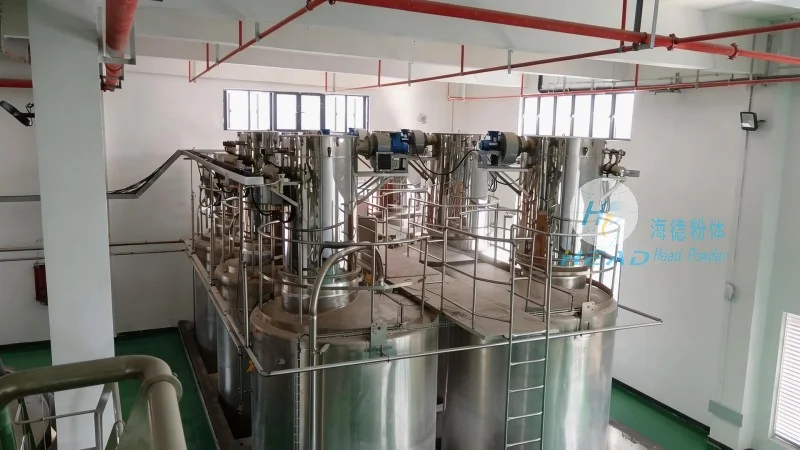
At the core of carbon fiber pneumatic conveying systems is the ability to transport dry bulk materials over varying distances with minimal maintenance and operational complexity. These systems are widely adopted in sectors like pharmaceuticals, food processing, and chemical manufacturing, where material purity and contamination control are paramount. The use of carbon fiber in the construction of these systems provides several advantages, including high strength-to-weight ratios, excellent corrosion resistance, and thermal stability, which are crucial for maintaining material integrity during transport.
The structure of a carbon fiber pneumatic conveying system typically comprises several integral components, each playing a vital role in the overall operation. The primary components include the air compressor, which generates the necessary pressure for material transport; the material feed hopper, where bulk material is introduced into the system; the conveying pipes, which form the pathway for material movement; and the control valves and regulators, which manage air flow and pressure. Additionally, the system may incorporate cyclone separators or filters to separate conveyed material from air at the discharge end, ensuring clean air release and material recovery.
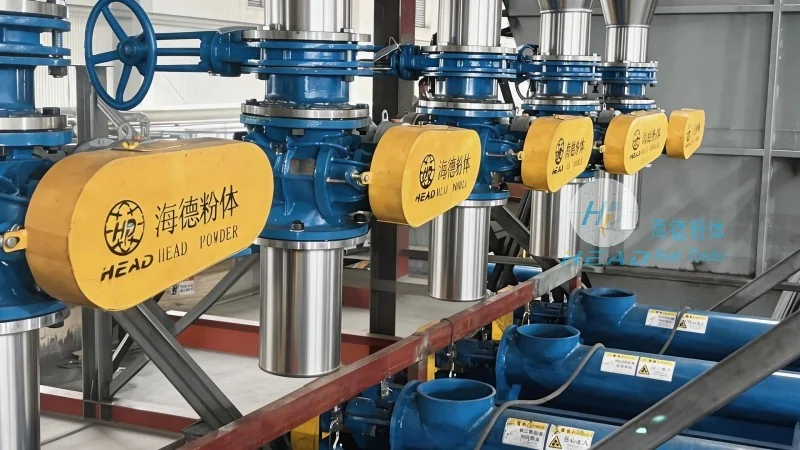
The operational principle of a carbon fiber pneumatic conveying system involves the introduction of bulk material into the feed hopper, where it is then drawn into the conveying pipes by the high-pressure air generated by the compressor. As the material is entrained by the air stream, it travels through the pipeline network, maintaining a consistent flow rate and velocity. At the discharge point, the material is separated from the air using a cyclone or other separation device, allowing the material to be collected in a designated container while the air is either filtered or released. The entire process is controlled by a series of valves and sensors that monitor pressure, flow, and material level, ensuring optimal performance and safety.
The adoption of carbon fiber in the construction of pneumatic conveying systems offers significant benefits over traditional materials like metal or plastic. Carbon fiber's high strength and lightweight nature reduce the overall weight of the system, making it easier to install and maintain. Its excellent corrosion resistance minimizes the risk of material degradation or contamination, which is critical in industries where product purity is non-negotiable. Furthermore, carbon fiber's thermal stability allows the system to operate under a wide range of temperatures without compromising performance or structural integrity. These advantages contribute to longer service life, lower maintenance costs, and enhanced operational efficiency.
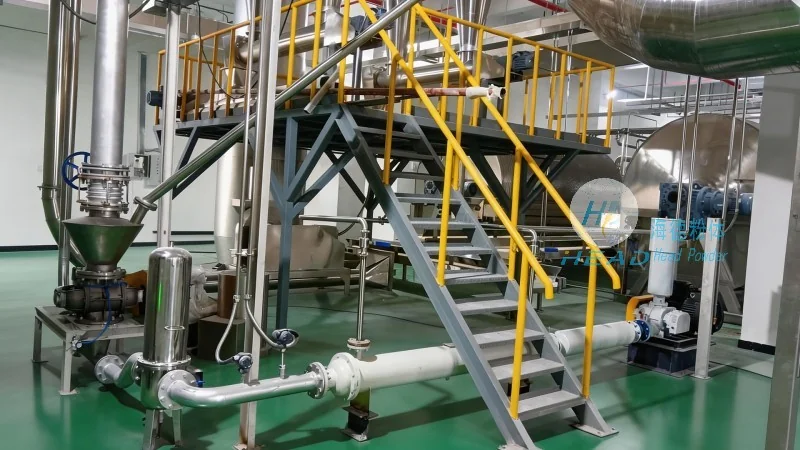
Carbon fiber pneumatic conveying systems are employed in a variety of applications across different industries. In the pharmaceutical sector, they are used to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring strict contamination control and maintaining product quality. In food processing, these systems handle powders and granules, such as spices, flour, and sugar, while adhering to stringent hygiene standards. The chemical industry also benefits from these systems when handling corrosive or abrasive materials, as carbon fiber's resistance to chemical attack and wear makes it an ideal choice. Additionally, in the aerospace and advanced manufacturing sectors, carbon fiber conveying systems are used for transporting high-value materials like nanomaterials and specialty powders, where precision and purity are essential.
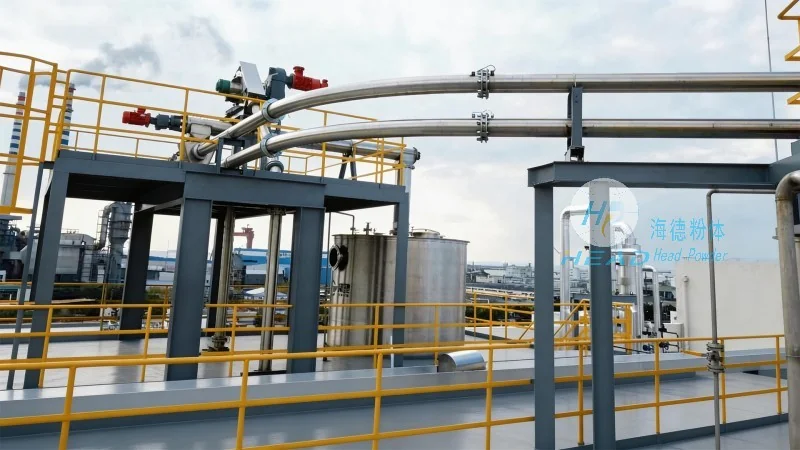
Proper maintenance and operational practices are essential to maximize the lifespan and efficiency of carbon fiber pneumatic conveying systems. Regular inspections of components such as the air compressor, feed hopper, and conveying pipes are necessary to identify and address any wear or damage. Cleaning the system, particularly the cyclone separators and filters, is crucial to prevent clogging and maintain optimal performance. Additionally, monitoring air pressure and flow rates helps ensure that the system operates within its designed parameters, preventing overloading or underperformance. By adhering to these maintenance guidelines, users can extend the service life of their systems and minimize downtime, ensuring consistent and reliable material transport.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of material handling equipment, specializes in the design, development, and production of carbon fiber pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries seeking advanced and reliable material transport solutions. HeadPowder's expertise in carbon fiber technology and pneumatic conveying systems has enabled them to deliver products that meet the highest standards of performance, durability, and safety. The company's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing equipment and a team of skilled engineers and technicians dedicated to delivering superior products and services to clients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top