For industries dealing with bulk materials like brown sugar, efficient and reliable material handling is crucial. The pneumatic conveying system, particularly designed for transporting brown sugar, offers a solution that combines precision, hygiene, and operational efficiency. This article provides an overview of the brown sugar pneumatic conveying system, detailing its structural components and the underlying principles that enable smooth material transport.
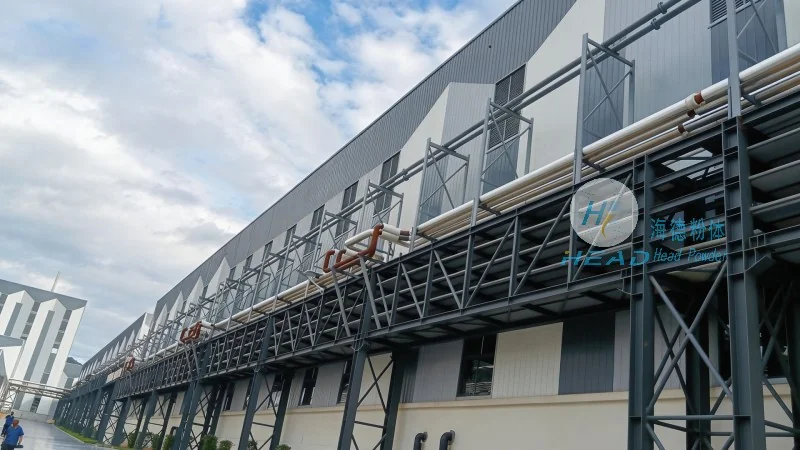
The brown sugar pneumatic conveying system is built upon several key components that work in tandem to achieve effective material transfer. The primary elements include the hopper, which serves as the initial storage and feeding unit, ensuring a consistent flow of brown sugar into the system. The hopper is typically equipped with a feeding mechanism, such as a rotary valve or a screw feeder, which regulates the material discharge rate. This control is vital for maintaining the system's performance and preventing blockages or overloading.
Next, the conveying line itself is a critical component. It consists of a pipeline system that transports the brown sugar from the hopper to the discharge point. The pipeline is usually made of materials like stainless steel or food-grade plastic, chosen for their durability and resistance to corrosion and contamination. The choice of material is essential for maintaining the quality of the brown sugar, as any exposure to impurities could affect its taste and quality. Additionally, the pipeline may include bends and elbows, which are designed to guide the material smoothly through the system without causing excessive pressure drops or turbulence.
The air supply system is another vital part of the brown sugar pneumatic conveying system. It generates the necessary airflow to move the brown sugar particles through the pipeline. This system typically includes a blower or a compressor, which provides the required pressure and volume of air. The air is then introduced into the pipeline, creating a flow that carries the brown sugar particles. The air velocity and pressure are carefully controlled to ensure that the brown sugar is conveyed efficiently without causing excessive wear on the system components or damaging the material.
The discharge unit is the final component of the system, where the brown sugar is released from the pipeline. This unit may include a receiver or a storage tank, which collects the conveyed brown sugar. The discharge mechanism, such as a rotary valve or a gate valve, controls the flow of material out of the system. Proper design of the discharge unit is essential to prevent material buildup and ensure a smooth, continuous flow. The receiver is often equipped with a cleaning system to maintain hygiene and prevent contamination, which is particularly important in food processing applications.
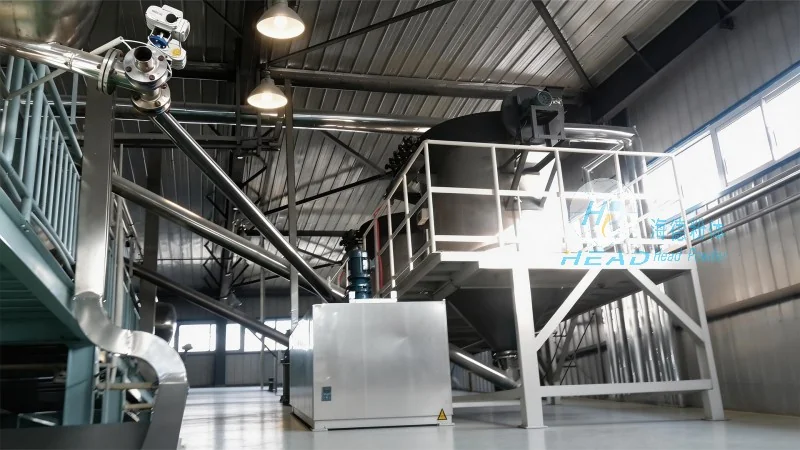
The operation of the brown sugar pneumatic conveying system is based on the principles of fluid dynamics and particle transport. The system relies on the movement of air to carry the brown sugar particles through the pipeline. When the air is introduced into the pipeline, it creates a low-pressure zone that draws the brown sugar particles into the air stream. The particles are then carried along with the air, moving through the pipeline to the discharge point. The velocity of the air is a key factor in determining the efficiency of the conveying process. If the air velocity is too low, the brown sugar particles may settle and cause blockages. Conversely, if the air velocity is too high, it can lead to excessive wear on the system components and energy consumption.
The system operates in either positive or negative pressure modes. In positive pressure mode, the blower or compressor pressurizes the pipeline, forcing the air and brown sugar particles through the system. This mode is often used for short-distance conveying or when the material needs to be transported to a higher elevation. In negative pressure mode, the system creates a vacuum in the pipeline, drawing the brown sugar particles into the air stream. This mode is commonly used for long-distance conveying or when the material needs to be transported to a lower elevation. The choice between positive and negative pressure depends on the specific application and the requirements of the brown sugar handling process.
The conveying process also involves the separation of the brown sugar particles from the air. At the discharge point, the air is typically filtered and vented, while the brown sugar particles are collected in the receiver. The separation is achieved through the use of cyclones or filters, which remove the particles from the air stream. The efficiency of the separation process is crucial for maintaining the quality of the brown sugar and preventing contamination. Proper maintenance of the separation equipment is essential to ensure consistent performance and prevent downtime.
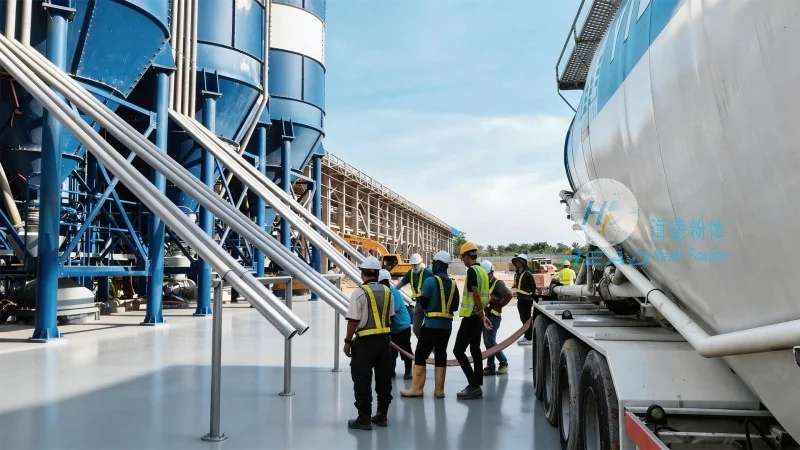
Implementing a brown sugar pneumatic conveying system offers several advantages over traditional material handling methods. One of the primary benefits is the ability to handle the material in a closed system, which enhances hygiene and prevents contamination. This is particularly important in the food industry, where maintaining the quality and safety of the product is paramount. The closed system also reduces the risk of dust exposure, which can be a health hazard for workers and can affect the quality of the brown sugar.
Another advantage is the flexibility and scalability of the system. The pneumatic conveying system can be easily adapted to different production volumes and conveying distances. It can be expanded or modified to accommodate changes in the brown sugar handling process, making it a cost-effective solution for growing businesses. The system also allows for the integration of other equipment, such as mixers or classifiers, to enhance the overall processing capabilities.
The efficiency and reliability of the brown sugar pneumatic conveying system are also significant advantages. The system can operate continuously with minimal downtime, ensuring a steady supply of brown sugar to the production line. The use of automated controls and sensors allows for real-time monitoring of the system's performance, enabling quick detection and resolution of any issues. This reduces the risk of production delays and minimizes the need for manual intervention, improving overall operational efficiency.
Furthermore, the system is energy-efficient compared to traditional methods like bucket elevators or belt conveyors. The use of air as the conveying medium reduces the energy consumption and wear on the system components. The lower maintenance requirements and longer service life of the components also contribute to the overall cost savings. The system's ability to handle the brown sugar in a gentle manner, without causing excessive friction or impact, helps preserve the quality and texture of the product, which is essential for maintaining customer satisfaction.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top