Lightweight aggregate pneumatic conveying lines are a critical component in material handling systems, particularly for transporting lightweight aggregates such as expanded clay, perlite, or vermiculite. These systems utilize air pressure to move bulk materials through a network of pipes, offering a flexible and efficient solution for industrial applications. This article delves into the operation process and working principle of such lines, highlighting key components, operational steps, and technical aspects that ensure reliable and effective material transport.
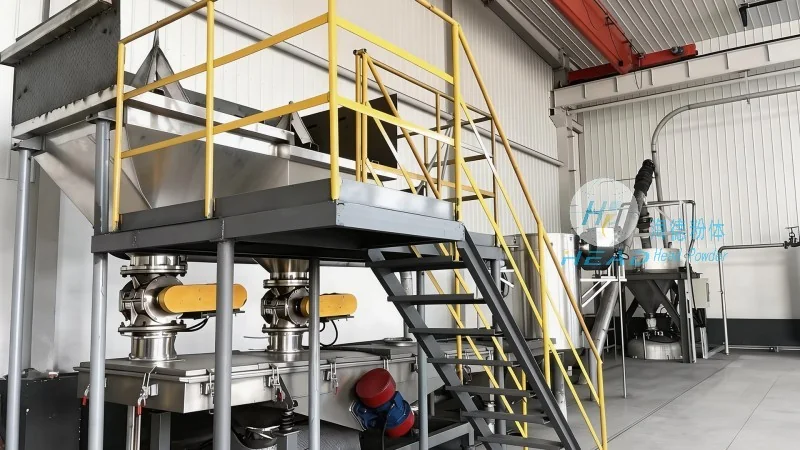
HeadPowder, a leading manufacturer in material handling equipment, specializes in designing and manufacturing high-quality pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for industries requiring efficient and reliable material transport solutions. The company’s headquarters is located in Shandong, China, where it leverages advanced technology and expertise to develop cutting-edge pneumatic conveying lines tailored to diverse industrial needs.
The operation of a lightweight aggregate pneumatic conveying line relies on several critical components that work in harmony to achieve efficient material transport. These components include the material hopper (serving as storage and feeding unit), the air compressor (generating necessary air pressure), the conveying pipes (forming the main transport pathway), the control valves (regulating air flow and pressure), and the dust collector (ensuring air purification and environmental compliance). Each component plays a vital role in maintaining system performance and safety.
The operation process of a lightweight aggregate pneumatic conveying line typically involves sequential steps. First, lightweight aggregate is fed into the material hopper from a storage silo or batch container. The hopper is equipped with a feeder mechanism (e.g., rotary valve or screw conveyor) to control material flow rate into the conveying line. Next, the air compressor starts and generates compressed air, which is directed into the conveying pipes. Compressed air creates a pressure differential, drawing lightweight aggregate particles into the pipe and transporting them to the destination point. Control valves adjust air pressure and flow rate to ensure optimal material transport without blockages or excessive energy use. Finally, material is discharged from the receiving hopper at the end of the line for further processing or use.
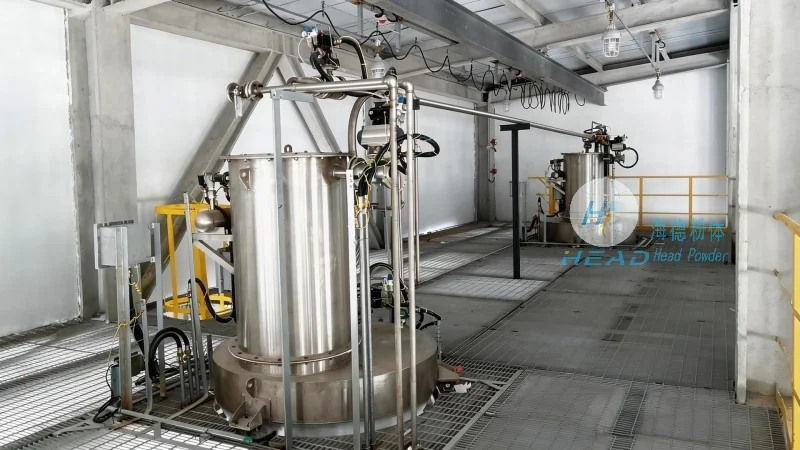
The working principle of a lightweight aggregate pneumatic conveying line is based on fluid dynamics and particle transport. Compressed air introduces a low-pressure zone that pulls lightweight aggregate particles into the flow. Air velocity is maintained to keep particles suspended and prevent settling or sticking to pipe walls. This suspension is achieved by balancing air flow rate with material flow rate. The system operates under positive or negative pressure, depending on application needs. Positive pressure systems use compressed air to push material forward, while negative pressure systems use suction to draw material. Both methods are effective, with the choice depending on factors like transport distance, material type, and system layout.
Lightweight aggregate pneumatic conveying lines offer advantages over traditional methods like belt conveyors or bucket elevators. Key benefits include flexible system layout (horizontal, vertical, or inclined paths to accommodate complex plant designs), dust-free and clean transport (critical for product quality and environmental compliance), and ability to handle diverse materials (including high-moisture or abrasive aggregates without damage). Energy efficiency is another advantage, as these systems transport materials over long distances with minimal energy consumption compared to other methods.
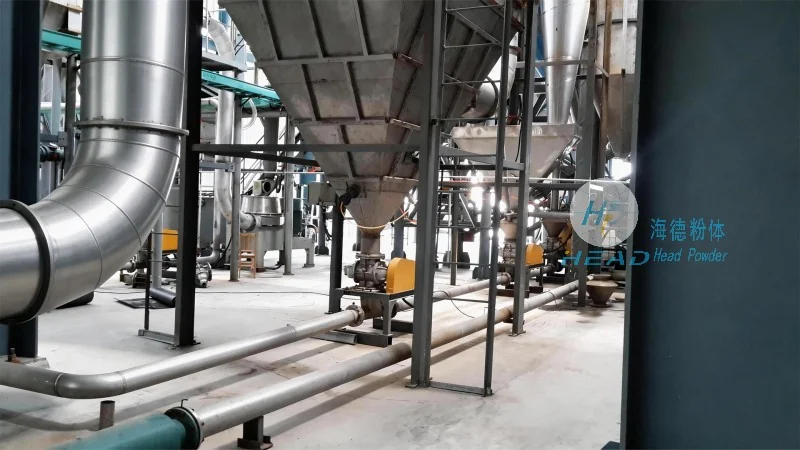
Lightweight aggregate pneumatic conveying lines are widely used in industries requiring bulk material transport. These include construction (expanded clay aggregates for concrete production), agriculture (perlite and vermiculite as soil amendments), and chemicals (lightweight aggregates for insulation materials). The system’s versatility in handling different materials and adapting to industrial processes makes it a valuable solution for material handling needs.
Regular maintenance is essential for reliable operation of lightweight aggregate pneumatic conveying lines. This includes checking the air compressor for proper pressure/flow, inspecting conveying pipes for blockages/wear, and cleaning the dust collector for air quality. Common issues like material buildup in pipes (caused by insufficient air flow or high moisture) can be resolved by adjusting air pressure/flow or using cleaning mechanisms (e.g., pulse jet systems). Timely maintenance and troubleshooting minimize downtime and maximize system efficiency.
Lightweight aggregate pneumatic conveying lines are a sophisticated and efficient solution for material handling in various industrial applications. Understanding the operation process and working principle of these systems helps optimize material transport operations, improve productivity, and ensure environmental compliance. With expertise from companies like Shandong HeadPowder Engineering Co., Ltd., industries benefit from reliable and high-performance pneumatic conveying systems tailored to specific requirements. Continuous technological advancements further enhance system capabilities, making them indispensable in modern material handling infrastructure.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top