Quartz stone material handling systems are specialized equipment designed to transport and manage quartz stone materials efficiently in industrial settings. These systems are crucial for applications ranging from raw material processing to finished product delivery, ensuring smooth workflow and operational efficiency. The design of such systems is tailored to the unique properties of quartz stone, including its hardness, weight, and handling requirements.
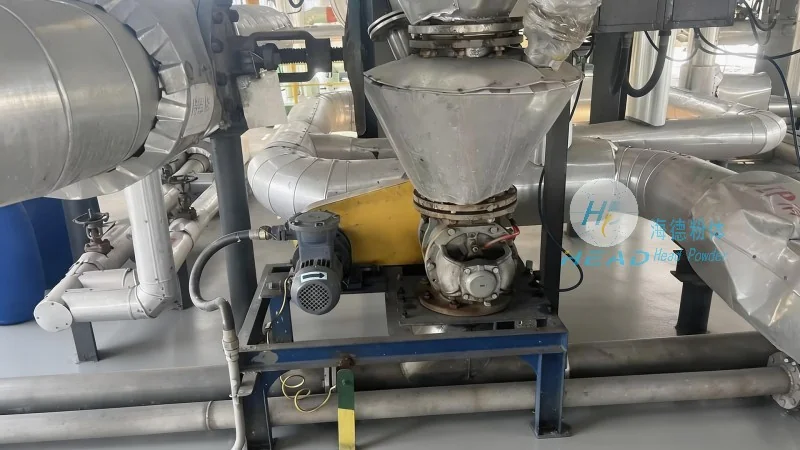
The core components of a quartz stone material handling system typically include feeders, conveyors, elevators, and sorting mechanisms. Each component plays a vital role in the overall operation. Feeders are used to control the flow of quartz stone from storage or processing areas, ensuring a consistent and controlled feed rate. Conveyors, often in the form of belt or chain systems, transport the material horizontally or at an incline. Elevators, such as bucket or screw conveyors, are employed to lift the material vertically, facilitating vertical movement within the system. Sorting mechanisms may be integrated to separate different sizes or grades of quartz stone, enhancing the system's versatility and adaptability.
The design principles of quartz stone material handling systems prioritize durability, efficiency, and safety. Due to the abrasive nature of quartz stone, components like belts, chains, and bearings are constructed from high-quality materials, such as stainless steel or specialized alloys, to withstand wear and tear. The system's layout is carefully planned to minimize material handling time and energy consumption. This involves optimizing the path of the material, reducing unnecessary movements, and integrating energy-efficient motors and drives. Additionally, safety features, including emergency stop mechanisms, protective guards, and load sensors, are incorporated to protect operators and prevent accidents.
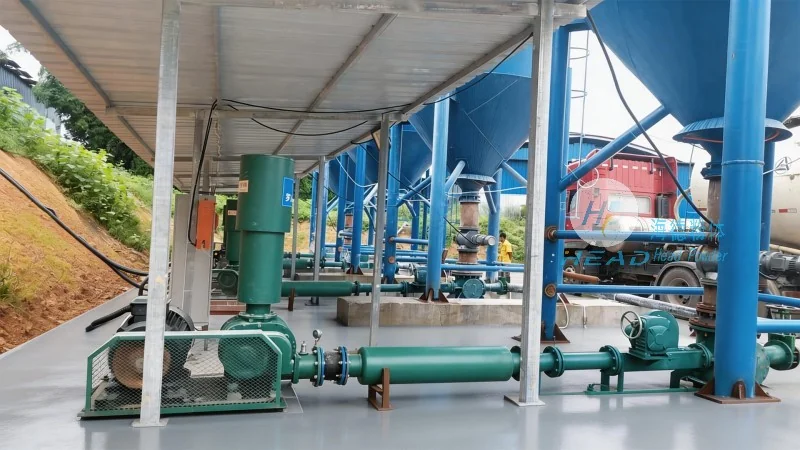
Quartz stone material handling systems find applications in various industries, including construction, manufacturing, and mining. In the construction industry, these systems are used to transport quartz stone for countertop production, flooring, and other building materials. In manufacturing, they facilitate the movement of quartz stone from raw material storage to processing machines, streamlining production lines. The benefits of these systems include increased productivity, reduced labor costs, improved material quality control, and enhanced workplace safety. By automating the material handling process, companies can achieve higher throughput and maintain consistent product quality.
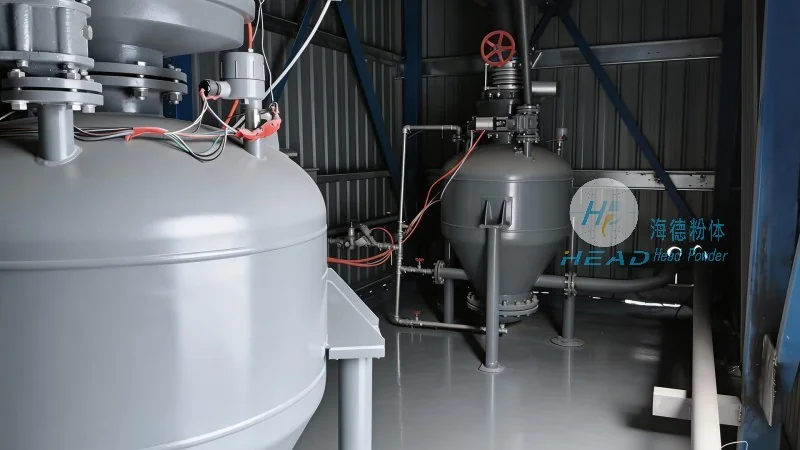
Quartz stone material handling systems can be customized to meet specific operational needs. Manufacturers often offer modular designs that allow for easy integration with existing production lines or storage facilities. This flexibility enables businesses to adapt the system to changing production requirements or expand their operations without significant disruptions. Customization may include adjustments to conveyor speed, capacity, or the addition of specialized features like dust collection systems or material sorting capabilities. The ability to integrate seamlessly with existing infrastructure is a key advantage, as it minimizes downtime and ensures a smooth transition to automated material handling.
Proper maintenance is essential to ensure the longevity and efficiency of quartz stone material handling systems. Regular inspections, cleaning, and lubrication of components are necessary to prevent wear and maintain optimal performance. Operators should be trained on the proper use and maintenance of the system to avoid damage and ensure safety. Additionally, monitoring system performance through sensors and data analysis can help identify potential issues before they become major problems. By adhering to a comprehensive maintenance schedule and operational guidelines, businesses can maximize the lifespan of their material handling systems and minimize downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top