Corn cob material handling systems are critical components in various industrial and agricultural applications, particularly in processes involving the processing of corn cobs for use as animal feed, biofuel, or other value-added products. These systems are designed to efficiently transport, store, and manage corn cob materials from the initial collection stage through to the final processing stage. Understanding the functionality and design principles of such systems is essential for optimizing operational efficiency and ensuring consistent product quality.
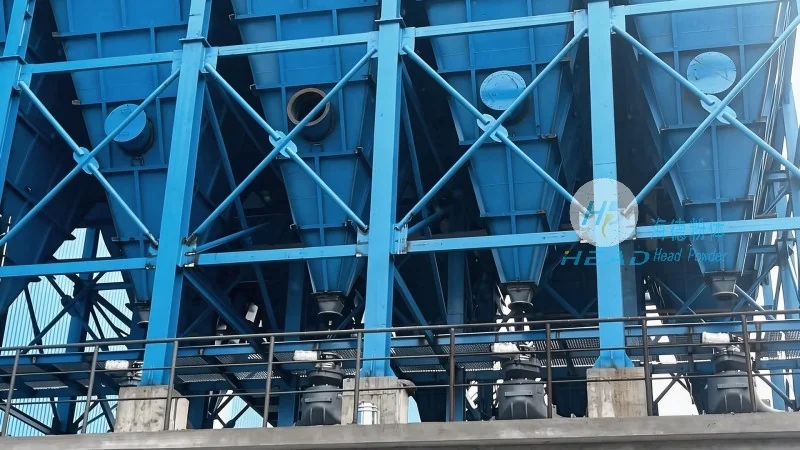
Corn cobs, the stalks of corn plants, are rich in fiber and nutrients, making them valuable raw materials in the production of animal feed, ethanol, and other biomass-based products. However, due to their irregular shape, high moisture content, and abrasive nature, handling corn cobs requires specialized equipment to prevent material degradation, equipment wear, and operational inefficiencies. A corn cob material handling system typically integrates multiple components, including feeders, conveyors, storage silos, and processing units, to streamline the material flow and enhance overall productivity.
HeadPowder, a prominent engineering company based in Shandong, China, specializes in the design, manufacturing, and supply of advanced material handling systems tailored to the unique needs of corn cob processing industries. With years of experience in the field, HeadPowder has developed a comprehensive range of solutions that address the challenges associated with corn cob handling, such as material segregation, dust control, and energy efficiency. The company's commitment to innovation and customer satisfaction has positioned it as a trusted partner for businesses seeking reliable and efficient material handling solutions.
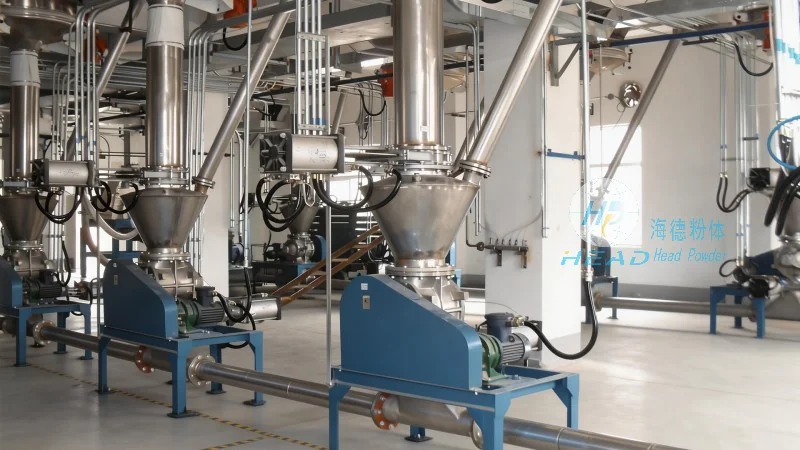
The design of a corn cob material handling system is guided by several key principles aimed at maximizing performance, durability, and safety. One of the primary considerations is the selection of appropriate conveyor types, such as screw conveyors, belt conveyors, or pneumatic systems, based on the specific characteristics of the corn cob material and the operational requirements. Screw conveyors, for instance, are commonly used for horizontal or slight incline transport due to their ability to handle bulk materials with minimal spillage and effective sealing. Belt conveyors, on the other hand, are suitable for longer distances and higher throughput, providing a cost-effective solution for large-scale corn cob handling.
Another critical design principle is the incorporation of robust sealing and dust control mechanisms. Corn cobs are prone to generating dust, which can pose health and safety risks and affect the quality of downstream products. Therefore, systems often include enclosed conveyor sections, dust collection systems, and air filtration units to minimize dust emissions and maintain a clean working environment. Additionally, the design emphasizes the use of wear-resistant materials, such as stainless steel or special alloys, for components that come into direct contact with the corn cob material to extend equipment lifespan and reduce maintenance costs.
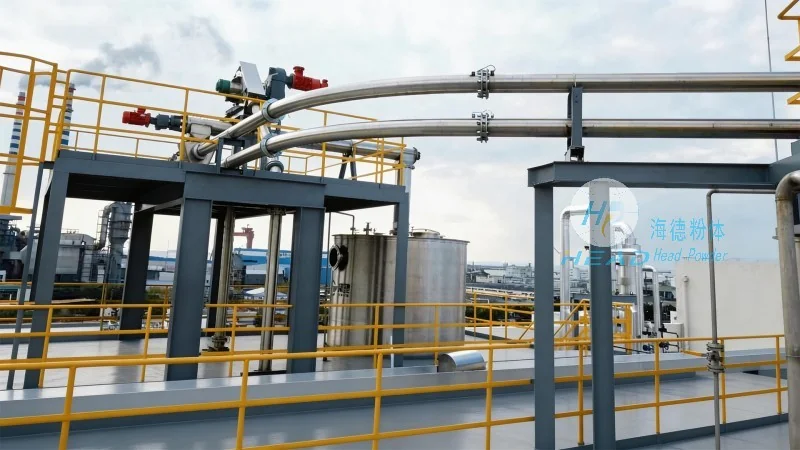
HeadPowder's corn cob material handling systems are engineered with several features that enhance their performance and reliability. These systems are designed to handle varying moisture contents and particle sizes, ensuring consistent material flow and preventing blockages or jams. The integration of variable speed drives allows for precise control over conveyor speed, enabling operators to adjust the system's output based on production demands. Furthermore, the systems are equipped with advanced monitoring and control systems, including sensors and automation controls, to optimize operational efficiency and reduce downtime.
One of the significant advantages of HeadPowder's solutions is their adaptability to different processing requirements. Whether for feed production, biofuel processing, or other applications, the systems can be customized to meet specific operational needs, such as varying throughput rates, material handling capacities, or integration with existing processing lines. The company's expertise in material handling technology ensures that each system is tailored to the unique challenges of corn cob processing, resulting in improved productivity and reduced operational costs.
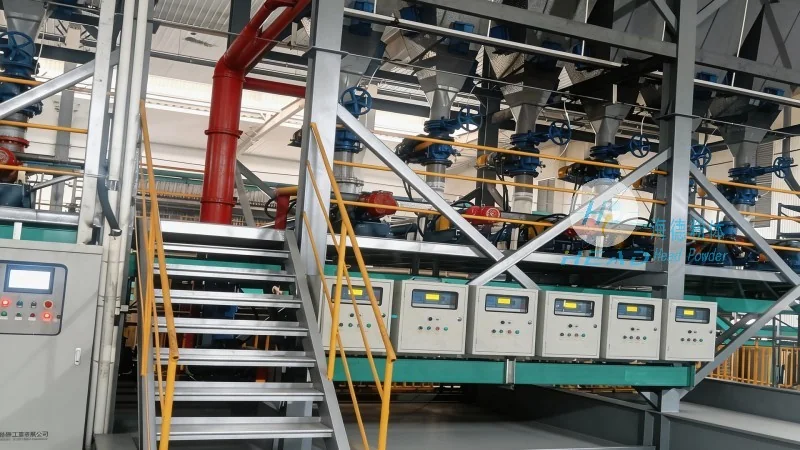
Corn cob material handling systems are widely used in various industries, including animal feed manufacturing, biofuel production, and agricultural processing. In animal feed production, these systems facilitate the efficient transport of corn cobs from storage to processing units, ensuring a steady supply of raw materials for feed formulation. In biofuel industries, the systems play a crucial role in moving corn cobs to ethanol or biogas production facilities, where they are converted into renewable energy sources. Additionally, the systems are utilized in agricultural processing plants for the production of corn cob-based products, such as fiberboard or other composite materials.
The versatility of corn cob material handling systems makes them essential in modern industrial operations, where efficiency and sustainability are paramount. By optimizing material flow and reducing waste, these systems contribute to the overall sustainability of corn cob processing, aligning with the growing demand for eco-friendly and resource-efficient industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top