When it comes to the efficient and safe transport of hematite using pneumatic conveying systems, one of the most critical challenges is managing dust leakage. Hematite, a key iron ore with a fine, powdery texture, can easily generate airborne particles during handling, posing risks to both equipment integrity and worker health. For industries relying on consistent material flow and environmental compliance, preventing dust leakage becomes a top priority. This article explores the strategies and technologies developed by Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) to address these challenges, ensuring reliable operation of pneumatic conveying systems for hematite transport.
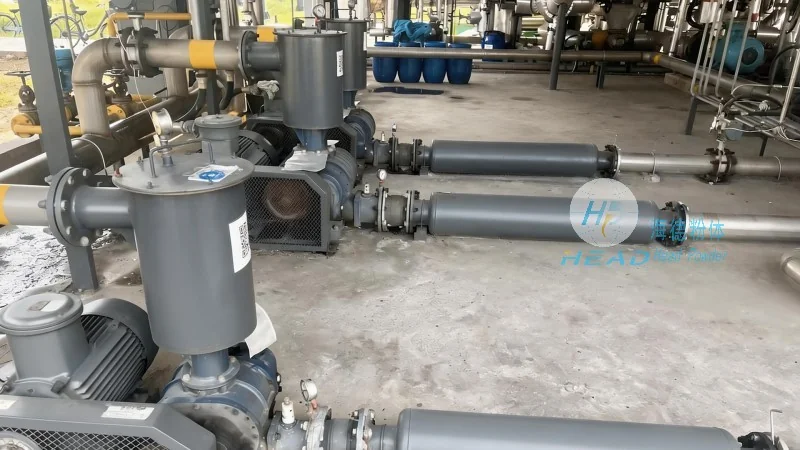
Pneumatic conveying systems are widely used in the mining and processing industries to move bulk materials like hematite from one location to another. However, the fine nature of hematite makes it prone to generating dust during loading, conveying, and unloading. Dust leakage can lead to equipment wear, reduced system efficiency, and even health hazards for personnel. Additionally, regulatory requirements for air quality and environmental protection demand strict control over dust emissions. Therefore, implementing effective dust control measures is essential for maintaining operational safety and compliance.
Dust leakage in pneumatic conveying systems occurs due to several factors, including material properties, system design, and operational conditions. Hematite’s high moisture content or low bulk density can cause it to flow poorly, leading to blockages and increased pressure differentials that force dust through seals and joints. Poorly maintained equipment, such as worn-out seals or damaged hoppers, can also contribute to leakage. The consequences of uncontrolled dust leakage extend beyond operational issues; it can result in product loss, increased maintenance costs, and potential legal penalties for non-compliance with environmental standards. Recognizing these risks is the first step toward developing effective prevention strategies.
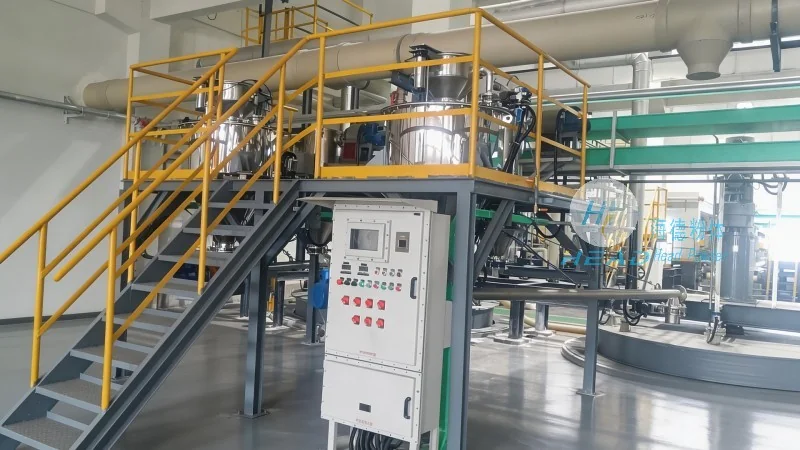
As a leading engineering company specializing in bulk material handling, HeadPowder has developed advanced solutions to mitigate dust leakage in pneumatic conveying systems for hematite. Our approach combines state-of-the-art technology with tailored engineering to address the unique challenges of hematite transport. By focusing on system design, material handling, and maintenance, we ensure that our clients achieve optimal performance while minimizing environmental impact. HeadPowder’s expertise lies in creating customized pneumatic conveying systems that are specifically designed to handle hematite’s characteristics, reducing the likelihood of dust leakage and improving overall operational efficiency.
Our pneumatic conveying systems for hematite are equipped with several key features that enhance dust control and system reliability. First, we use high-quality, dust-tight hoppers and feeders that are designed to minimize material spillage and prevent dust ingress. These components are constructed from durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the abrasive nature of hematite. Second, our systems incorporate advanced sealing technologies, including double-seal mechanisms and airlock valves, to prevent air and dust from escaping. These seals are regularly inspected and maintained to ensure they remain effective over time. Third, we employ energy-efficient blowers and filters that capture and recycle dust, reducing emissions and improving system performance. By integrating these features, our systems provide a robust solution for hematite transport while maintaining compliance with environmental regulations.
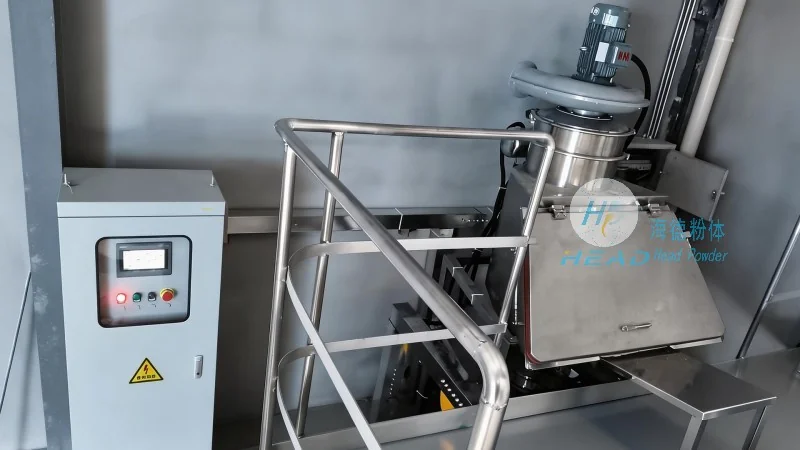
HeadPowder employs a multi-faceted approach to minimize dust emissions from pneumatic conveying systems. One key strategy is the use of positive pressure conveying, which maintains a slight positive pressure within the system to prevent external air from entering and carrying dust out. This method is particularly effective for handling fine materials like hematite, as it reduces the risk of dust being drawn into the system. Another approach is the implementation of cyclone separators and bag filters, which capture dust particles before they are released into the environment. These filtration systems are designed to handle high volumes of dust and maintain consistent performance, even under varying operational conditions. Additionally, we recommend regular maintenance schedules, including cleaning of filters and inspection of seals, to ensure that the system operates at peak efficiency. By combining these technical approaches, HeadPowder’s solutions effectively reduce dust leakage and improve the overall sustainability of hematite transport operations.
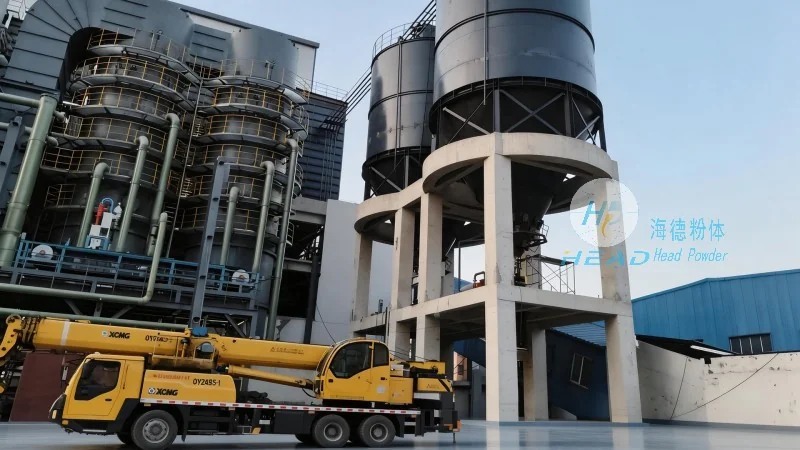
HeadPowder has successfully implemented its dust control solutions in various hematite processing facilities across China. For example, a major mining company in Shandong province reduced dust leakage by 85% after upgrading to our pneumatic conveying system. The system included upgraded hoppers with double-seal mechanisms and cyclone separators, which significantly improved air quality in the plant and reduced maintenance costs. Another client, a steel manufacturing facility, reported increased material flow rates and reduced downtime after installing our energy-efficient blowers and filter systems. These case studies demonstrate the effectiveness of HeadPowder’s solutions in real-world applications, providing tangible benefits for clients in terms of operational efficiency and environmental compliance.
Compliance with environmental regulations is a critical consideration for industries handling hematite. HeadPowder’s pneumatic conveying systems are designed to meet or exceed local and international standards for dust emissions. By using advanced filtration and sealing technologies, our systems help clients avoid fines and maintain a positive public image. Additionally, our solutions enhance operational efficiency by reducing downtime caused by equipment wear and maintenance. The durability of our components and the reliability of our systems ensure that clients can achieve consistent material flow and minimize disruptions. HeadPowder’s commitment to quality and innovation ensures that our clients receive not only effective dust control solutions but also long-term value and support.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top