HeadPowder, a leading provider in the field, specializes in the design and manufacturing of advanced pneumatic conveying systems for sodium bicarbonate powder. This article delves into the operational process and underlying principles of such equipment, offering a comprehensive understanding for industry professionals and potential clients.
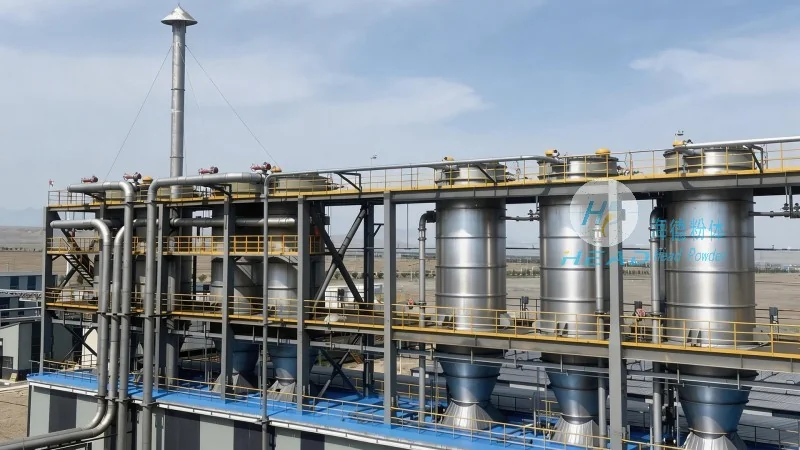
The pneumatic conveying system for sodium bicarbonate powder typically consists of several key components, including a hopper, feeder, air compressor, conveying line, and receiver. The working principle revolves around the use of compressed air to create a flow that transports the powder particles through the system. When the feeder releases the powder into the hopper, the air compressor generates a high-pressure air stream. This air stream, combined with the powder, forms a slurry that moves through the conveying line under pressure. The receiver then collects the powder as the air pressure decreases, allowing the powder to settle and be discharged.
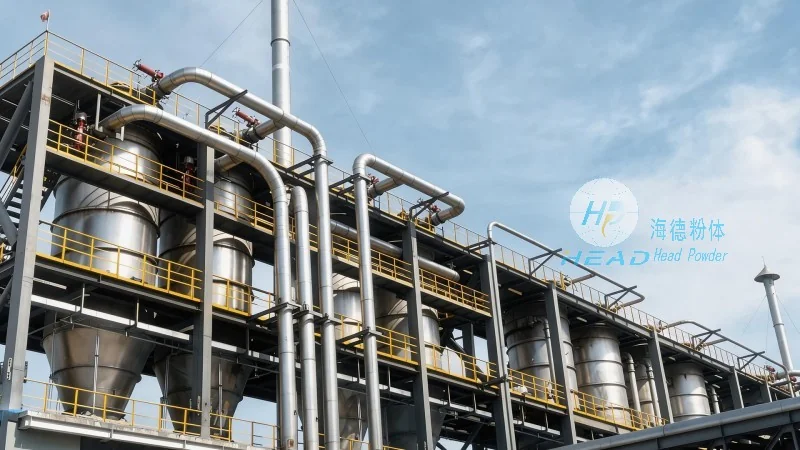
The operation of the sodium bicarbonate powder pneumatic conveying equipment follows a systematic sequence to ensure efficient and reliable transport. Initially, the powder is stored in the hopper, which is equipped with a level indicator to monitor the material volume. The feeder then regulates the flow rate of the powder into the conveying line, ensuring a consistent feed. The air compressor, often a positive displacement type, supplies the necessary air pressure, typically ranging from 0.5 to 1.0 MPa, depending on the system design and material characteristics. As the compressed air enters the conveying line, it mixes with the powder, creating a dense phase flow. This flow travels through the pipeline, overcoming resistance from bends, valves, and other components. Upon reaching the receiver, the air pressure is reduced, causing the powder to separate from the air and settle in the receiver's container. The air, now filtered to remove any residual powder particles, is discharged to the atmosphere or recirculated if the system is designed for that purpose.
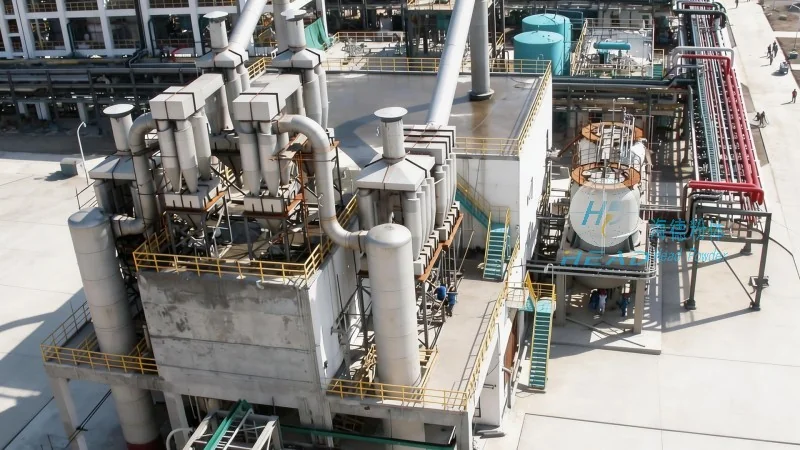
HeadPowder's pneumatic conveying systems for sodium bicarbonate powder offer several advantages that enhance performance and reliability. The dense phase conveying method minimizes particle degradation and agglomeration, preserving the quality of the powder. The system is also capable of handling varying particle sizes and moisture content, making it versatile for different applications. Additionally, the equipment is designed for easy maintenance and cleaning, with components that can be easily accessed and serviced. The use of high-quality materials, such as stainless steel for the conveying line and hopper, ensures durability and resistance to corrosion, which is crucial for handling sodium bicarbonate powder that may be slightly alkaline.
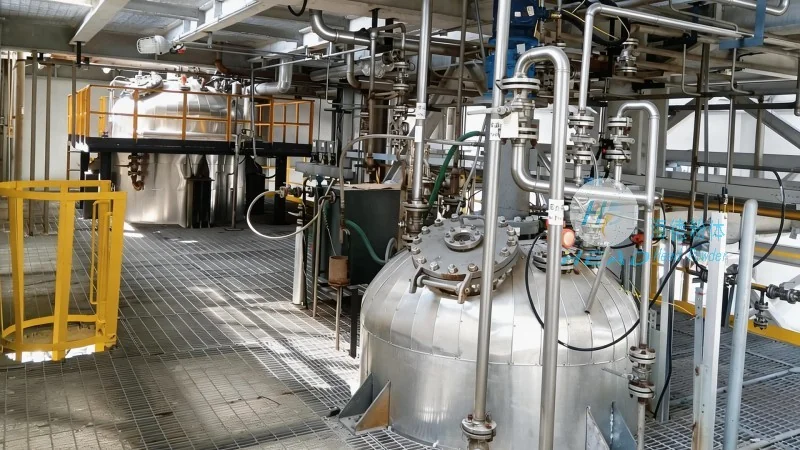
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer specializing in industrial conveying solutions. With years of experience in the field, the company has developed a strong reputation for producing high-quality pneumatic conveying equipment tailored to the needs of various industries. The company's commitment to innovation and customer satisfaction has enabled it to serve a wide range of clients, from chemical and food processing to pharmaceutical and manufacturing sectors. HeadPowder's products are designed to meet international standards and are backed by comprehensive technical support and after-sales service.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top