Lightweight aggregate material handling equipment is a specialized system engineered to transport and manage lightweight aggregates, including expanded clay, perlite, vermiculite, and other low-density construction materials. These materials are prized in construction, insulation, and industrial applications for their exceptional thermal insulation properties and reduced structural weight. The equipment is essential for ensuring efficient, safe, and consistent material handling from storage to processing and delivery, addressing the unique challenges posed by lightweight, often dusty, and granular materials. Manufactured by Shandong HeadPowder Engineering Co., Ltd., this equipment is designed to meet the demands of modern industrial operations.
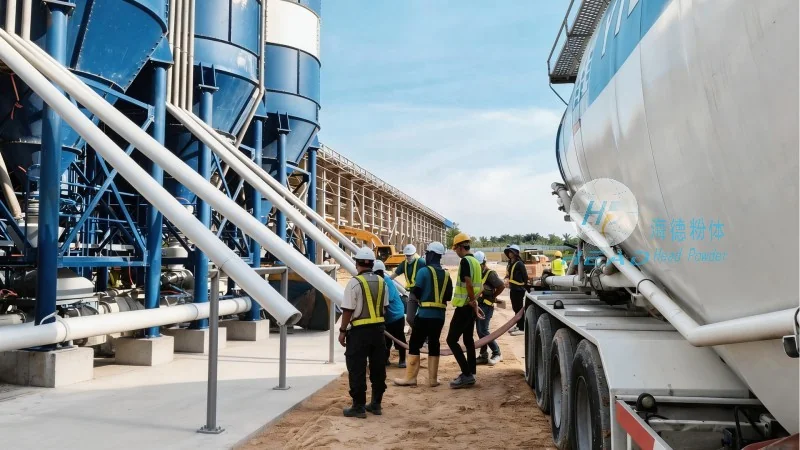
The fundamental working principle of lightweight aggregate material handling equipment revolves around a series of interconnected components and processes tailored to the physical characteristics of lightweight aggregates. The system typically begins with material storage in a hopper or silo, where the aggregates are held until needed. A feeder mechanism, such as a rotary or vibratory feeder, then regulates the flow of material into a conveyor system. The conveyor—often a belt conveyor, screw conveyor, or pneumatic conveyor—transports the lightweight aggregates to the next stage of processing or packaging. In some applications, classifiers or separators may be integrated to sort materials by size or density, ensuring uniformity. Control systems, including sensors for material levels and flow rates, monitor the entire process, enabling automated adjustments to maintain optimal performance. This integrated approach ensures smooth material flow, minimizing blockages and ensuring consistent output.
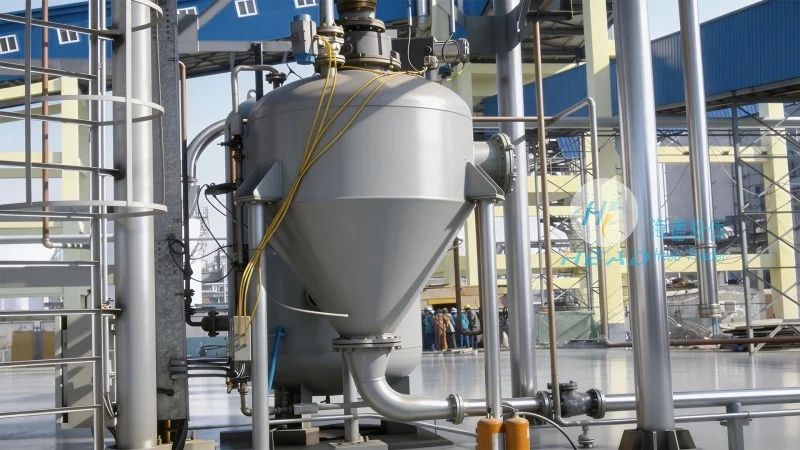
Lightweight aggregate material handling equipment is distinguished by several critical features that enhance its functionality and usability. One primary feature is its robust construction, designed to withstand the abrasive and low-density nature of lightweight aggregates without excessive wear. The equipment often incorporates specialized components, such as wear-resistant liners and durable conveyor belts, to extend operational life and reduce maintenance. Another key feature is the integration of dust control systems, including dust collectors and filtration units, which are vital for maintaining a clean, safe working environment, especially when handling powders or fine particles. The equipment also offers adjustable speed controls and variable feed rates, allowing operators to adapt the system to different production volumes and material types. Modern systems frequently utilize energy-efficient technologies, like variable frequency drives (VFDs) and optimized conveyor designs, to reduce energy consumption and operational costs. Additionally, the equipment is engineered for minimal downtime, with modular components that simplify maintenance and repairs, ensuring continuous operation in industrial settings.
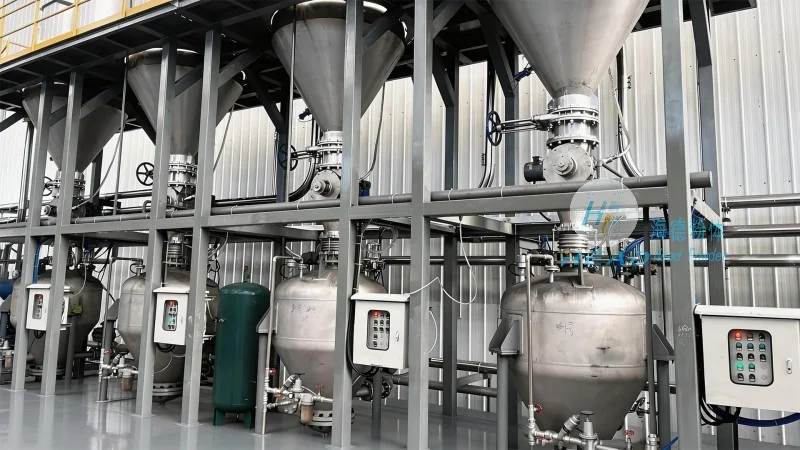
Lightweight aggregate material handling equipment is widely employed across multiple industries, with notable applications in construction, insulation manufacturing, and chemical processing. In the construction sector, these systems are critical for transporting expanded clay aggregates used in lightweight concrete, which enhances thermal insulation and reduces structural weight. For insulation manufacturers, the equipment efficiently handles perlite and vermiculite, essential components in thermal and acoustic insulation products. The benefits of using such equipment include improved material flow control, reduced labor costs through automation, enhanced workplace safety via automated processes, and consistent product quality. The ability to handle large volumes of lightweight aggregates efficiently also boosts production throughput and minimizes downtime, making the equipment a valuable investment for businesses in these fields. Furthermore, the equipment’s design ensures compatibility with various production scales, from small-scale operations to large industrial facilities, providing flexibility and adaptability to meet diverse production needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top