Urea material handling systems are sophisticated industrial solutions designed to efficiently transport and manage urea, a vital component in modern agriculture. These systems are integral to the supply chain of urea production, ensuring that the material is moved from production facilities to storage or packaging areas with minimal loss and maximum efficiency. The operation of such systems involves a series of coordinated components and processes, each playing a critical role in maintaining the integrity and flow of the urea material.
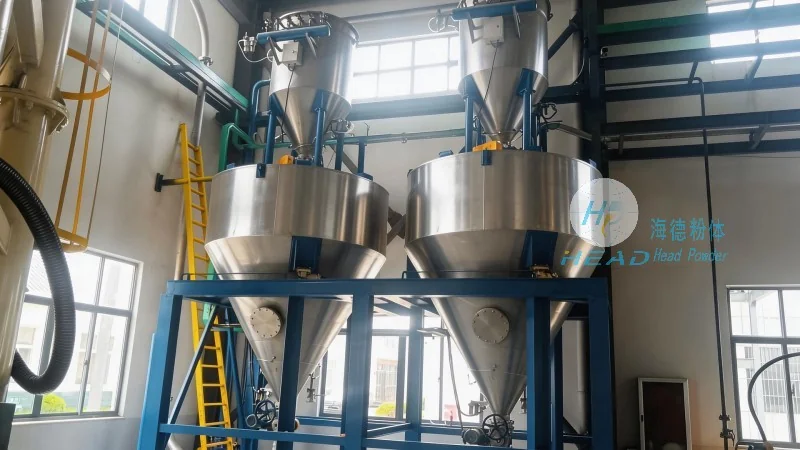
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a prominent manufacturer specializing in the development and production of advanced material handling equipment. With years of experience in the chemical processing industry, the company has built a reputation for delivering high-quality, reliable systems that meet the stringent requirements of modern urea production facilities. HeadPowder's commitment to innovation and customer satisfaction has positioned it as a leading provider of urea material handling solutions, serving clients globally with tailored equipment that enhances operational efficiency and safety.
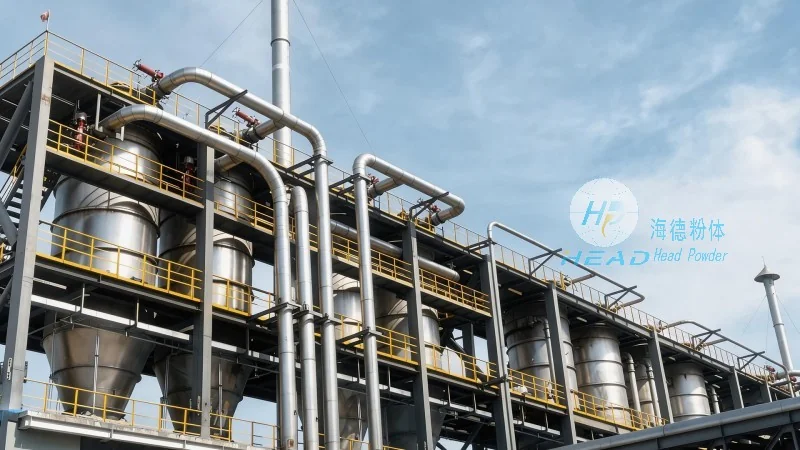
The urea material handling system typically consists of several key components, each designed to perform a specific function in the material flow process. The primary components include feeders, conveyors, storage silos, and control systems. Feeders, often equipped with adjustable speed mechanisms, are responsible for regulating the initial flow of urea from the production line into the system. They ensure a consistent and controlled feed rate, preventing overloading or underfeeding of the conveyor. Conveyors, which may be belt, screw, or pneumatic types, transport the urea from the feeder to the storage silos or packaging lines. Belt conveyors are commonly used for bulk material handling due to their high capacity and ability to handle large volumes of urea. Screw conveyors, on the other hand, are ideal for vertical or inclined transport, providing a compact solution for moving urea between different levels. Storage silos are large, airtight containers that store the urea, maintaining its quality and preventing moisture absorption. These silos are equipped with level sensors to monitor the material inside, ensuring proper inventory management. The control system, usually a programmable logic controller (PLC), integrates all components, monitoring parameters such as flow rate, pressure, and temperature, and adjusts operations automatically to maintain optimal performance.
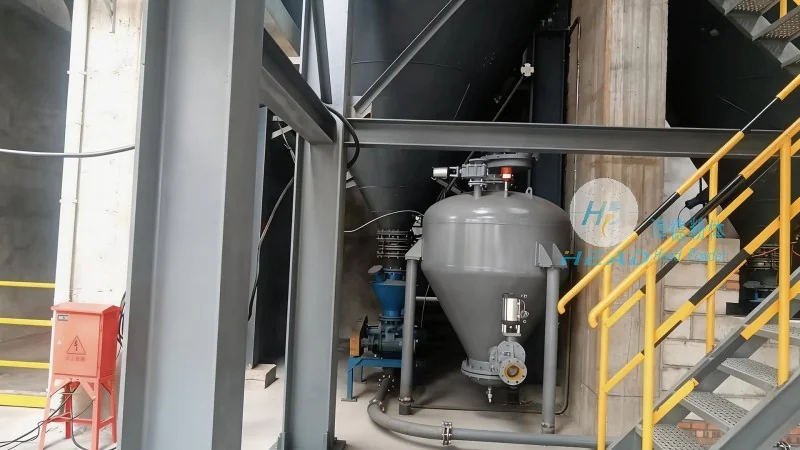
The operational process of a urea material handling system begins with the reception of urea from the production unit. The urea, in granular or prilled form, is first collected in a feed hopper. The feeder then regulates the flow of urea into the conveyor system. The conveyor transports the urea to the storage silos or directly to the packaging line. If the system is configured for storage, the urea is deposited into the silos, where it is held until it is needed for packaging or distribution. The control system continuously monitors the level of urea in the silos and adjusts the feeder speed to maintain the desired inventory level. For packaging operations, the urea is conveyed directly to the packaging machinery, where it is weighed and packaged into bags or containers. The entire process is automated, with the PLC controlling the speed and direction of the conveyor, the feeder, and the silo valves. This automation ensures that the system operates smoothly, with minimal human intervention, reducing the risk of errors and increasing production efficiency.
The working principle of urea material handling systems is based on the principles of mechanical engineering and automation. The system operates by converting electrical energy into mechanical energy to move the urea through the system. The electric motors powering the conveyors and feeders provide the necessary force to transport the urea. The control system, using sensors and feedback mechanisms, adjusts the speed and direction of the components to maintain a consistent flow. For example, if the level of urea in the feed hopper decreases, the control system increases the feeder speed to maintain a constant flow rate. Similarly, if the storage silo is filling up, the system reduces the feeder speed to prevent overfilling. The system also incorporates safety features, such as emergency stop buttons and overload protection, to ensure the safety of operators and the equipment. Additionally, dust suppression systems are often integrated into the design to control airborne particles, which is essential for maintaining a safe working environment, as urea dust can cause respiratory issues if inhaled in large quantities.
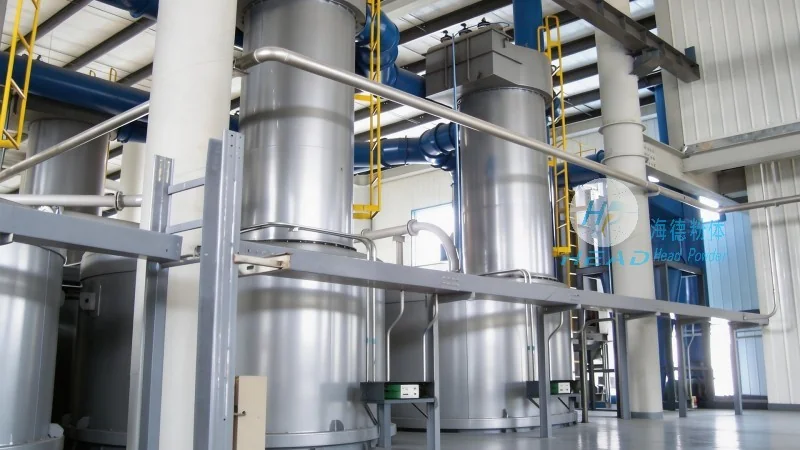
Proper maintenance is crucial for the long-term performance and reliability of urea material handling systems. Regular maintenance activities include cleaning the conveyor belts and screws to prevent material buildup, checking the motor and gearbox for wear and tear, and inspecting the control system for any faults. The storage silos should be inspected periodically for any signs of corrosion or damage, as urea can be corrosive to certain materials. Additionally, the system should be checked for any leaks or blockages in the pipelines or conveyor systems. Proper training of operators is also essential to ensure that they understand the system's operation and can respond appropriately to any issues that may arise. By following a regular maintenance schedule and adhering to safety protocols, the system can operate efficiently and safely for many years, providing reliable service to the urea production facility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top