Clay ash, a byproduct of industrial processes, requires efficient handling and transportation systems to ensure smooth operation in various industrial applications. The equipment designed for clay ash material handling plays a crucial role in optimizing material flow, reducing operational costs, and enhancing overall productivity. This article provides a detailed overview of the operation process and working principle of such systems, highlighting the key components and mechanisms involved.
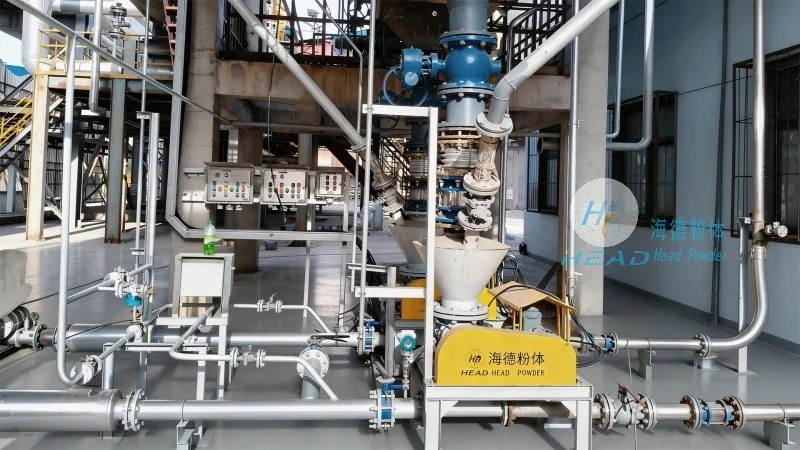
As a leading manufacturer in the field of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and supplying advanced equipment for industrial material processing. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable clay ash handling systems. HeadPowder's expertise lies in designing customized solutions that meet the specific requirements of clients, ensuring optimal performance and durability in demanding industrial environments.
The clay ash material handling system typically consists of several critical components that work in tandem to facilitate efficient material transport. These components include feeders, conveyors, storage silos, and control systems. Each component is engineered to handle the unique characteristics of clay ash, such as its density, moisture content, and particle size. The feeders are responsible for uniformly distributing the material into the conveyor system, while the conveyors transport the material to the desired location. Storage silos are used to store the clay ash temporarily, allowing for controlled release and preventing material buildup. Control systems monitor and regulate the entire process, ensuring safety and efficiency.
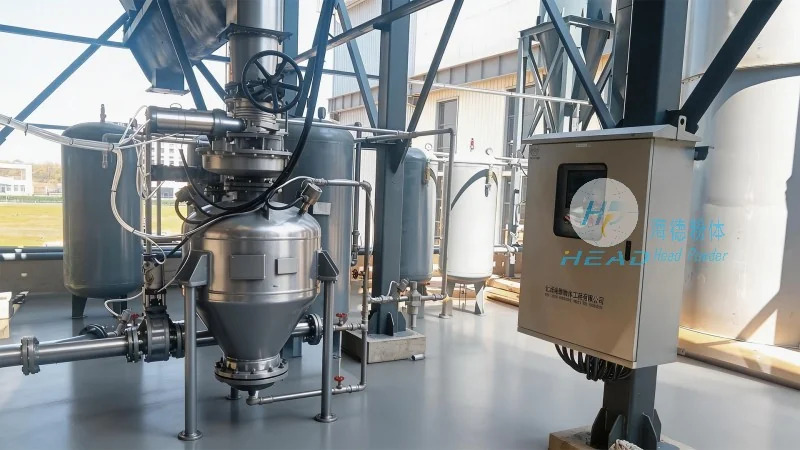
The operation process of clay ash material handling equipment begins with the intake of raw clay ash material. The material is first fed into a hopper or feeder, where it is evenly distributed and prepared for transport. The feeder then transfers the material to the conveyor system, which moves the material along a designated path. The conveyor may be a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the specific requirements of the application. As the material moves through the system, it is continuously monitored for flow rates and any potential blockages. The control system adjusts the speed and operation of the feeder and conveyor to maintain optimal material flow. Once the material reaches the storage silo or processing unit, it is discharged as needed, completing the cycle.
The working principle of clay ash material handling systems is based on mechanical and pneumatic forces to move the material from one location to another. The primary mechanism involves the use of conveyors, which utilize friction or air pressure to transport the material. In belt conveyors, the material is placed on a moving belt and carried to the destination. Screw conveyors use a rotating screw to push the material forward, while pneumatic conveyors use air pressure to transport the material through a pipeline. The control system plays a vital role in regulating the speed and direction of the conveyor, ensuring that the material is transported safely and efficiently. Sensors and detectors are also integrated into the system to detect any abnormalities, such as blockages or overloads, and trigger appropriate responses to prevent damage to the equipment.
Clay ash material handling systems offer several advantages over traditional manual handling methods. These systems enhance operational efficiency by automating the material transport process, reducing labor costs and human error. The consistent flow of material ensures that production processes are not interrupted, leading to increased productivity. Additionally, the systems improve safety by minimizing the risk of accidents associated with manual handling, such as falls or material spills. The use of advanced control systems allows for real-time monitoring and adjustment, ensuring optimal performance and reducing downtime. The durability of the equipment, designed to withstand the harsh conditions of industrial environments, ensures long-term reliability and low maintenance costs.
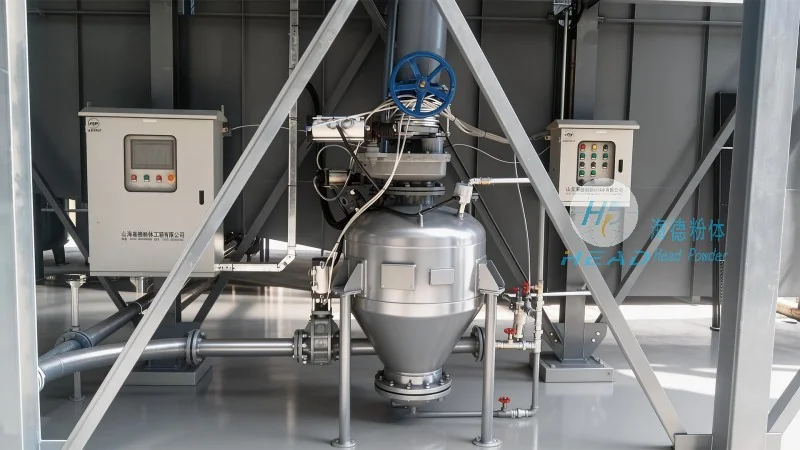
Clay ash material handling systems are widely used in various industrial sectors, including power plants, cement manufacturing, and mining. In power plants, the system is used to transport ash from the boiler to the storage facility, ensuring efficient disposal and reuse. In cement manufacturing, the system handles ash as a raw material, contributing to the production of cement. In mining operations, the system is used to transport ash from processing facilities to storage or disposal sites. The versatility of the equipment allows it to be adapted to different applications, making it a valuable asset for businesses in these industries.
Clay ash material handling systems are essential for optimizing material flow and enhancing operational efficiency in industrial applications. The advanced technology and robust design of these systems ensure reliable performance and durability. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality solutions to meet the evolving needs of the industry. With its headquarters in Shandong, China, HeadPowder remains committed to delivering exceptional service and support to its clients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top