Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced material handling systems tailored for the rice bran processing industry. The company's expertise lies in developing efficient and reliable equipment that optimizes the transportation of rice bran, a byproduct of rice milling, from production lines to storage or further processing stages.
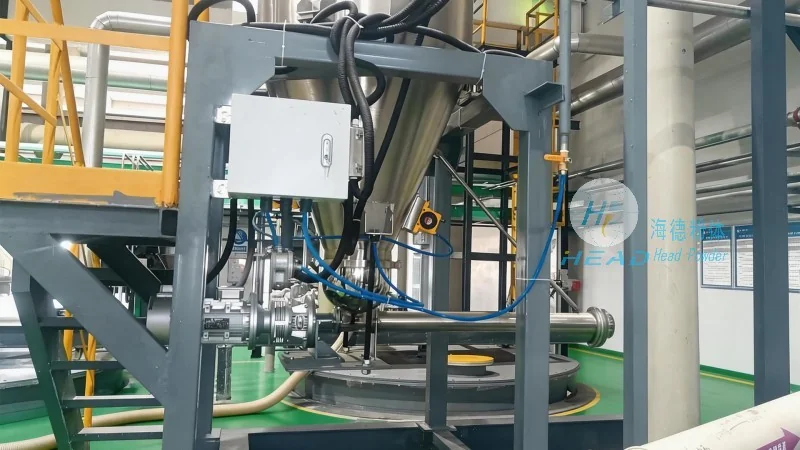
At the core of rice bran processing operations is the efficient movement of this valuable material. Rice bran, rich in nutrients and widely used in food, feed, and industrial applications, requires specialized handling to maintain its quality and prevent degradation. The material handling systems designed by HeadPowder are engineered to address these challenges, ensuring minimal loss, consistent flow, and easy integration into existing production workflows.
The rice bran material handling system typically comprises several critical components, each playing a vital role in the overall operation. These include feeders, conveyors, elevators, and storage silos, all working in tandem to achieve seamless material transfer. Feeders, such as screw feeders or vibratory feeders, are responsible for initial material intake and uniform feeding. Conveyors, often belt or chain types, transport the bran over longer distances or to elevated levels. Elevators, like bucket elevators or pneumatic conveyors, handle vertical movement, while storage silos provide temporary or long-term storage, ensuring a steady supply for downstream processes.
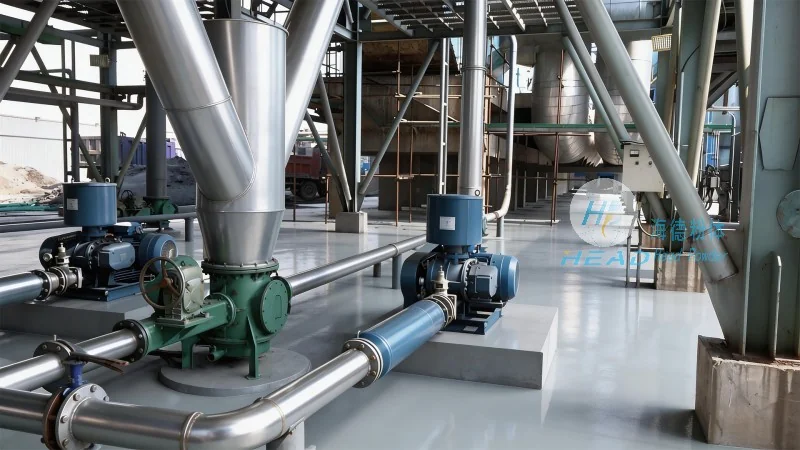
The operation of the rice bran material handling system begins with the collection of bran from the milling machine. The system's feeders capture the bran as it is produced, preventing spillage and maintaining a consistent flow. The bran is then conveyed through a series of connected components, moving from the initial collection point to the storage silo or to other processing units. The conveyors are equipped with adjustable speed controls and material sensors to ensure smooth operation and prevent blockages. In cases where vertical movement is required, elevators lift the bran to higher levels, utilizing mechanical or pneumatic systems to maintain efficiency. Throughout the process, the system's controls monitor key parameters like flow rate, pressure, and temperature, ensuring optimal performance and product quality.
The working principle of the rice bran material handling system combines mechanical engineering with advanced control systems. The mechanical components, including conveyors and elevators, rely on motor-driven mechanisms to move the material. For example, belt conveyors use rotating pulleys and tension systems to transport bran, while bucket elevators utilize buckets attached to a rotating chain to lift material vertically. Pneumatic conveyors, on the other hand, use air pressure to transport fine or dusty materials, offering flexibility in layout and reduced mechanical wear. The control systems integrate sensors and programmable logic controllers (PLCs) to regulate the operation of each component. Sensors detect material levels, flow rates, and blockages, triggering automatic responses such as adjusting conveyor speed or activating alarms. PLCs coordinate the sequence of operations, ensuring that each step is executed in the correct order and that the system operates efficiently and safely.
HeadPowder's rice bran material handling systems offer several advantages that enhance operational efficiency and product quality. The systems are designed for high capacity and low maintenance, reducing downtime and operational costs. The use of durable materials and robust construction ensures long service life, even under harsh conditions. The integration of advanced controls provides real-time monitoring and data collection, enabling operators to optimize performance and troubleshoot issues quickly. Additionally, the systems are modular, allowing for easy customization and expansion to meet changing production needs. This flexibility makes them suitable for both small-scale and large-scale rice bran processing facilities.
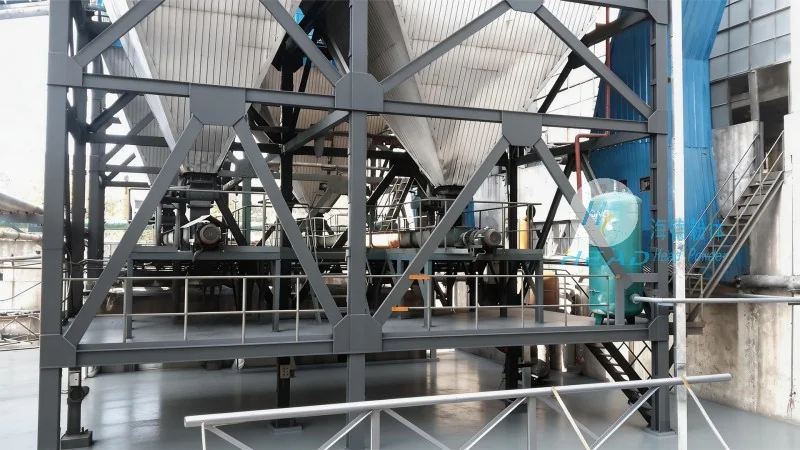
Rice bran material handling systems are essential in the rice bran industry for maintaining product quality and improving process efficiency. The systems are widely used in rice mills, where they transport bran from the milling section to storage or to further processing units such as oil extraction or animal feed production. The consistent flow and minimal loss provided by these systems ensure that the bran reaches its destination in optimal condition, preserving its nutritional value and market value. In addition, the systems contribute to a cleaner and more organized production environment, reducing the risk of contamination and improving workplace safety.
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive rice bran material handling solutions that combine advanced technology with practical design. The operation process and working principle of these systems are engineered to meet the specific needs of the rice bran industry, ensuring efficient material transport, minimal loss, and high product quality. By leveraging their expertise in material handling technology, HeadPowder helps rice mills and processing facilities enhance their operational performance and achieve greater productivity. With a focus on reliability and innovation, HeadPowder continues to be a trusted partner in the rice bran processing sector, delivering solutions that meet the evolving demands of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top