Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design, production, and supply of wheat flour material handling equipment. The company is located in Shandong, China, and has been committed to providing high-quality and efficient solutions for the flour processing industry.
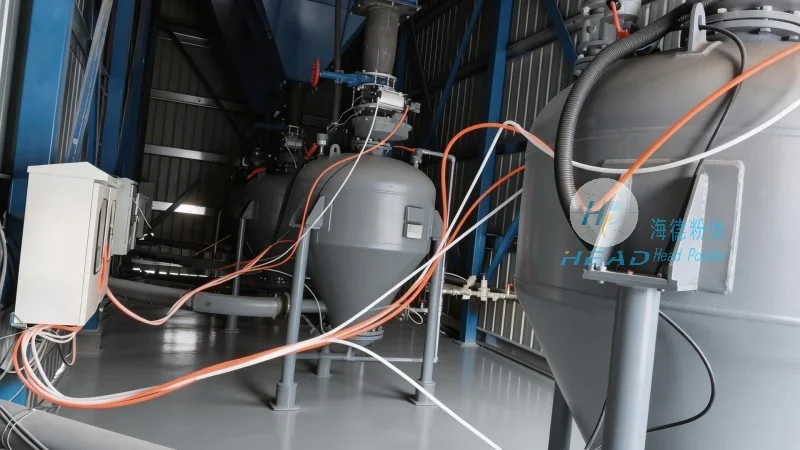
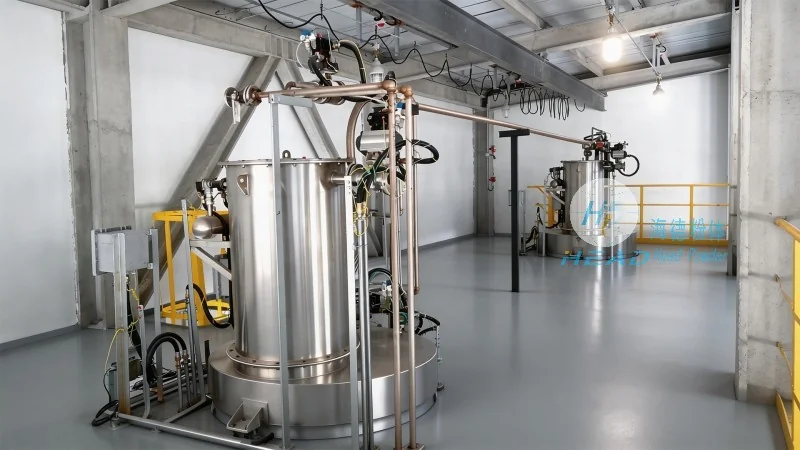
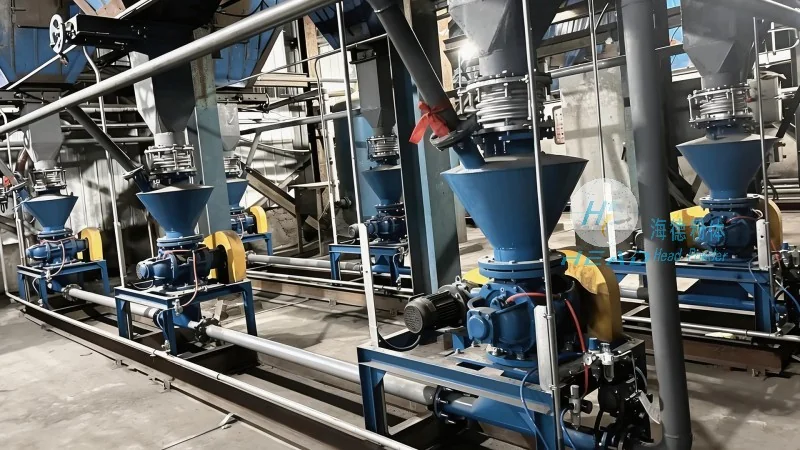
The operation process of wheat flour material handling equipment is a systematic sequence of actions designed to ensure the seamless transfer of wheat flour from its source to the processing or storage destination. The process starts with the preparation of the flour, which may involve screening or cleaning to remove impurities before it enters the conveying system. The initial step involves the use of a feeder, such as a rotary valve or a variable-speed screw feeder, which regulates the flow of flour into the primary conveyor. The feeder is crucial for maintaining a consistent feed rate, as fluctuations can lead to uneven conveying or system inefficiencies. Once the flour is fed into the conveyor, it is transported through a series of pipes or hoses. For pneumatic systems, the conveyor uses compressed air to create a positive pressure that propels the flour through the pipeline. The air flow is carefully controlled to achieve the optimal velocity for flour suspension, ensuring that the particles remain airborne and do not settle. In mechanical systems, such as screw or belt conveyors, the rotating components apply a continuous force to move the flour along the conveyor path. These systems are often equipped with variable speed drives to adjust the conveying rate based on the flour's characteristics and the system's load. The conveying process may also include intermediate storage or mixing units, where the flour can be blended or conditioned before further processing. The final stage involves the discharge of the flour into the target container, which could be a storage silo, a processing machine, or a packaging line. The discharge mechanism, such as a rotary valve or a gate valve, controls the release of the flour to prevent spills and maintain a controlled flow. Throughout the operation, the equipment is monitored by sensors and control systems to detect any issues, such as blockages or pressure changes, and to adjust the process parameters accordingly.
The working principle of wheat flour material handling equipment is rooted in the fundamental physics of material transport and the specific requirements of flour handling. For pneumatic conveying systems, the core principle is the use of compressed air to create a fluidized bed of flour particles, allowing them to be transported through a pipeline. The air velocity is maintained above the "saltation velocity," which is the minimum speed required to keep the flour suspended and prevent it from settling. This principle ensures that the flour moves efficiently without clogging the system. Mechanical conveying systems, on the other hand, rely on the principle of mechanical force to move the material. Screw conveyors, for example, use a rotating screw to push the flour along the conveyor tube, while belt conveyors use a moving belt to transport the material. These systems are particularly effective for handling bulk materials with higher moisture content or larger particle sizes, as they can maintain a consistent flow without the need for air. The equipment also incorporates features like airlocks and dust collectors to maintain air quality and prevent contamination. Airlocks are used to separate the conveying system from the processing area, preventing the backflow of air or flour. Dust collectors, such as cyclones or bag filters, remove airborne particles to ensure a clean and safe working environment. The integration of these principles allows the equipment to handle the delicate nature of wheat flour while maintaining efficiency, reliability, and compliance with industry standards. The design of the equipment is tailored to the specific characteristics of the flour, such as particle size, moisture content, and flowability, to optimize performance and minimize product degradation. Additionally, the equipment is equipped with sensors and control systems that monitor key parameters like pressure, flow rate, and temperature, ensuring that the process remains stable and within safe operating limits. Regular maintenance of these components is essential to prevent wear and tear and ensure long-term performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top