For food processing facilities, especially those dealing with liquid seasonings like chicken essence, efficient material handling is crucial to maintain product quality and operational efficiency. The equipment designed for transporting chicken essence, often referred to as chicken essence material handling equipment, plays a vital role in ensuring smooth production workflows. This article explores the operational process and working principles of such equipment, highlighting how it contributes to the overall productivity and reliability of chicken essence production lines.
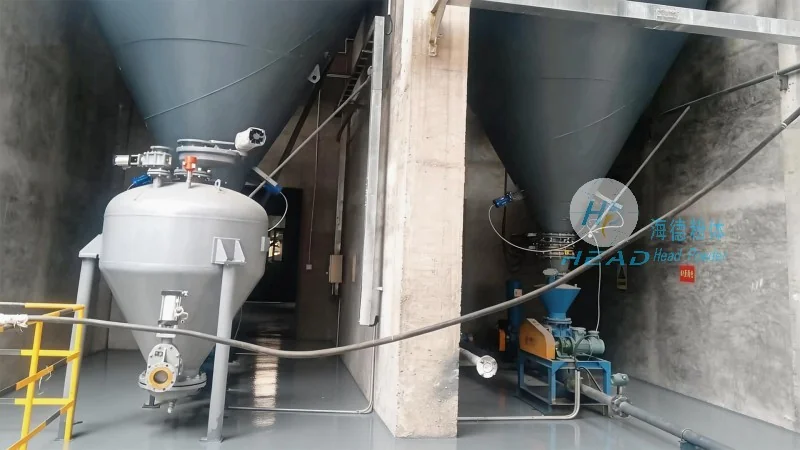
Overview of Chicken Essence Material Handling Equipment
Chicken essence material handling equipment is specifically engineered to handle the transportation of chicken essence, a popular liquid seasoning used in various food products. These systems are designed to manage the flow of chicken essence from storage tanks to processing units, packaging lines, or other destinations within a food processing plant. The equipment typically includes components such as pumps, conveyors, tanks, and control systems, all working in tandem to ensure safe and efficient material movement.
Key Components of the Equipment
The chicken essence material handling equipment consists of several critical components that work together to achieve the desired functionality. The primary components include:
- Storage Tanks: These tanks are used to store the chicken essence before it is transported. They are usually made of stainless steel to prevent contamination and ensure durability.
- Pumps: Pumps are essential for moving the liquid chicken essence from the storage tanks to the processing or packaging areas. Centrifugal pumps or positive displacement pumps are commonly used, depending on the viscosity and flow rate requirements.
- Conveyors: Conveyors may be used to transport bulk chicken essence or related ingredients, such as spices or seasonings, to the processing line. These can include screw conveyors, belt conveyors, or pneumatic conveyors, depending on the specific application.
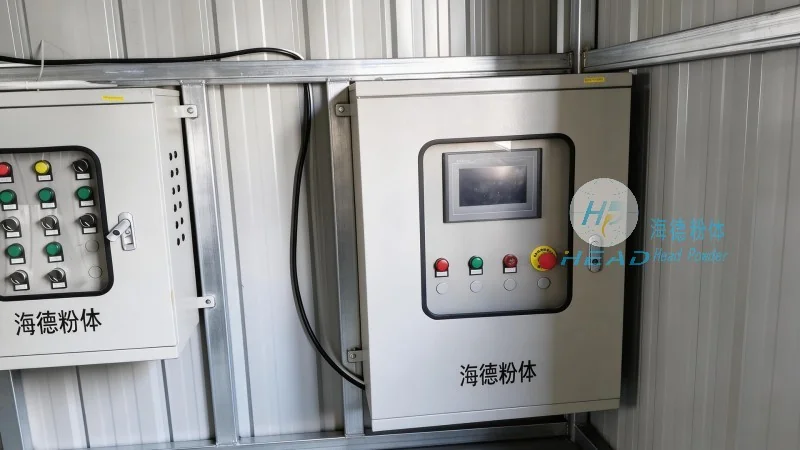
- Control Systems: Advanced control systems are integrated into the equipment to monitor and regulate the flow of chicken essence. These systems ensure that the pump speed, pressure, and flow rate are maintained within optimal parameters, preventing overfilling or underfilling.
The Operating Process of Chicken Essence Material Handling Equipment
The operation of chicken essence material handling equipment follows a systematic process to ensure consistent and efficient material movement. The typical steps involved are as follows:
- Preparation and Loading: The chicken essence is first loaded into the storage tanks. The tanks are then sealed to prevent contamination and ensure that the liquid remains in optimal condition.
- Initiation of Pumping: Once the storage tanks are filled, the control system is activated to start the pumps. The pumps begin to draw the chicken essence from the tanks and move it through the piping system.
- Transport to Processing Units: The chicken essence is transported through the pipelines to the processing units, such as mixing or blending equipment. The pumps maintain the required pressure and flow rate to ensure smooth delivery.
- Delivery to Packaging Lines: After processing, the chicken essence is directed to the packaging lines. The equipment ensures that the liquid is delivered at the correct volume and pressure to fill containers accurately.
- Monitoring and Adjustment: Throughout the process, the control system continuously monitors the flow rate, pressure, and temperature of the chicken essence. If any deviations are detected, the system automatically adjusts the pump speed or other parameters to maintain optimal conditions.
Working Principle of the Equipment
The working principle of chicken essence material handling equipment is based on the principles of fluid dynamics and mechanical engineering. The equipment operates by converting mechanical energy into hydraulic energy to move the liquid chicken essence. The key principles include:
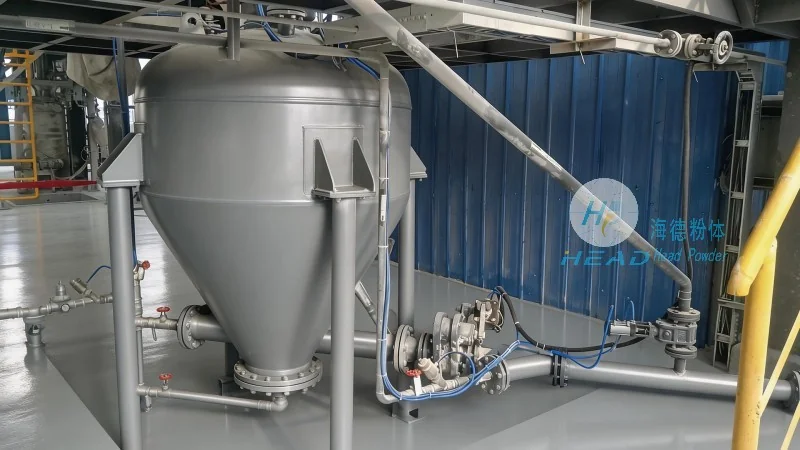
- Pressure Generation: Pumps generate pressure by compressing the liquid chicken essence, which allows it to be transported through the pipelines against gravity or other resistance.
- Flow Control: The control system regulates the flow rate by adjusting the pump speed or using valves to maintain the desired flow rate. This ensures that the chicken essence is delivered at the correct rate for processing or packaging.
- Temperature Management: Some systems may include temperature control features to maintain the chicken essence at a consistent temperature, preventing degradation or separation of components.
- Prevention of Contamination: The equipment is designed with sanitary components and sealed systems to prevent contamination from external sources, ensuring that the chicken essence remains safe for consumption.
Benefits of Using Chicken Essence Material Handling Equipment
Implementing chicken essence material handling equipment offers several benefits to food processing facilities. These include improved operational efficiency, reduced labor costs, enhanced product quality, and increased safety. The equipment minimizes the risk of spills or leaks, which can lead to product loss or contamination. Additionally, the automated control systems reduce the need for manual intervention, allowing operators to focus on other critical tasks.
Conclusion
Chicken essence material handling equipment is a critical component of modern food processing facilities, ensuring the efficient and safe transportation of chicken essence. By understanding the operating process and working principles of such equipment, food manufacturers can optimize their production lines and maintain high standards of quality and safety. The equipment, manufactured by companies like Shandong HeadPowder Engineering Co., Ltd., provides reliable solutions for handling liquid seasonings, contributing to the overall success of chicken essence production.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
