Positive pressure material conveying lines, also known as pressurized conveying systems, are advanced industrial solutions designed to transport bulk materials efficiently and safely. These systems are widely used in various industries, including chemical, food processing, and pharmaceuticals, where the handling of powders and granules requires precise control and minimal contamination. The core technology behind these systems involves creating a positive pressure environment within the conveying line, ensuring that material is moved from the source to the destination without external air infiltration or material spillage. As a leading provider of industrial conveying solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality positive pressure material conveying lines tailored to meet the specific needs of different industries.
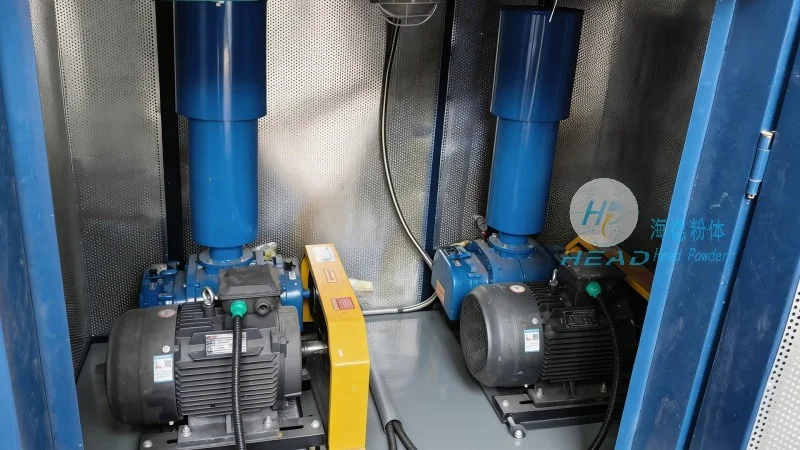
The fundamental principle of positive pressure material conveying is based on the generation of a pressure differential. The system operates by blowing air or a carrier gas into the conveying line at a pressure higher than the ambient air pressure. This pressure differential forces the material to move through the pipeline. The key components of a typical positive pressure system include a material feeder, a positive displacement blower or compressor, a conveying line (often made of stainless steel or other corrosion-resistant materials), and a discharge device. The material feeder, such as a rotary valve or a screw feeder, ensures a consistent flow of material into the system. The positive displacement blower then creates the necessary pressure to push the material through the line. The conveying line is designed to handle the material's properties, such as particle size, moisture content, and abrasiveness, to prevent blockages or wear. The discharge device, like a rotary valve or a bagging unit, controls the release of material at the destination. The system also includes pressure sensors and control valves that monitor and regulate the pressure within the line, ensuring stable operation and preventing over-pressurization or under-pressurization, which could lead to inefficiencies or equipment damage.
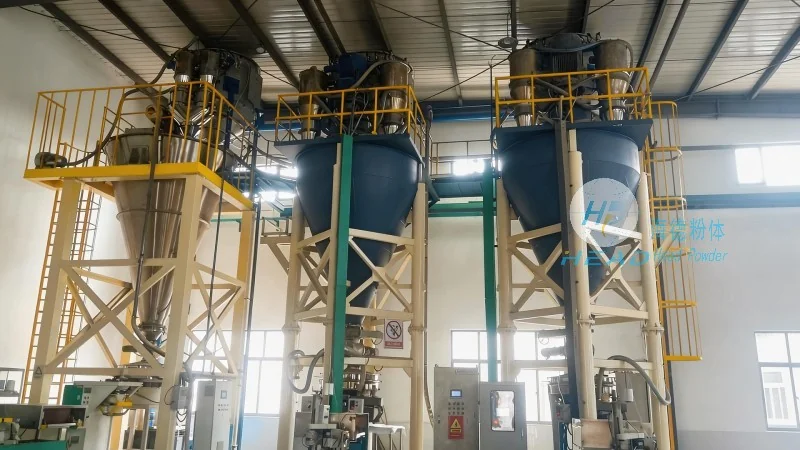
The operation of a positive pressure material conveying line involves several sequential steps that ensure smooth and continuous material transport. First, the material is fed into the system from the source, typically a hopper or a storage silo. The feeder regulates the flow rate, ensuring that the material is introduced at a consistent rate. Next, the positive displacement blower or compressor starts, generating the required pressure. The pressure is maintained at a level sufficient to overcome the resistance in the conveying line, including the length of the line, the number of bends, and the material's frictional properties. As the pressure is applied, the material is carried along the pipeline by the moving air or gas. The conveying line is equipped with sensors and controls to monitor the pressure and flow, ensuring that the system operates within safe and efficient parameters. At the destination, the material is discharged through the discharge device, which may include a filter to remove any dust or particles before release. The entire process is automated, with controls that can adjust the feeder speed and blower pressure based on real-time conditions, optimizing the conveying efficiency and reducing energy consumption. For example, in a chemical plant, the system may be programmed to increase the blower pressure when the line length increases due to a change in the material's location, ensuring consistent performance without manual intervention.
Positive pressure material conveying systems offer several advantages over traditional vacuum or negative pressure systems. One of the primary benefits is the ability to handle a wide range of material types, including fine powders, granules, and even sticky or abrasive materials. The positive pressure environment prevents material from settling or caking in the line, reducing the risk of blockages and maintenance issues. Additionally, these systems are more energy-efficient compared to vacuum systems, as they require less power to maintain the pressure. The enclosed design of the conveying line also minimizes dust emissions and environmental contamination, making them suitable for applications where dust control is critical. Furthermore, the systems are easy to clean and maintain, as the components are designed to be accessible and removable for inspection and cleaning. This feature is particularly important in industries such as food and pharmaceuticals, where hygiene and cleanliness are paramount. For instance, in a food processing facility, the stainless steel construction of the conveying line allows for easy cleaning and sanitization, ensuring compliance with food safety regulations. The positive pressure system also reduces the risk of cross-contamination between different materials, as each line is isolated and operated independently.
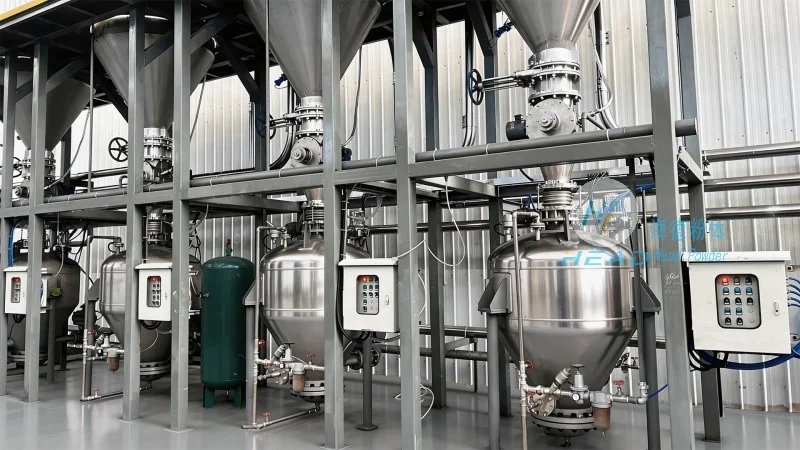
Positive pressure material conveying lines are used in a variety of industries where bulk material handling is essential. In the chemical industry, these systems are used to transport raw materials and finished products, such as powders and granules, between processing units. The pharmaceutical industry relies on positive pressure systems to handle active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the materials are transported in a sterile and controlled environment. The food processing industry uses these systems to convey ingredients like flour, sugar, and spices, maintaining the quality and safety of the products. Additionally, in the mining and minerals sector, positive pressure conveying is used to transport ore and other bulk materials from processing plants to storage or shipping facilities. The versatility of these systems makes them suitable for a wide range of applications, from small-scale operations to large industrial plants. For example, a small-scale bakery might use a positive pressure conveying line to transport flour from a storage silo to the mixing area, while a large chemical plant might use multiple lines to transport different raw materials to various production units. The flexibility of the system allows for customization based on the specific requirements of each application, ensuring optimal performance and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top