HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced dust-free pneumatic conveying systems. These systems are engineered to efficiently transport bulk materials while maintaining a clean and dust-free environment, making them ideal for industries such as food processing, pharmaceuticals, and electronics manufacturing.
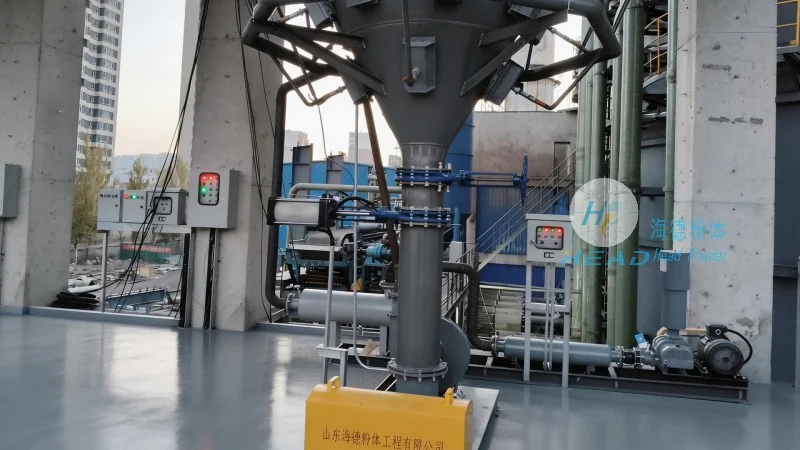
The operation of a dust-free pneumatic conveying machine involves several key components that work in harmony to achieve efficient material transport. The primary elements include a material hopper, a rotary valve or feeder, a conveying line (typically made of stainless steel to prevent contamination), a vacuum or pressure system, and a receiver or discharge unit. The material is first loaded into the hopper, where it is then fed into the conveying line through the rotary valve. The conveying system uses either vacuum (suction) or pressure (blowing) to move the material through the pipeline. In a dust-free system, the entire process is sealed to prevent any dust particles from escaping into the environment, ensuring compliance with strict industrial hygiene standards.
The operation of a dust-free pneumatic conveying machine follows a systematic sequence to ensure smooth and efficient material transfer. Initially, the bulk material is stored in the hopper. The rotary valve or feeder then regulates the flow of material into the conveying line. The vacuum or pressure system is activated, creating the necessary force to move the material through the pipeline. As the material travels, it is contained within the sealed system, preventing dust emissions. Upon reaching the receiver or discharge point, the material is collected, and the system returns to its idle state, ready for the next cycle. This continuous process allows for high-volume material handling with minimal human intervention and maximum environmental protection.
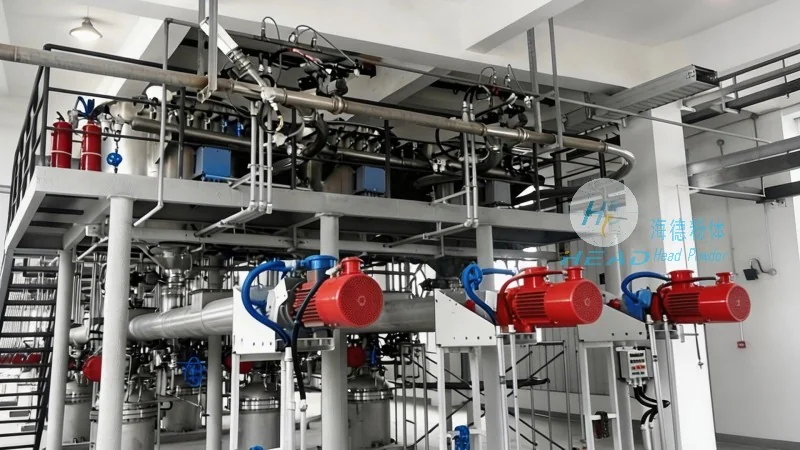
One of the most significant advantages of dust-free pneumatic conveying systems is their ability to maintain a clean working environment. Unlike traditional belt or bucket elevators, these systems do not generate dust, reducing the risk of respiratory issues for workers and preventing contamination of the transported materials. Additionally, the sealed design minimizes material loss and improves overall efficiency. The stainless steel construction of the conveying lines ensures durability and resistance to corrosion, making them suitable for a wide range of applications, including sensitive materials like food and pharmaceuticals. Furthermore, the systems are highly customizable, allowing manufacturers to adapt them to specific operational needs, such as varying material types, flow rates, and environmental requirements.
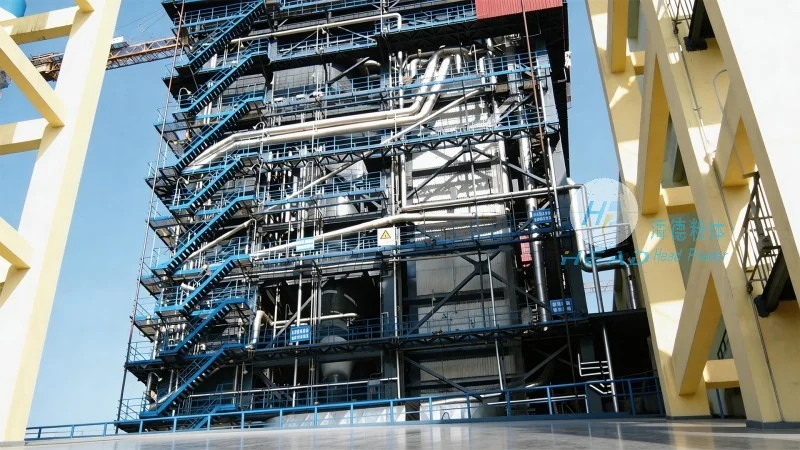
Dust-free pneumatic conveying equipment is widely used across various industries due to its versatility and effectiveness. In the food industry, it is used to transport ingredients like flour, sugar, and spices without compromising their quality or hygiene. In the pharmaceutical sector, it ensures that active ingredients and finished products are handled in a sterile environment, preventing contamination and maintaining product integrity. The electronics industry also benefits from these systems, as they help maintain a cleanroom environment, which is critical for producing high-quality components. Additionally, in the chemical and agricultural sectors, dust-free conveying systems are employed to handle powders and granules safely and efficiently, reducing the risk of dust explosions and improving workplace safety.
Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is a trusted provider of dust-free pneumatic conveying solutions. The company leverages advanced engineering and manufacturing capabilities to deliver high-performance systems that meet the stringent requirements of modern industries. By focusing on innovation and quality, HeadPowder ensures that its products are reliable, efficient, and environmentally friendly. For businesses seeking to enhance their material handling processes while maintaining a clean and safe working environment, dust-free pneumatic conveying systems from HeadPowder offer a superior solution. The company's commitment to customer satisfaction and technical excellence has established it as a leader in the field, providing tailored solutions that address the unique challenges of each application.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top