HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced pneumatic conveying equipment tailored for sand and gravel applications. This article delves into the operational process and underlying principles of such systems, providing a comprehensive understanding for industry professionals and potential clients.
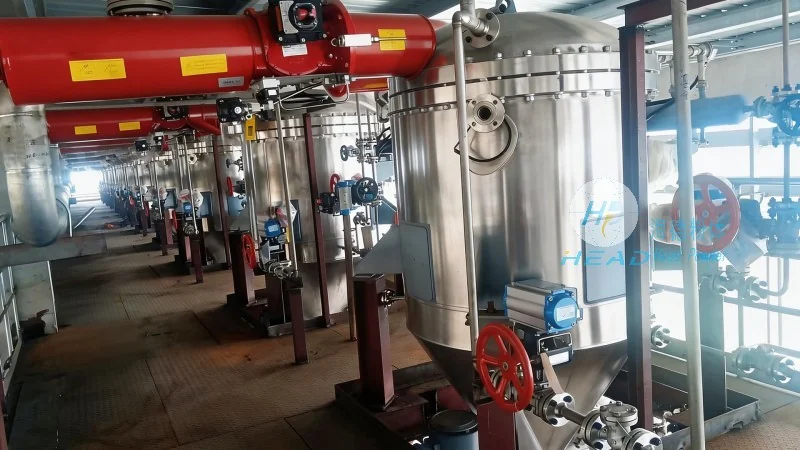
Pneumatic conveying systems are essential in the construction and mining sectors for efficiently transporting bulk materials like sand and gravel over short to medium distances. Unlike traditional mechanical conveyors, these systems utilize air or gas as the primary medium to move materials, offering advantages such as reduced wear on components, lower maintenance costs, and the ability to handle abrasive materials without significant damage. The core components of a typical sand and gravel pneumatic conveying system include a hopper for material storage, a blower or compressor to generate airflow, a pipeline network to transport the material, and a receiver or discharge point for the final delivery.
The operation of a sand and gravel pneumatic conveying system involves several sequential steps that ensure smooth and continuous material transport. Initially, the raw sand or gravel is fed into the hopper from a storage silo or truck. A feeder, often a rotary valve or a screw feeder, regulates the flow rate of the material into the system, preventing overloading and maintaining consistent pressure within the pipeline. Simultaneously, the blower or compressor starts, creating a high-pressure air stream that flows through the pipeline. As the material is introduced into the hopper, it is drawn into the air stream by the pressure differential, forming a dense mixture known as a "slurry" or "conveyed stream." This mixture travels through the pipeline under the force of the air, moving from the inlet to the discharge point. At the receiving end, the material is separated from the air using a cyclone separator or a filter, and the air is either recirculated or vented to the atmosphere. The separated material is then collected in a storage bin or directly used in the next production stage.
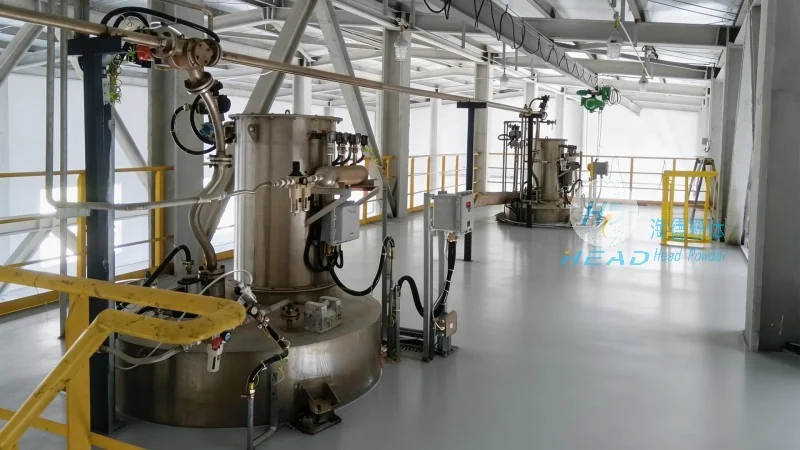
The working principle of pneumatic conveying equipment for sand and gravel is based on the fundamental concept of fluidization and particle suspension. When air is forced through the pipeline at a sufficient velocity, it creates a pressure drop that lifts the particles and keeps them suspended in the air stream. This process is known as "pneumatic transport" and relies on the balance between the air velocity and the gravitational force acting on the particles. The key factors influencing the efficiency of the system include the air velocity, the particle size and density, the pipeline diameter, and the length of the conveying line. High air velocity ensures that particles remain suspended, while excessive velocity can lead to increased energy consumption and potential wear on the pipeline. Conversely, low velocity may cause the particles to settle, leading to blockages or reduced conveying capacity. Proper design of the system, including the selection of blower capacity, pipeline diameter, and feeder type, is crucial to achieve optimal performance and minimize operational issues.
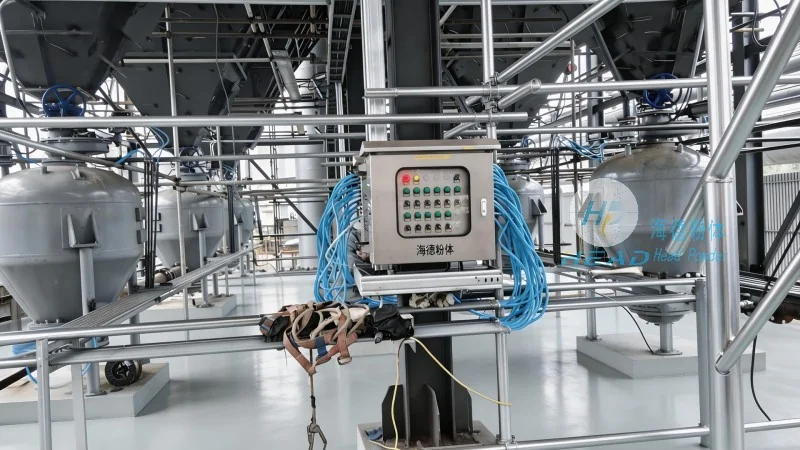
Several critical components work in tandem to ensure the efficient operation of a sand and gravel pneumatic conveying system. The hopper serves as the primary storage and feeding unit, with a smooth interior to prevent material buildup and ensure uniform flow. The feeder, typically a rotary valve or a screw feeder, controls the material discharge rate, maintaining a stable pressure in the system. The blower or compressor is the power source, generating the necessary airflow to transport the material. It is essential to select a blower with sufficient capacity to handle the material's specific gravity and particle size, as inadequate airflow can result in poor conveying performance. The pipeline network connects the hopper to the discharge point and is usually made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of sand and gravel. The receiver or discharge unit separates the material from the air and collects the final product. Cyclone separators are commonly used for this purpose, utilizing centrifugal force to separate particles from the air stream. The air is then either recirculated back to the blower or vented to the environment, depending on the system design.
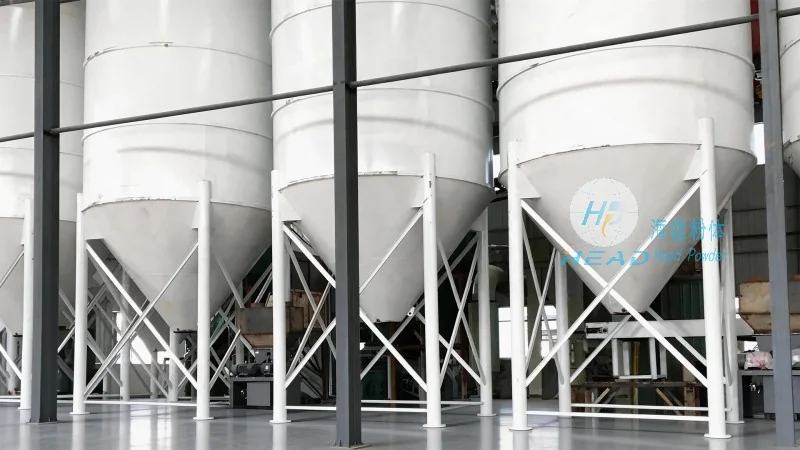
Pneumatic conveying systems offer several advantages over traditional mechanical conveyors, making them ideal for sand and gravel applications. First, they eliminate the need for moving parts in the conveying line, reducing wear and tear and maintenance costs. Second, the system can handle abrasive materials without significant damage to components, as the particles are suspended in the air rather than sliding against each other or the pipeline. Third, the equipment is compact and can be installed in confined spaces, making it suitable for construction sites or industrial facilities with limited space. Additionally, pneumatic conveying systems can transport materials vertically, horizontally, or at an angle, providing flexibility in system design. These advantages make the technology widely used in the construction industry for transporting sand and gravel from storage silos to mixing plants, in mining operations for material transport between processing stages, and in aggregate production facilities for material handling and distribution.
Proper maintenance and operational considerations are essential to ensure the longevity and efficiency of a sand and gravel pneumatic conveying system. Regular inspection of the hopper and feeder for material buildup or blockages is crucial to prevent system downtime. The blower and compressor should be checked for proper airflow and pressure, as any deviations can indicate issues with the system. The pipeline should be inspected for signs of wear or corrosion, particularly at bends and joints, as these areas are prone to stress and material abrasion. Cleaning the cyclone separator and other filtration components regularly is necessary to maintain optimal separation efficiency and prevent material accumulation. Additionally, monitoring the system's energy consumption can help identify inefficiencies and guide adjustments to improve performance. By following these maintenance practices, operators can ensure the system operates at peak efficiency, minimizing downtime and maximizing productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top