HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for handling rare earth mineral powders. The company's expertise lies in developing efficient solutions that address the unique challenges associated with transporting these valuable materials, ensuring optimal performance and reliability in industrial applications.
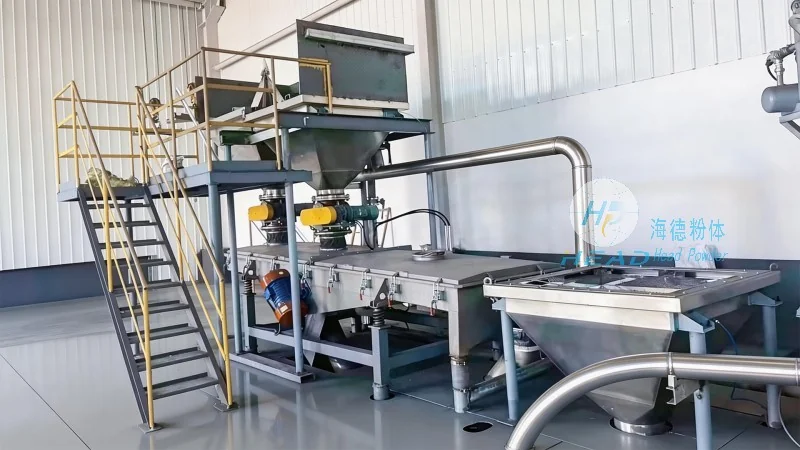
Pneumatic conveying equipment operates by utilizing air or gas to transport bulk materials like rare earth mineral powders through a pipeline system. The core principle involves creating a pressure differential or using vacuum to move the material from the source to the destination. For rare earth applications, the system typically employs either pressure or vacuum-based methods. Pressure systems use compressed air to push the material forward, while vacuum systems create a negative pressure to draw the material into the pipeline. This method eliminates the need for mechanical components such as buckets or belts, reducing maintenance and operational costs. The equipment is designed to handle fine powders with high moisture content or abrasive properties, which are common in rare earth processing. By controlling the air flow rate and pressure, the system ensures consistent material transport without clogging or degradation of the powder quality.
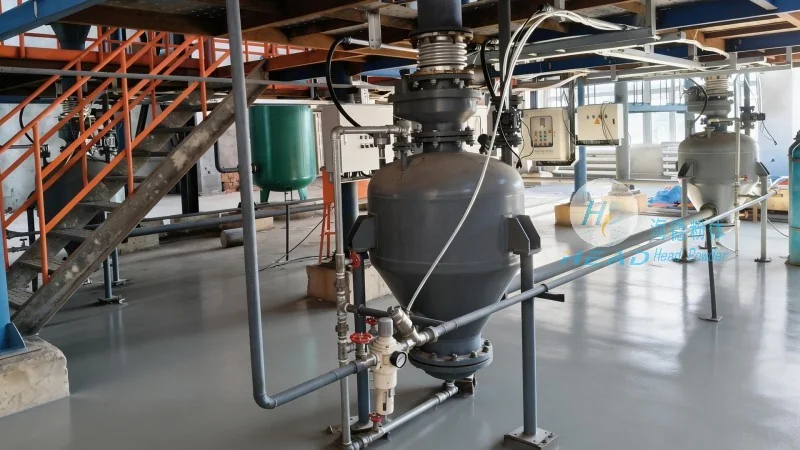
The working scene characteristics of these conveying systems are tailored to meet the specific demands of rare earth mineral processing facilities. In mining operations, the equipment is used to transport raw ore from extraction sites to processing plants, where the ore is crushed and milled into fine powders. The pneumatic system efficiently handles the high volume of material, minimizing the risk of dust dispersion and ensuring a clean working environment. In processing plants, the equipment is integrated into the production line to convey the rare earth powders between various stages, such as drying, magnetic separation, and chemical processing. The system's ability to handle fine particles and maintain consistent flow rates is crucial for maintaining product quality and process efficiency. Additionally, the equipment is designed to operate in environments with varying temperatures and humidity levels, making it suitable for both indoor and outdoor applications. The working scene also includes scenarios where the material needs to be transported over long distances or through complex layouts, requiring the use of multiple pipelines and control systems to ensure smooth operation. The characteristics of the equipment, such as its flexibility and adaptability, make it a preferred choice for industries dealing with rare earth minerals, as it can be customized to fit specific operational requirements and space constraints.
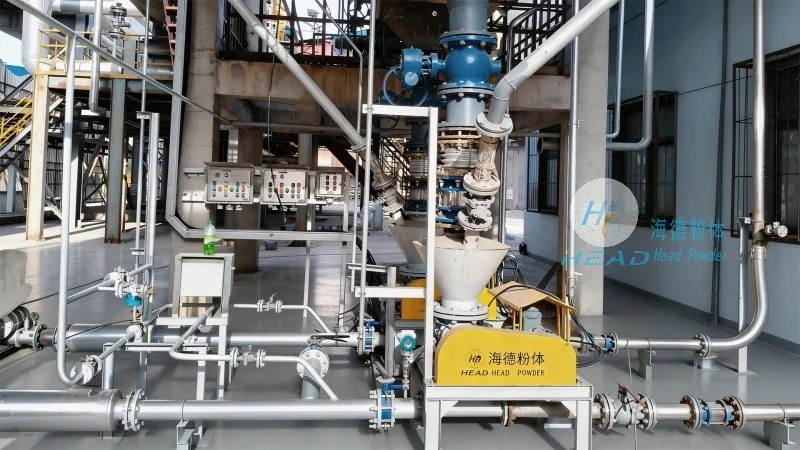
HeadPowder's pneumatic conveying equipment for rare earth mineral powders offers several key features that enhance performance and reliability. The systems are equipped with advanced control technologies, including variable frequency drives and pressure sensors, which allow for precise regulation of air flow and pressure. This ensures that the material is transported at optimal speeds, reducing energy consumption and preventing material degradation. The equipment also incorporates high-quality materials, such as stainless steel and special alloys, to withstand the corrosive and abrasive nature of rare earth powders. This durability minimizes maintenance requirements and extends the service life of the system. Another advantage is the system's ability to handle a wide range of particle sizes and moisture contents, making it versatile for different processing stages. The equipment is designed with safety features, such as dust collection and explosion-proof components, to comply with industrial safety standards. These features are particularly important in rare earth processing, where the materials can be hazardous if not handled properly. Overall, the advantages of using pneumatic conveying systems for rare earth mineral powders include improved efficiency, reduced labor costs, and enhanced product quality, making it an essential component in modern rare earth processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top