Coal ash, a byproduct of coal combustion, is commonly found in various industrial settings such as power plants and cement production facilities. The efficient and reliable transport of coal ash granular materials is crucial for maintaining operational efficiency and reducing environmental impact. Pneumatic conveying equipment has emerged as a preferred solution for handling these materials due to its ability to transport particles through air pressure, minimizing the need for mechanical components and reducing maintenance costs.
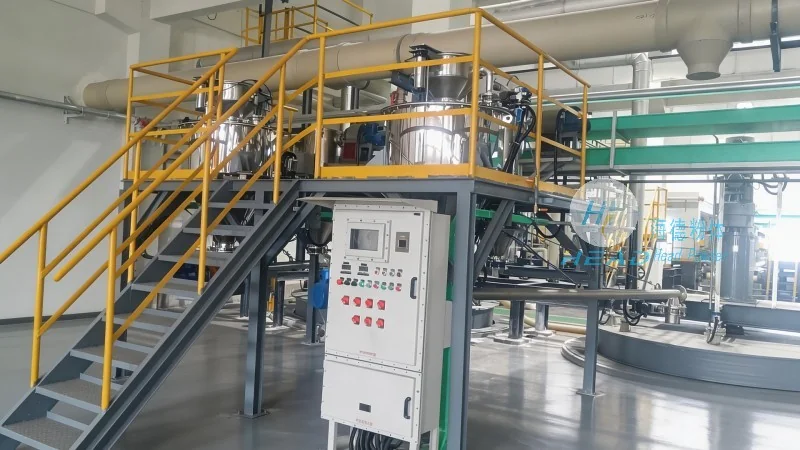
Pneumatic conveying systems operate on the fundamental principle of using air to move solid particles. In the case of coal ash, the equipment typically consists of a hopper, a conveyor line, and a receiver. The process begins with the coal ash being fed into the hopper, where it is then introduced into the conveyor line under controlled air pressure. The air, often generated by a blower or compressor, creates a flow that propels the granular material through the pipeline. This method allows for the seamless transport of coal ash from one location to another, such as from storage silos to processing units or from a power plant to a disposal site.
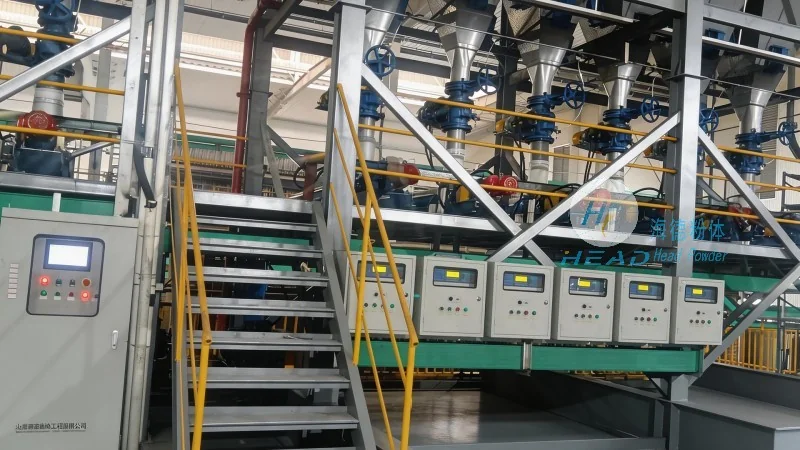
The application of coal ash pneumatic conveying equipment varies significantly based on the specific industrial environment and operational requirements. In power plants, for instance, these systems are often used to transfer coal ash from the boiler to ash handling systems, ensuring that the material is removed efficiently and without causing operational disruptions. The working scene may involve high-volume transport over short to medium distances, requiring robust equipment capable of handling large quantities of granular material without clogging or loss. In cement production, the equipment may be used to convey coal ash as a raw material for cement clinker production, where the material's fineness and moisture content are critical factors affecting the final product quality. The working scene in this context demands precise control over air flow and particle velocity to maintain consistent material characteristics.
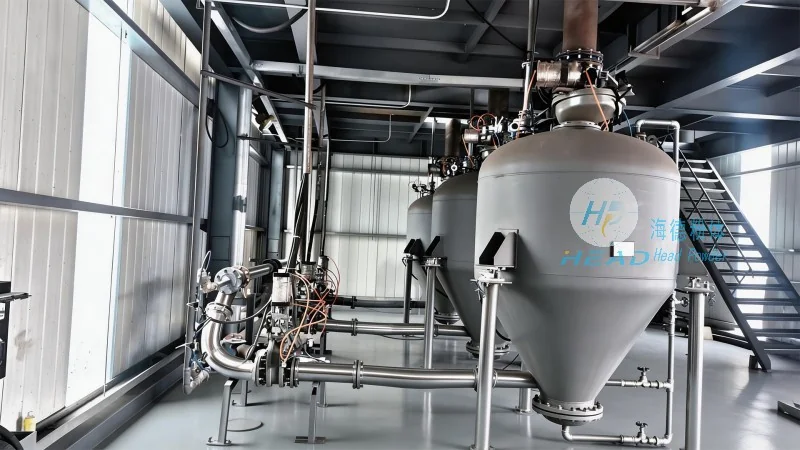
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying equipment, specializes in providing customized solutions tailored to the unique needs of coal ash handling applications. The company's systems are designed with advanced air flow management and particle handling capabilities, ensuring minimal material degradation and high transport efficiency. HeadPowder Engineering's equipment is built to withstand the abrasive nature of coal ash particles, featuring durable materials and robust construction that reduce wear and tear over time. The company's expertise in material flow dynamics allows for the optimization of conveyor line design, minimizing energy consumption and operational costs. Additionally, the systems are equipped with monitoring and control features that enable real-time tracking of material flow, enhancing operational safety and reliability.
The working scene characteristics of coal ash pneumatic conveying equipment are further enhanced by the adaptability of the systems to various industrial settings. In industrial plants located in China, such as those in Shandong province, the equipment is often integrated into existing infrastructure, requiring minimal modifications to the facility layout. The operational benefits include reduced labor costs due to automated material transport, lower environmental impact by preventing dust emissions during handling, and improved safety by eliminating manual handling of heavy or hazardous materials. The systems also contribute to increased production efficiency by ensuring a continuous and reliable supply of coal ash to processing units, minimizing downtime and maximizing output.
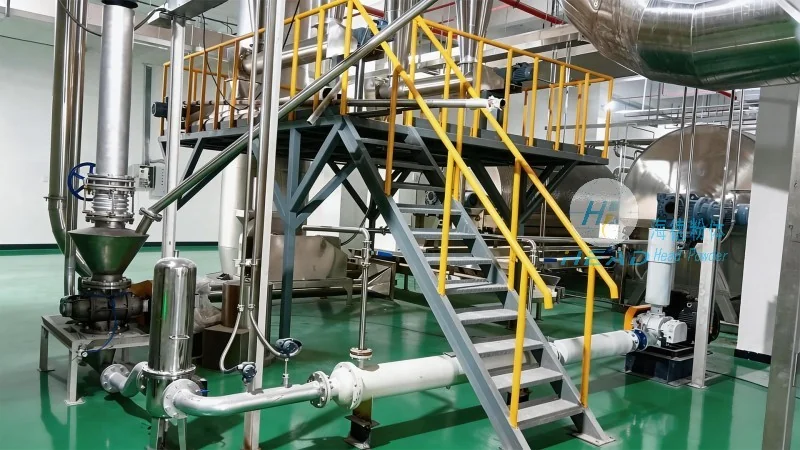
Coal ash granular material pneumatic conveying equipment plays a vital role in modern industrial operations, offering an efficient and environmentally friendly solution for material transport. By understanding the principle of air-driven transport and the specific characteristics of working scenes, industries can optimize their material handling processes. HeadPowder Engineering's commitment to innovation and quality ensures that their pneumatic conveying solutions meet the demanding requirements of coal ash management, providing long-term operational benefits and sustainable performance. The integration of advanced technology and robust design in their equipment positions them as a trusted partner for industries seeking reliable and efficient coal ash handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top