Large-scale bulk material pneumatic conveying systems represent a critical technology in modern industrial operations, enabling the efficient and reliable transport of bulk materials over significant distances. These systems are essential for industries ranging from chemical processing and mining to food and pharmaceuticals, where the movement of raw materials or finished products is a core operational requirement. The design and implementation of such systems require a deep understanding of both the physical principles governing material transport and the specific operational conditions of the application.
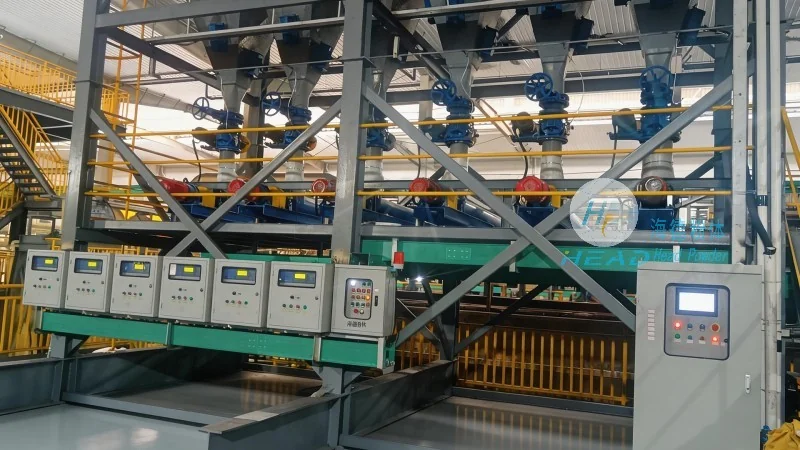
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a prominent Chinese company specializing in the design, manufacturing, and integration of advanced pneumatic conveying systems. With headquarters in Shandong, China, the company leverages decades of industry experience to deliver customized solutions tailored to the unique needs of clients worldwide. HeadPowder's commitment to innovation and quality ensures that their systems meet the highest standards of performance, safety, and durability, making them a trusted partner for businesses seeking to optimize their material handling processes.
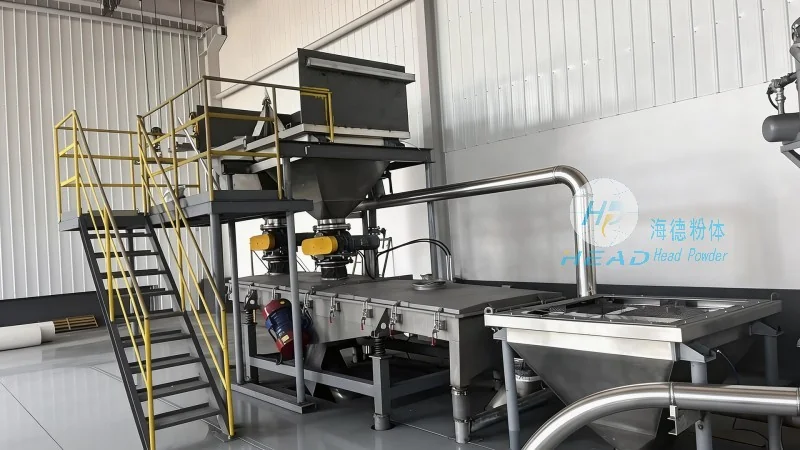
The core principle of pneumatic conveying is the use of air or other gases to transport bulk materials through a pipeline. This method can be categorized into two primary types: suction (or negative pressure) systems and pressure (or positive pressure) systems. In suction systems, a vacuum is created at the material inlet to draw the material into the pipeline, where it is then carried to the discharge point. This approach is ideal for applications requiring the transport of materials from multiple sources or over long distances where the material is to be collected from various points. Conversely, pressure systems use compressed air to push the material through the pipeline, typically from a central storage or processing unit. Pressure systems are often preferred for short to medium distance transport, where the material is already consolidated and needs to be delivered to a specific destination.
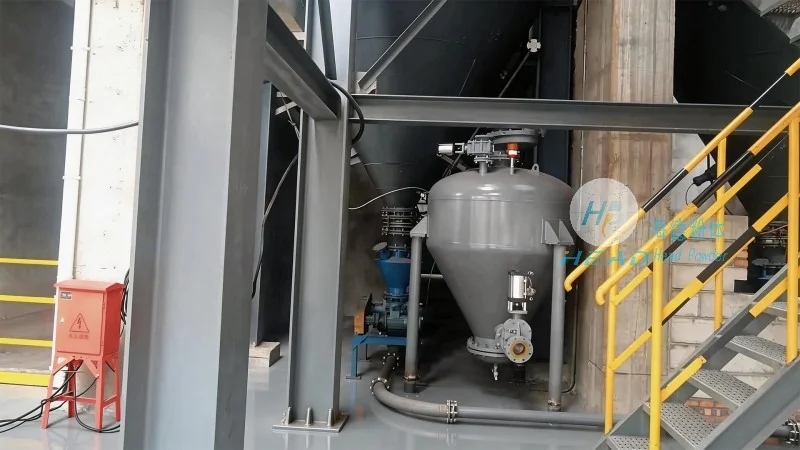
Large-scale pneumatic conveying systems are characterized by several distinct operational features that distinguish them from smaller, more localized systems. First, the scale of these systems necessitates robust and high-capacity components, including large-diameter pipelines, powerful air compressors, and advanced control systems. The ability to handle high material flow rates is a critical factor, as these systems are designed to support continuous production processes without interruption. Second, the operational flexibility of large-scale systems allows for the integration of multiple material sources and destinations, enabling complex material flow networks. This flexibility is particularly valuable in industries where materials need to be routed to different processing stages or storage locations. Third, the reliability and safety features of large-scale systems are paramount, as any downtime or failure can result in significant production losses. HeadPowder incorporates advanced monitoring and control technologies to ensure system stability and prevent operational hazards, such as material blockages or air leaks.
Large-scale pneumatic conveying systems find widespread application across a diverse range of industries, each with unique material handling requirements. In the chemical industry, for example, these systems are used to transport powders and granules for processing, such as in the production of fertilizers, plastics, or pharmaceuticals. The ability to handle abrasive or corrosive materials without causing equipment wear is a key advantage of pneumatic conveying, which is why it is preferred over mechanical systems in many chemical applications. In the mining sector, large-scale systems are employed to transport ore from mines to processing facilities, often over long distances and through challenging terrain. The durability and efficiency of pneumatic conveying make it an ideal solution for handling large volumes of raw materials in mining operations. The food and beverage industry also utilizes these systems for the transport of ingredients, such as flour, sugar, or spices, where hygiene and contamination control are critical. HeadPowder's systems are designed to meet the stringent standards of the food industry, including materials that are non-toxic, easy to clean, and resistant to corrosion.
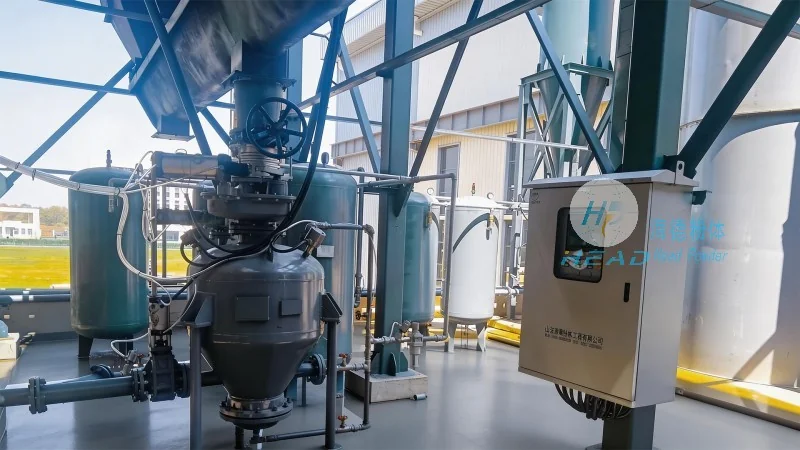
When evaluating material handling solutions, businesses often consider the advantages of pneumatic conveying over traditional mechanical methods. One of the most significant benefits is the reduction in labor costs and operational complexity. Unlike belt conveyors or bucket elevators, pneumatic systems require minimal manual intervention, as the material is transported automatically through the pipeline. This automation leads to increased efficiency and reduced human error. Additionally, pneumatic conveying systems are highly adaptable to changes in production volume, allowing businesses to scale their operations without significant modifications to the infrastructure. The ability to transport materials in a closed system also minimizes dust emissions and environmental impact, which is increasingly important for compliance with environmental regulations. HeadPowder's large-scale systems are engineered to provide these advantages while maintaining high performance and reliability, ensuring that clients achieve optimal results in their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top