HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for the handling of bulk materials such as powders and cereals. This article delves into the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in various industrial applications.
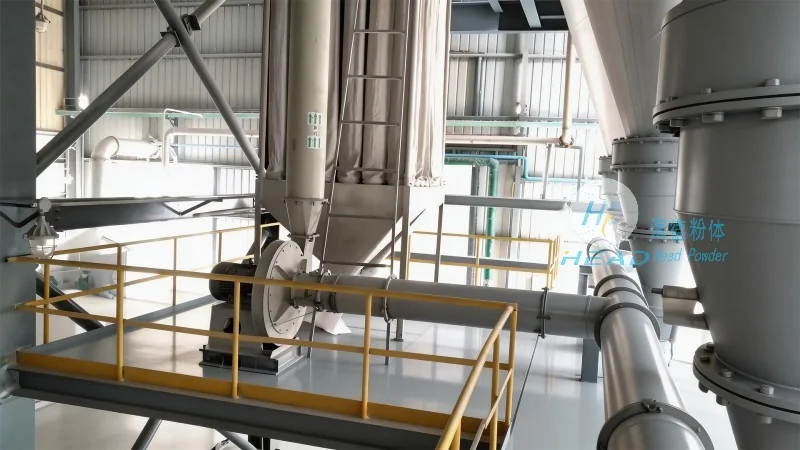
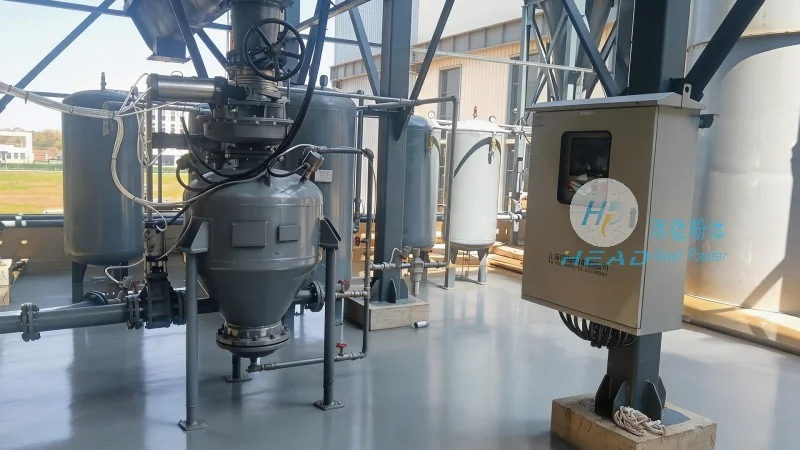
Pneumatic conveying equipment operates by using air or gas to transport bulk materials through a pipeline system. The core mechanism involves creating a pressure differential or utilizing vacuum to move the material from the source to the destination. There are primarily two types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push the material forward, while vacuum systems create a negative pressure to draw the material into the pipeline. The choice between these systems depends on factors like material properties, distance, and system layout. For instance, in handling fine powders like flour or cereal powders, pressure systems are often preferred due to their ability to maintain material integrity and prevent segregation. The equipment typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The air flow is managed by a blower or compressor, which provides the necessary pressure or vacuum to ensure efficient material transport. The design of the conveying line, including the diameter and length, is critical to maintaining the required air velocity to prevent material settling or blockages. Proper air-to-material ratio is essential to achieve optimal conveying efficiency and minimize energy consumption.
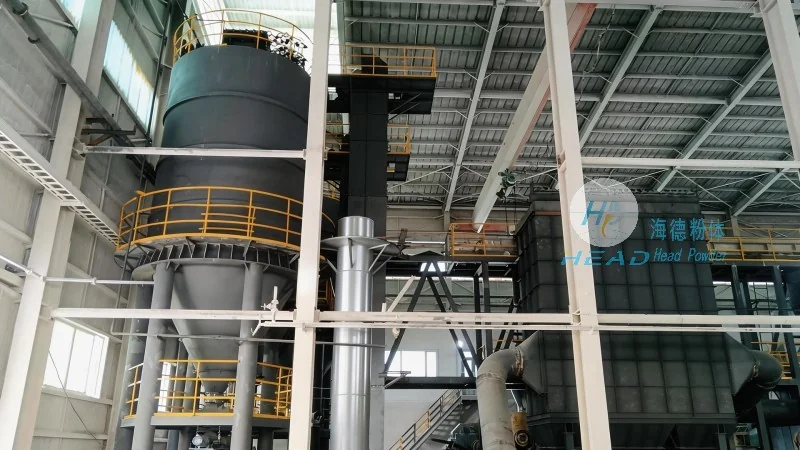
The working scene characteristics of pneumatic conveying systems are influenced by several factors that impact their performance and suitability for different applications. One of the primary characteristics is the material's physical properties, including particle size, density, and flowability. For example, handling fine powders requires systems with higher air velocities and possibly larger line diameters to prevent clogging. In contrast, handling coarse cereals or granules may involve lower air velocities and different nozzle designs to ensure smooth transport. Another important characteristic is the conveying distance and layout. For short distances, simple pressure or vacuum systems may suffice, while long-distance conveying often requires more complex systems with multiple stages or intermediate receivers to maintain pressure and prevent material degradation. The system's ability to handle variations in material flow rate is also a critical characteristic. In industrial settings, material feed rates can fluctuate due to production cycles or raw material availability. Pneumatic conveying systems must be designed to accommodate these variations without compromising efficiency or causing system failures. Additionally, the system's maintenance requirements and operational costs are key considerations for working scenes. Efficient systems should minimize downtime and reduce energy consumption, which are crucial for long-term operational economics. The integration of the conveying system with existing production lines is another important characteristic. Modern pneumatic conveying equipment is often designed to be modular and compatible with existing infrastructure, allowing for easy installation and integration without significant disruptions to production processes.
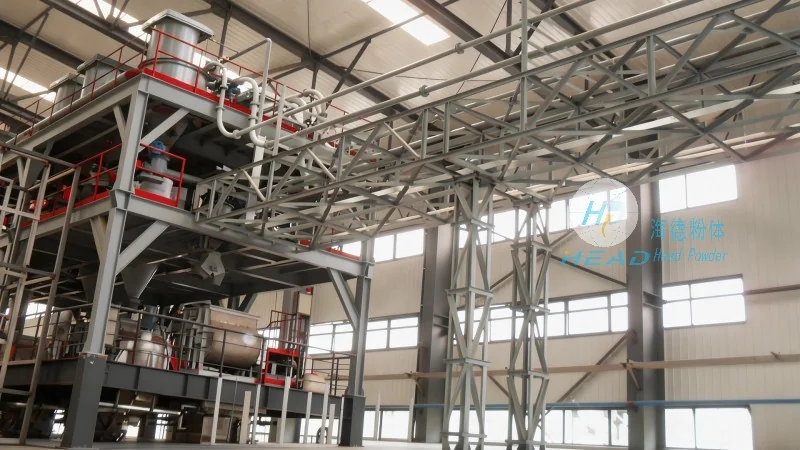
Pneumatic conveying equipment is widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, for example, it is commonly used to transport flour, sugar, and other cereal powders in bakeries and food processing plants. The advantages of using pneumatic conveying in these applications include the ability to maintain product hygiene, prevent contamination, and ensure consistent material quality. The system's enclosed design minimizes dust and particle loss, which is essential for food safety regulations. In the pharmaceutical industry, pneumatic conveying is used to transport powders and granules in manufacturing processes, where cleanliness and product integrity are paramount. The systems are often designed to meet stringent hygiene standards, with materials that are easy to clean and sanitize. In the chemical industry, pneumatic conveying is used to handle various powders and granules, including chemicals and raw materials. The ability to handle abrasive or corrosive materials is a key advantage of these systems, as they can be constructed from materials such as stainless steel to resist wear and corrosion. The mining industry also utilizes pneumatic conveying for transporting bulk materials from mines to processing facilities. The systems are designed to handle large volumes of material over long distances, often with high material densities and varying particle sizes. The advantages of pneumatic conveying in mining include reduced labor costs, improved safety (as material is transported without manual handling), and increased efficiency compared to traditional methods like trucks or conveyor belts.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top