HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust powder pneumatic conveying equipment. This article explores the fundamental principles behind these systems and highlights their key working scene characteristics, providing a comprehensive overview for industry professionals seeking efficient material handling solutions.
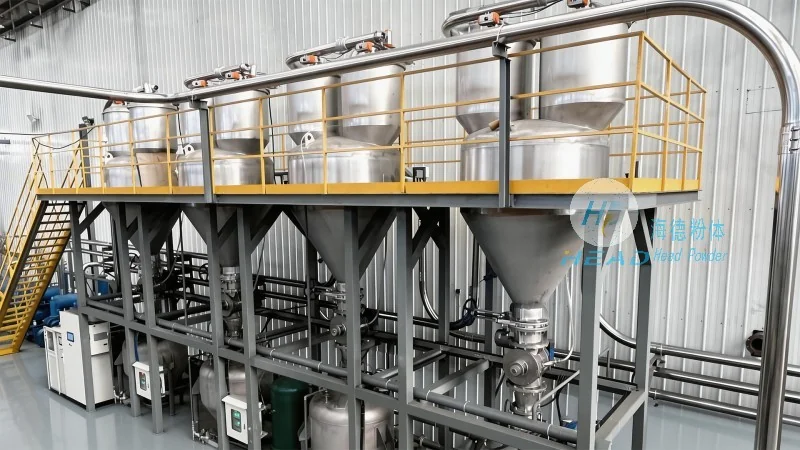
Pneumatic conveying is a widely used method for transporting dry, powdery materials such as dust and fine particles through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical conveying methods, which rely on belts, screws, or buckets, pneumatic systems offer advantages like flexibility, low maintenance, and the ability to handle materials that are difficult to transport with conventional equipment. The core principle involves creating a pressure differential or using vacuum to move the material through the pipeline, ensuring safe and efficient transfer from the source to the destination.
The operation of dust powder pneumatic conveying equipment is based on the interaction between the material and the conveying air. In a typical system, the powder is fed into a hopper or feeder, where it is then introduced into a pipeline. The system uses either positive pressure (where air is blown into the line to push the material) or negative pressure (where air is drawn out to pull the material). The key components include the feeder, pipeline, and discharge device, each playing a critical role in the overall conveying process. The feeder ensures a consistent flow of material, the pipeline transports it, and the discharge device controls the release at the destination. This integrated approach allows for precise control over the conveying rate and material handling, minimizing product degradation and ensuring high efficiency.
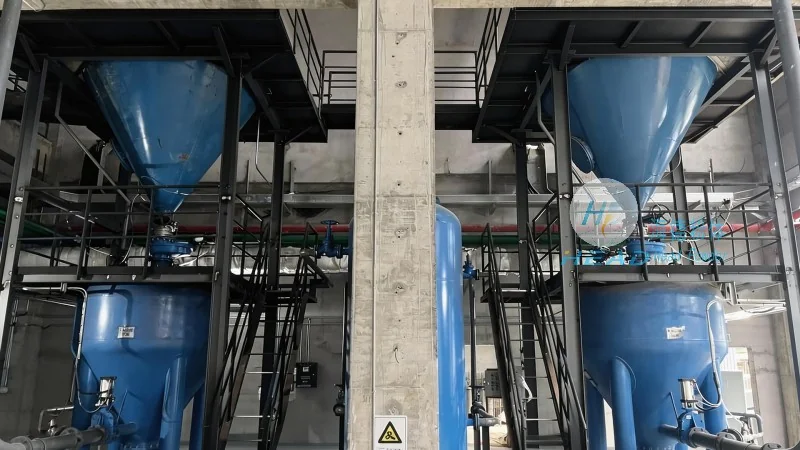
The working scene characteristics of dust powder pneumatic conveying equipment are tailored to meet the specific demands of various industrial applications. These systems are particularly effective in environments where dust and fine particles need to be handled without causing contamination or loss. Some key characteristics include:
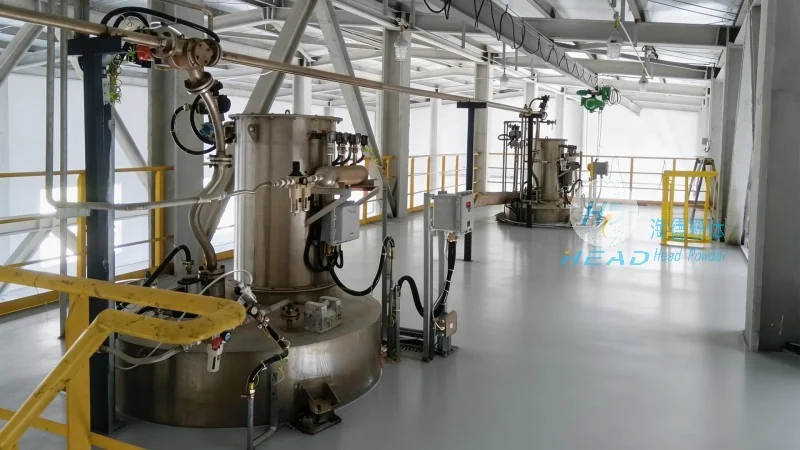
Dust powder pneumatic conveying equipment is widely used across various industries, including chemical, food processing, pharmaceuticals, and mining. In the chemical industry, it is used to transport powders such as pigments, catalysts, and raw materials, ensuring safe and efficient handling. The food and pharmaceutical sectors benefit from the hygienic design of these systems, which prevents cross-contamination and maintains product quality. Mining operations use pneumatic conveying to transport ore and fine particles from processing plants to storage or further processing facilities. The versatility of these systems makes them suitable for a wide range of applications, from small-scale operations to large industrial plants.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of dust powder pneumatic conveying equipment. With a focus on innovation and quality, the company offers advanced solutions that meet the diverse needs of industrial applications. By understanding the fundamental principles and working scene characteristics of these systems, businesses can enhance their material handling processes, improve efficiency, and reduce operational costs. For more information about their products and services, please contact HeadPowder directly.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top