Ammonia fertilizer is a critical component in contemporary agricultural practices, supplying essential nitrogen to boost crop yields and soil fertility. The efficient and safe handling of ammonia fertilizer is vital for both agricultural productivity and operational safety. This article explores the principles and working characteristics of specialized equipment designed for ammonia fertilizer material handling, highlighting technical aspects and practical applications in various agricultural settings.
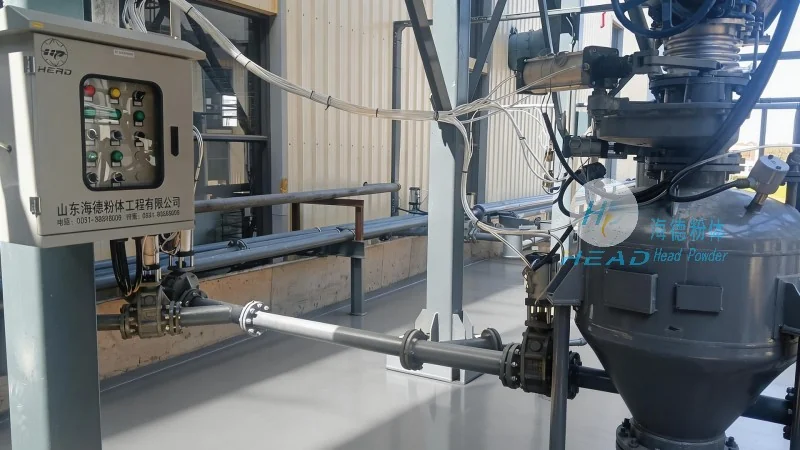
HeadPowder, as a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and integration of advanced material handling systems for the fertilizer industry. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for agricultural and industrial clients seeking reliable solutions for ammonia fertilizer processing and transportation. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technologies tailored to the specific needs of the fertilizer sector.
The core principle of ammonia fertilizer material handling systems centers on the safe and efficient transfer of liquid or solid ammonia-based fertilizers from storage to application points. These systems typically integrate several key components, including storage tanks, pumps, conveyors, and control systems, all engineered to operate under strict safety protocols due to the hazardous nature of ammonia. The equipment is designed to handle the corrosive and volatile properties of ammonia, ensuring minimal leakage and optimal performance under varying operational conditions. Advanced materials, such as stainless steel and specialized coatings, are used in system component construction to withstand chemical exposure and maintain structural integrity over time.
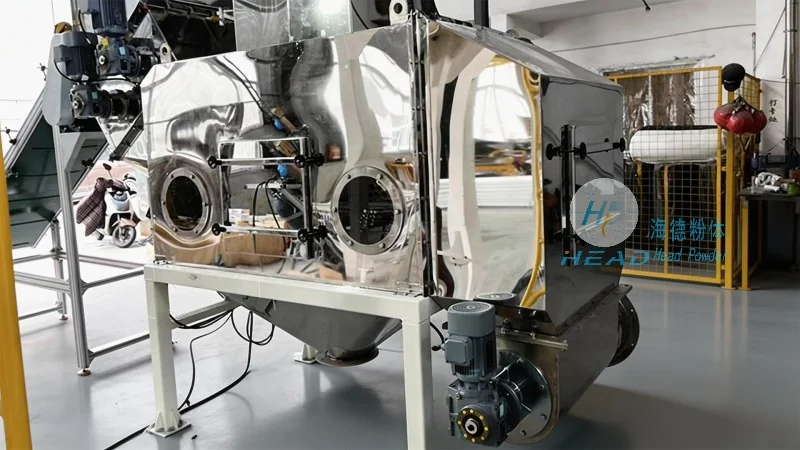
The working scene characteristics of ammonia fertilizer material handling systems are influenced by factors like fertilizer type (liquid or solid), operational scale, and specific agricultural environment. For liquid ammonia fertilizer, systems often feature closed-loop pipelines and automated dosing mechanisms to ensure precise application rates, minimizing waste and environmental impact. Solid ammonia fertilizer handling may involve bulk storage silos, screw conveyors, and pneumatic transport systems, which require robust mechanisms to prevent caking and ensure consistent flow. The equipment is designed to operate in diverse climates, from temperate regions to tropical agricultural zones, with features like temperature regulation and weather-resistant enclosures to maintain functionality under adverse conditions.
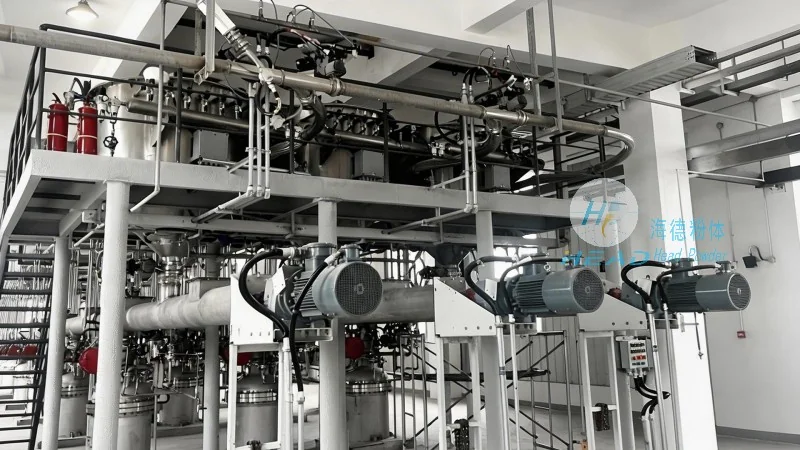
HeadPowder's ammonia fertilizer material handling systems are distinguished by comprehensive design addressing operational efficiency and safety. The systems incorporate advanced control technologies, such as PLC (Programmable Logic Controller) systems, to monitor and regulate flow rates, pressure, and temperature in real-time. This automation enhances precision in fertilizer application, reduces human error, and ensures compliance with safety standards. Additionally, the systems are equipped with emergency shutdown mechanisms and leak detection sensors, providing immediate response to potential hazards and safeguarding personnel and the environment. The modular design of these systems allows for easy integration with existing agricultural infrastructure, enabling clients to upgrade or expand fertilizer handling capabilities without significant operational disruption.
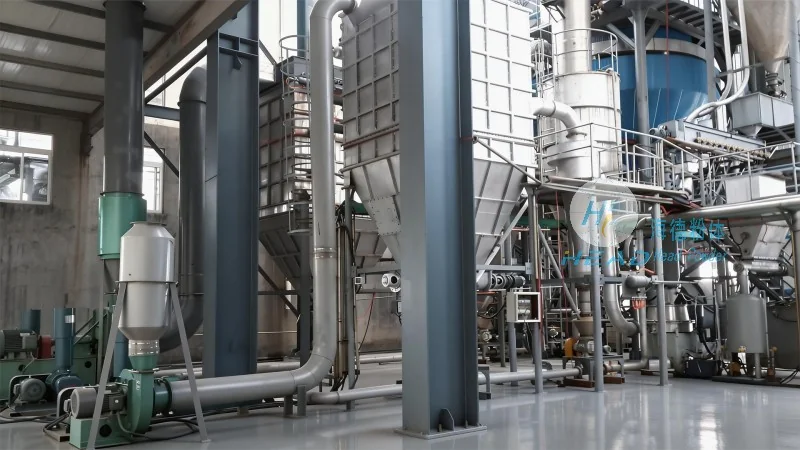
The working scene characteristics of ammonia fertilizer handling equipment are evident in various agricultural applications, from large-scale commercial farms to smaller family-owned operations. In commercial settings, these systems support high-volume fertilizer application, enabling farmers to meet the nutritional demands of extensive crop rotations while optimizing resource utilization. For smaller operations, compact and portable systems are available, providing flexibility in handling smaller quantities of fertilizer without compromising on safety or efficiency. The operational benefits of these systems extend beyond efficiency; they also reduce labor costs as automated processes minimize manual handling of hazardous materials. Furthermore, consistent fertilizer application quality leads to improved crop yields and soil health, ultimately enhancing the economic viability of agricultural enterprises.
In conclusion, the ammonia fertilizer material handling systems developed by Shandong HeadPowder Engineering Co., Ltd. represent a sophisticated solution to modern agricultural fertilizer management challenges. By integrating advanced engineering principles with robust safety features, these systems ensure efficient and secure handling of ammonia-based fertilizers across diverse working scenes. As agricultural practices continue to evolve, the demand for reliable and innovative material handling solutions will remain high, positioning HeadPowder as a key player in meeting future fertilizer industry needs. The company's commitment to quality, innovation, and customer satisfaction ensures its systems will continue to play a vital role in supporting sustainable agricultural development worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top