HeadPowder, a leading provider of industrial conveying systems, specializes in advanced pneumatic conveying solutions tailored for mineral sands and other bulk powders. The company, based in Shandong, China, leverages cutting-edge technology to address the challenges of transporting fine and abrasive materials efficiently and reliably. This article explores the principles and applications of pneumatic conveying systems designed specifically for mineral sands, highlighting how air flow can be optimized to enhance material handling performance.
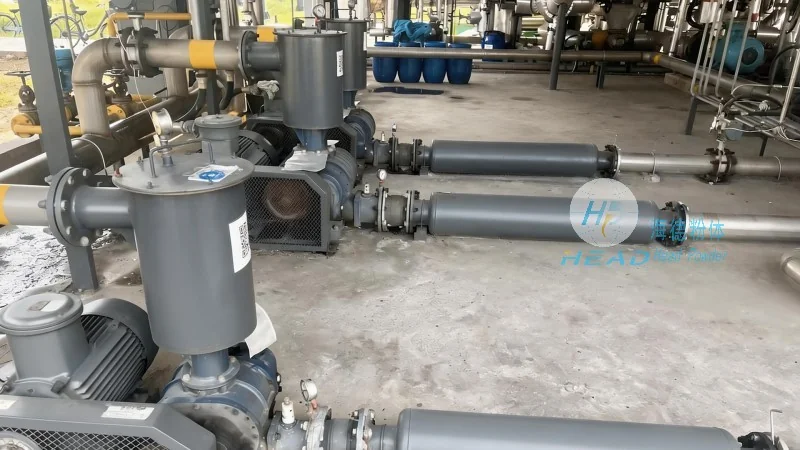
Pneumatic conveying systems operate by using air pressure to move powders and granules through a pipeline. For mineral sands, which often consist of fine particles with high abrasiveness, the design of the conveying system is critical. HeadPowder’s engineers focus on selecting appropriate air velocities, pipeline diameters, and material handling components to ensure minimal wear and optimal flow. The system typically involves a hopper or feeder that feeds the material into a pipeline, where compressed air propels the particles forward. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing safety in handling potentially hazardous materials.
Effective pneumatic conveying of mineral sands relies on several key components. The feed system, which may include a rotary valve or a screw feeder, ensures a consistent flow of material into the pipeline. The pipeline itself is constructed from durable materials, such as stainless steel or special alloys, to withstand the abrasive nature of mineral sands. HeadPowder’s systems often incorporate pulse-jet or venturi designs to maintain consistent air flow and prevent material buildup. The receiver or discharge unit at the end of the pipeline collects the conveyed material, and may include a dust collection system to ensure environmental compliance. The company’s expertise lies in customizing these components to match the specific characteristics of the mineral sands being handled, such as particle size, density, and moisture content.
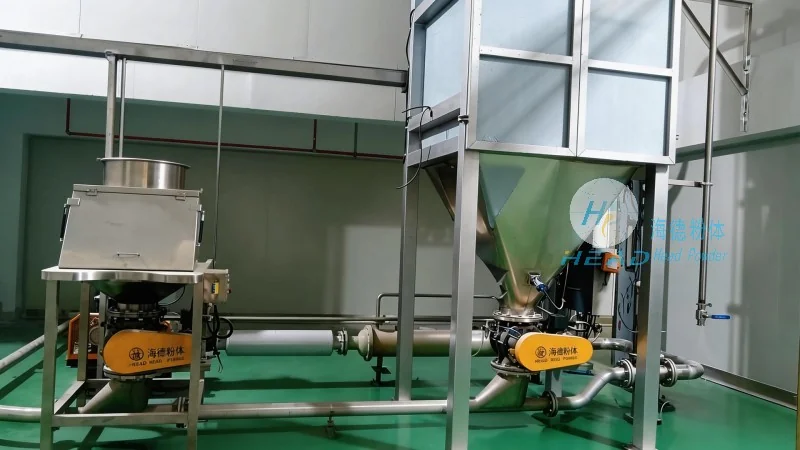
Compared to traditional mechanical conveying methods, pneumatic systems offer several advantages for mineral sands applications. The primary benefit is the ability to transport materials over long distances without the need for intermediate transfer points. This reduces downtime and improves overall operational efficiency. Additionally, pneumatic conveying minimizes product contamination, as the material is not in direct contact with mechanical parts. The system also provides better control over material flow, allowing for precise dosing and batching. For mineral sands, which are often used in high-value applications like mining and processing, these advantages translate into cost savings and improved product quality. HeadPowder’s systems are designed to handle the specific challenges of mineral sands, such as high abrasiveness and fine particle size, ensuring reliable and efficient operation.
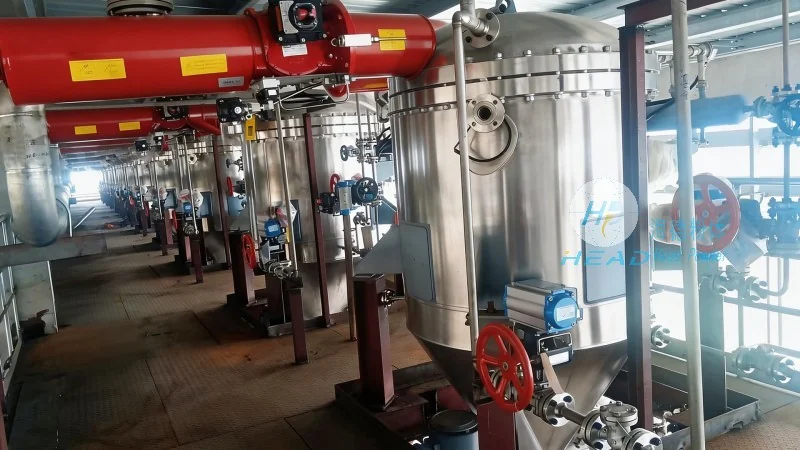
The versatility of pneumatic conveying systems makes them suitable for a wide range of mineral sands applications. In mining operations, these systems are used to transport ore from the mine to processing facilities, often over long distances. In industrial processing, they are employed to move mineral sands from storage silos to production lines, ensuring a steady supply of raw material. HeadPowder has successfully implemented pneumatic conveying solutions for clients in the mining, chemical, and food processing industries. For example, a client in Shandong used a HeadPowder system to transport fine mineral sands from a hopper to a processing plant, achieving a 30% reduction in handling time and a 15% decrease in maintenance costs. Another application involved the transport of abrasive mineral sands in a chemical plant, where the HeadPowder system’s durable components and optimized air flow reduced wear and extended equipment life.
HeadPowder understands that each mineral sands operation has unique requirements. The company offers customized pneumatic conveying solutions tailored to the specific needs of its clients. This includes designing systems that can handle varying particle sizes, moisture levels, and abrasive properties. HeadPowder’s team of engineers works closely with clients to assess their operational needs and recommend the most suitable conveying system. The company also provides comprehensive after-sales service, including maintenance, repair, and technical support. With a focus on quality and reliability, HeadPowder ensures that its clients receive systems that meet their performance and safety standards. The company’s commitment to customer satisfaction is reflected in its long-term partnerships with clients across China and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top