For malt processing facilities, the efficient and reliable transport of malt using pneumatic conveying systems is crucial. However, one of the primary challenges in this process is the risk of pipeline blockages, which can lead to downtime, increased maintenance costs, and reduced productivity. Understanding the root causes of blockages and implementing appropriate design parameters is essential to ensure smooth operation. This article explores how pneumatic conveying systems can be optimized to prevent blockages in malt transport and highlights the key design parameters that contribute to their effectiveness.
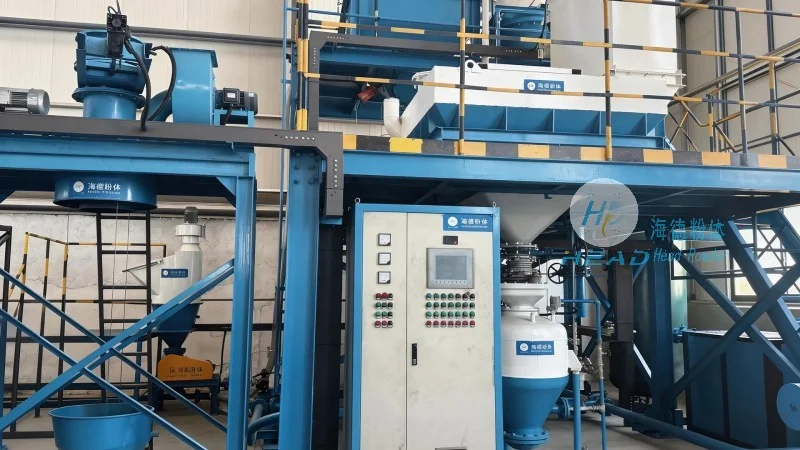
Pneumatic conveying systems utilize air or gas to transport bulk materials like malt through a pipeline. These systems are widely used in the food and beverage industry due to their ability to handle delicate materials without causing damage. The basic principle involves creating a pressure differential between the inlet and outlet of the pipeline, which propels the malt forward. However, the nature of malt—its moisture content, particle size distribution, and flow characteristics—makes it susceptible to bridging, rat-holing, and other blockage issues if the system is not properly designed.
Several factors contribute to blockages in pneumatic conveying systems for malt. One of the main causes is the high moisture content of malt, which can cause the material to stick to the pipe walls, leading to bridging. Another factor is the particle size distribution; if the particles are too fine or too large, they may not flow uniformly, causing uneven pressure distribution and potential blockages. Additionally, the presence of foreign materials or agglomerates can obstruct the pipeline. Inadequate air velocity or pressure can also lead to insufficient transport capacity, causing the material to settle and form blockages.
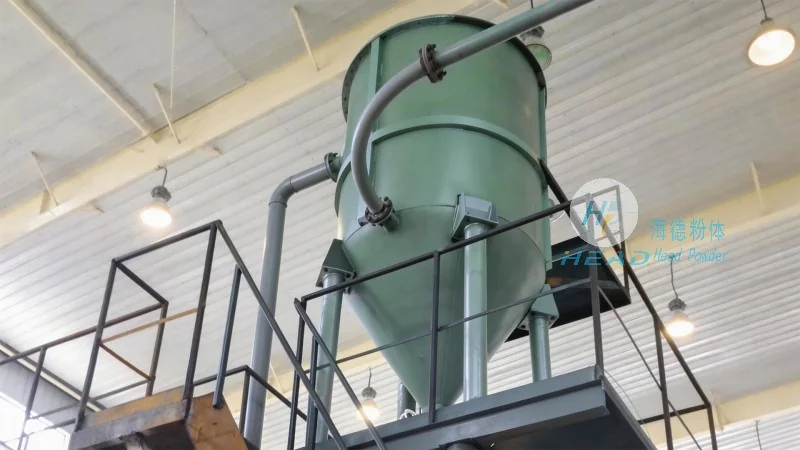
Optimizing the design of a pneumatic conveying system for malt transport involves several critical parameters. The first is the air velocity, which must be sufficient to maintain the material in suspension and prevent it from settling. For malt, an air velocity of 20-30 meters per second is typically recommended to ensure proper flow. The second parameter is the pressure differential; maintaining an appropriate pressure gradient is essential to propel the malt through the pipeline without causing excessive wear or energy consumption. The pipe diameter is another critical factor; larger diameters reduce friction losses and the risk of blockages, but they also increase capital costs. For malt transport, a pipe diameter of 100-150 mm is commonly used, depending on the material flow rate.
The physical properties of malt, such as its bulk density and angle of repose, significantly impact the system's performance. Bulk density affects the required air volume, while the angle of repose determines the material's flowability. A lower angle of repose indicates better flowability, reducing the risk of blockages. To mitigate issues related to flow characteristics, some systems incorporate vibrators or agitators to break up agglomerates and ensure uniform flow. Additionally, the use of flexible hoses or expansion joints can help accommodate thermal expansion and reduce stress on the pipeline, preventing cracks that could lead to blockages.
Effective separation and cleaning systems are vital components of a pneumatic conveying system designed to prevent blockages. The system typically includes a cyclone separator or a filter to remove dust and fine particles from the air stream. These components help maintain the air quality and prevent clogging of downstream equipment. Regular cleaning of the separator and filter is necessary to ensure optimal performance. Furthermore, incorporating a pressure relief valve or a venting system can help manage excess pressure and prevent over-pressurization, which could cause the pipeline to rupture or lead to blockages.
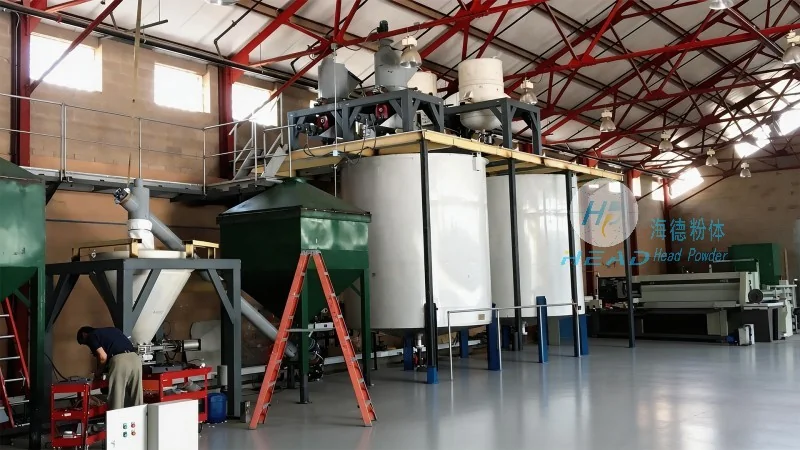
The integration of the pneumatic conveying system with other processing equipment, such as mixers or storage silos, is crucial for preventing blockages. Proper alignment and sealing of connections between the system and other equipment reduce the risk of material leakage or air leakage, which can affect the system's performance. Regular maintenance, including inspections of the pipeline for signs of wear or corrosion, is essential to identify and address potential issues before they lead to blockages. Additionally, training operators on the proper operation of the system and the importance of monitoring key parameters (such as pressure and flow rate) can help prevent human error-related blockages.
Preventing pipeline blockages in pneumatic conveying systems for malt transport requires a comprehensive approach that considers the material's properties, system design, and operational practices. By optimizing key design parameters such as air velocity, pressure, pipe diameter, and material handling techniques, and by implementing effective separation and maintenance strategies, malt processing facilities can ensure the reliable and efficient operation of their conveying systems. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder) in designing and implementing such systems is invaluable for achieving optimal performance and minimizing downtime in malt transport operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top