Nitrogen-protected material conveying lines are critical industrial systems designed to maintain an inert atmosphere during the transport of sensitive materials. These systems play a vital role in preventing oxidation, moisture absorption, and contamination, which are common challenges in industries such as food processing, pharmaceuticals, and chemical manufacturing. By utilizing nitrogen gas to displace oxygen and other reactive gases, these lines ensure the integrity and quality of the conveyed materials throughout the entire process.
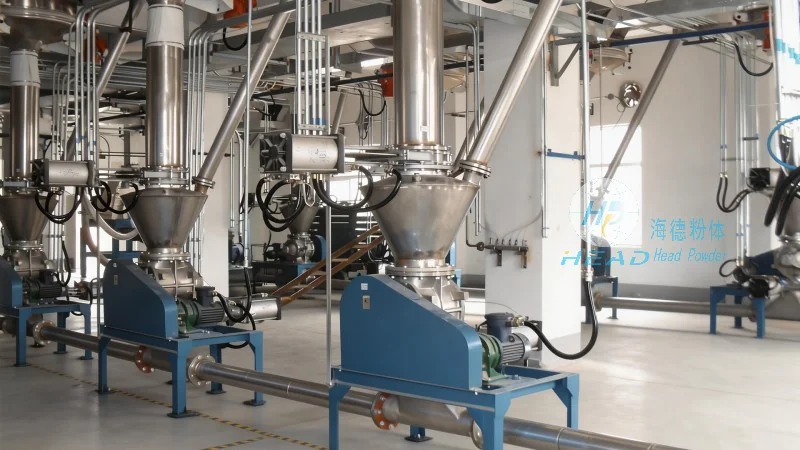
The core principle of nitrogen-protected material conveying lines revolves around creating and maintaining an inert environment within the conveying system. This is achieved by introducing high-purity nitrogen gas into the conveyor's interior, effectively displacing ambient air that contains oxygen and moisture. The nitrogen gas acts as a protective barrier, preventing direct contact between the material and oxygen, which can lead to degradation, spoilage, or safety hazards. The system typically includes components such as nitrogen gas generators, pressure regulators, and sealed conveyor components to ensure consistent and reliable protection. The nitrogen flow is carefully controlled to maintain a positive pressure within the system, preventing external contaminants from entering and compromising the material's quality.
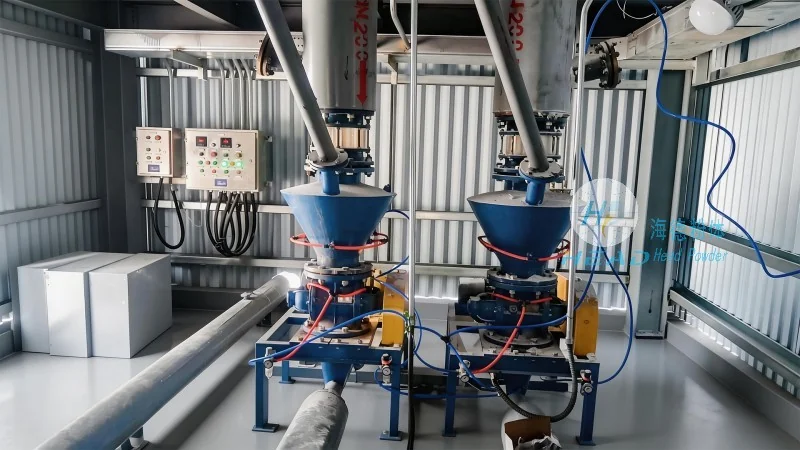
The application of nitrogen-protected material conveying lines varies across different industrial sectors, each with unique requirements and challenges. In the food industry, for example, these systems are used to transport perishable products like grains, powders, and spices, where oxidation can cause rancidity and loss of nutritional value. The nitrogen atmosphere helps preserve the freshness and flavor of the food products, extending their shelf life and ensuring consumer safety. In the pharmaceutical sector, nitrogen-protected conveying lines are essential for handling active pharmaceutical ingredients (APIs) and finished drug products, as they are highly sensitive to moisture and oxygen, which can affect their efficacy and stability. The inert environment prevents degradation and contamination, meeting stringent regulatory standards. In the chemical industry, these systems are employed for transporting reactive or hazardous materials, where exposure to air can lead to dangerous reactions or product degradation. The nitrogen protection ensures safe and reliable material handling, reducing the risk of accidents and environmental contamination.
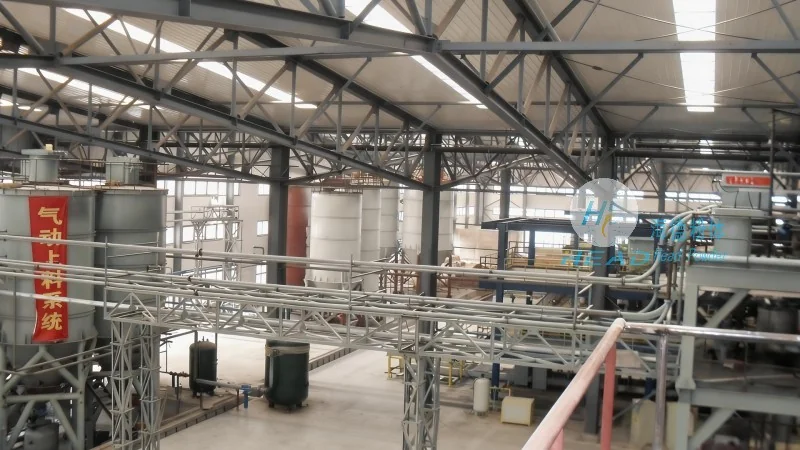
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling systems, including nitrogen-protected conveying lines. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner in various industries. The company's engineering team leverages years of experience and cutting-edge technology to design and manufacture customized conveying systems that meet the specific needs of clients. HeadPowder's nitrogen-protected material conveying lines are engineered to deliver consistent performance, high efficiency, and long-term reliability. The systems are equipped with advanced monitoring and control features, allowing for real-time tracking of the conveying process and ensuring optimal nitrogen usage. By partnering with HeadPowder, businesses can enhance their material handling capabilities, improve product quality, and reduce operational costs. The company's commitment to quality and customer satisfaction has made it a preferred choice for companies seeking reliable and effective nitrogen protection solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top