Positive pressure material conveying lines represent a sophisticated approach to material handling, particularly in industries where dust control, product integrity, and efficient transport are critical. This article explores the underlying principles of these systems and highlights key operational scenarios where their application proves advantageous.
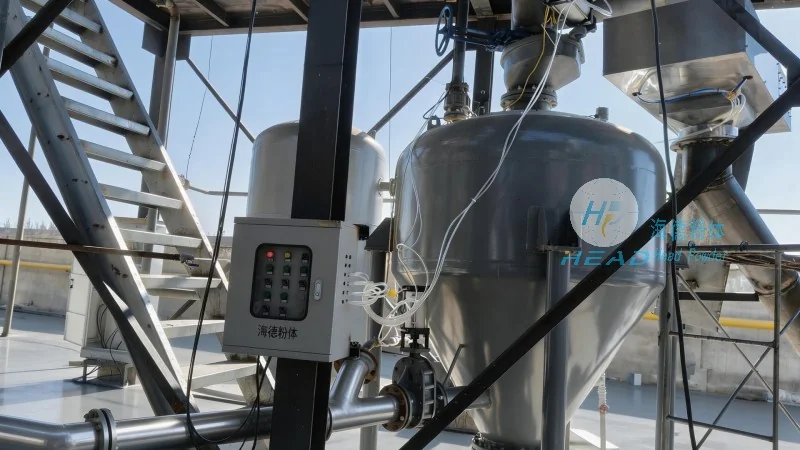
At the heart of positive pressure material conveying is the use of pressurized air to move bulk materials from one location to another. Unlike traditional suction systems that rely on negative pressure, positive pressure systems generate an air flow that pushes material through a sealed pipeline. This method ensures that the material is contained within a controlled environment, minimizing dust emissions and preventing contamination. The system typically consists of a blower or fan that supplies compressed air, a hopper or feeder to introduce the material, and a series of ducts or pipes that transport the material to its destination. The air pressure is carefully regulated to maintain a consistent flow rate, ensuring reliable and continuous operation. This design not only enhances safety by containing particulate matter but also improves the overall efficiency of material transport by reducing energy waste and preventing material degradation.
Positive pressure material conveying lines are widely utilized across various industries due to their adaptability and effectiveness. In the pharmaceutical sector, for instance, these systems are essential for transporting powders and granules in sterile environments, where contamination control is paramount. The sealed pipeline prevents cross-contamination and maintains the integrity of sensitive products. Similarly, in the food processing industry, positive pressure conveying ensures that food-grade materials are handled hygienically, with minimal exposure to external elements. The system’s ability to maintain a positive pressure environment helps in preserving the quality and safety of the products being transported.
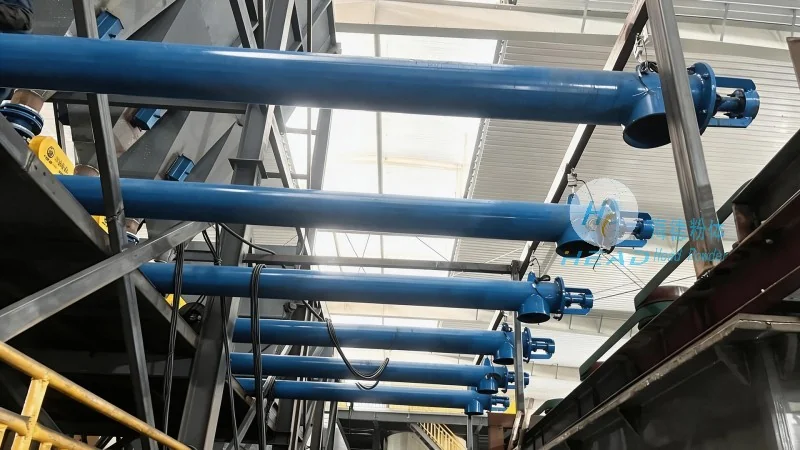
In the chemical industry, positive pressure conveying is employed for handling hazardous or reactive powders, where dust explosion prevention is a critical concern. By containing the material within a pressurized system, the risk of ignition and explosion is significantly reduced. The technology also finds applications in the mining and construction sectors, where bulk materials such as coal, sand, or cement are transported over long distances with high efficiency. The consistent air pressure and sealed design ensure that the material is delivered without spillage or loss, optimizing the overall material handling process.
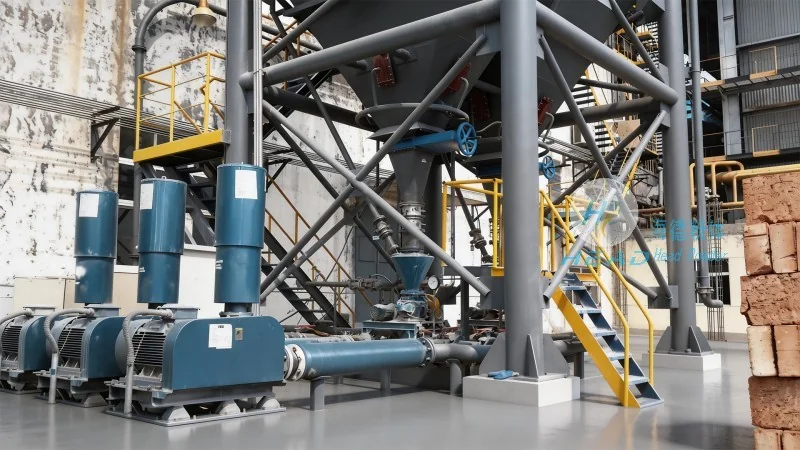
One of the primary advantages of positive pressure material conveying is its ability to handle a wide range of materials, from fine powders to larger granules, with minimal maintenance. The sealed system reduces the need for cleaning and prevents material buildup in the ductwork, which can lead to clogging and reduced efficiency. Additionally, the pressurized air flow helps in maintaining a consistent material flow rate, even when dealing with varying material densities or moisture content. However, operational considerations must be taken into account, such as the need for proper air filtration to prevent dust accumulation in the system and the importance of regular maintenance to ensure the blower and other components function optimally. Proper sizing of the blower and ducts is also crucial to maintain the desired pressure and flow rate, avoiding issues like excessive energy consumption or insufficient material transport.
Positive pressure material conveying lines offer a reliable and efficient solution for material handling in various industrial applications. By leveraging pressurized air to transport materials in a controlled environment, these systems enhance safety, maintain product quality, and improve operational efficiency. As industries continue to prioritize sustainability and process optimization, the adoption of such technology remains a strategic choice for companies seeking to enhance their material handling capabilities. With its adaptability and effectiveness, positive pressure conveying is set to remain a vital component in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top