The calcined ash powder conveying system is a specialized industrial solution designed to handle and transport calcined ash, a byproduct commonly generated in power plants and other industrial facilities. As a key component in material handling, this system ensures efficient and reliable movement of the powder, addressing the unique challenges associated with calcined ash's properties such as high temperature, abrasive nature, and potential moisture content. The system's design integrates advanced engineering principles to meet the demands of modern industrial applications, providing a robust solution for safe and effective material transport.
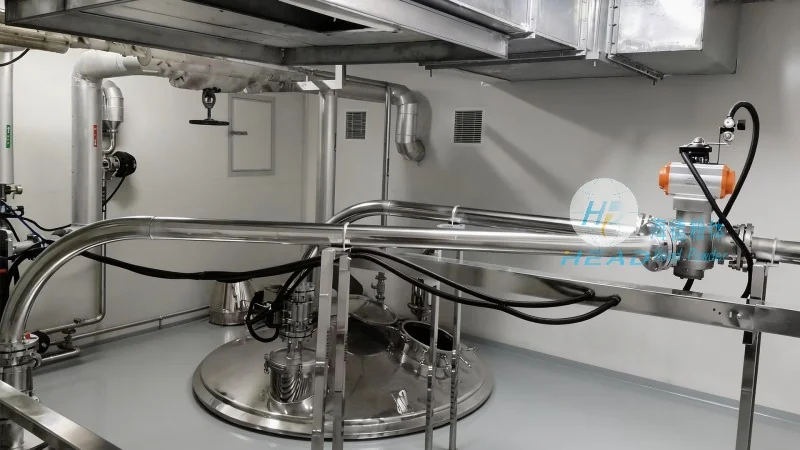
The fundamental principle of the calcined ash powder conveying system revolves around the use of positive pressure or negative pressure air flow to transport the powder. The system typically employs a combination of airlocks, rotary valves, and ductwork to create a sealed environment that prevents dust leakage and maintains operational safety. The positive pressure method involves blowing air into the system to push the powder through the ducts, while the negative pressure method uses suction to draw the powder. Both approaches are engineered to handle the high temperature and abrasive characteristics of calcined ash, ensuring durability and minimal wear on components. The system's design also incorporates temperature control mechanisms to manage the heat generated during the conveying process, protecting equipment and maintaining material integrity.
The calcined ash powder conveying system consists of several critical components, each playing a vital role in the overall operation. The primary components include the ash hopper, which stores the calcined ash before transport; the feeder, which controls the flow rate of the powder into the system; the air compressor or vacuum pump, which provides the necessary pressure or suction; the conveying ducts, which transport the powder from the hopper to the destination; and the discharge equipment, which releases the powder at the receiving point. The ash hopper is designed with heat-resistant materials to withstand the high temperatures of the calcined ash, while the feeder ensures a consistent and controlled flow, preventing blockages and ensuring smooth operation. The air compressor or vacuum pump is selected based on the system's capacity and the specific requirements of the application, providing the necessary pressure or suction to move the powder efficiently. The conveying ducts are made of durable, corrosion-resistant materials to handle the abrasive nature of the calcined ash, with smooth surfaces to minimize friction and wear. The discharge equipment, such as rotary valves or airlocks, ensures that the powder is released safely and without dust emissions, maintaining environmental compliance and operational safety.
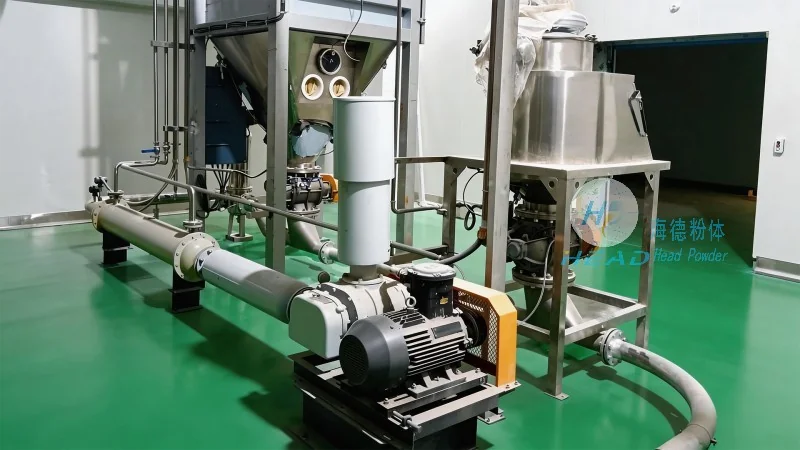
The calcined ash powder conveying system is widely used in various industrial settings, particularly in power plants, where calcined ash is a byproduct of coal combustion. The system's working scene characteristics are tailored to the specific requirements of these applications, ensuring optimal performance and efficiency. In power plants, the system is typically integrated into the ash handling system, transporting calcined ash from the boiler to the storage or disposal site. The system is designed to handle large volumes of ash, with capacities ranging from several tons per hour to hundreds of tons per hour, depending on the plant's size and output. The working scene also includes considerations for environmental regulations, as the system must comply with dust emission standards and ensure minimal environmental impact. Additionally, the system's design accommodates the varying properties of calcined ash, such as changes in moisture content or particle size, which can affect the conveying efficiency. The working scene characteristics also include the need for maintenance and operational flexibility, as the system must be easily accessible for inspections and repairs, and capable of adapting to changes in the plant's operational needs.
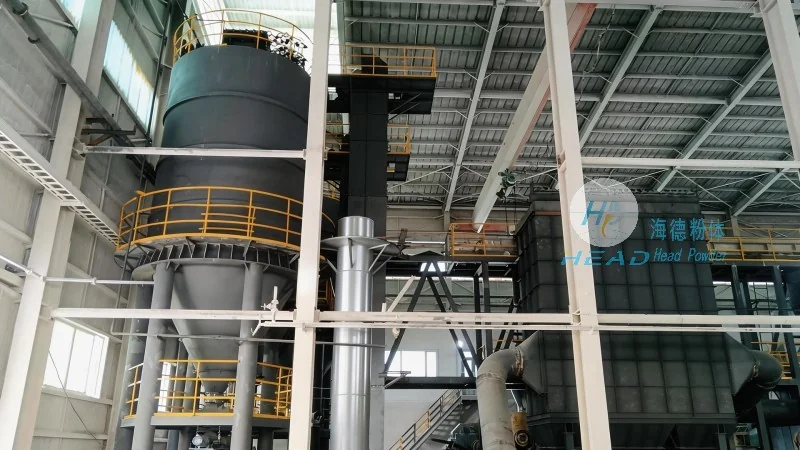
The calcined ash powder conveying system offers several advantages and benefits that make it an ideal solution for industrial applications. One of the primary benefits is its efficiency in handling large volumes of calcined ash, reducing the need for manual handling and improving overall operational productivity. The system's design minimizes dust emissions, enhancing workplace safety and compliance with environmental regulations. Additionally, the system's durability and resistance to wear and corrosion ensure long-term reliability and low maintenance costs. The system's flexibility allows it to be integrated into existing industrial setups, minimizing the need for major modifications or new infrastructure. The use of advanced materials and engineering techniques also ensures that the system can handle the high temperatures and abrasive nature of calcined ash, providing a robust and reliable solution for material transport. Furthermore, the system's ability to maintain material integrity during transport is crucial, as calcined ash is often used in other industrial processes, and maintaining its quality is essential for downstream applications.
The calcined ash powder conveying system is a critical component in industrial material handling, providing an efficient and reliable solution for transporting calcined ash. Its design, based on advanced engineering principles, addresses the unique challenges associated with calcined ash's properties, ensuring safe and effective operation. The system's components are carefully selected and engineered to meet the demands of modern industrial applications, offering durability, efficiency, and environmental compliance. As a leading provider of industrial solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing calcined ash powder conveying systems tailored to the specific needs of clients. With a focus on quality, innovation, and customer satisfaction, the company provides comprehensive support, including design, installation, and maintenance services. Located in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise and experience to deliver high-performance conveying systems that enhance operational efficiency and ensure long-term reliability. The company's commitment to excellence and customer-centric approach makes it a trusted partner for industrial clients seeking reliable material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top