HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and manufacturing of pneumatic conveying systems tailored for calcium carbonate powder applications. This article explores the fundamental principles behind these systems and highlights the key operational characteristics that define their effectiveness in various industrial settings.
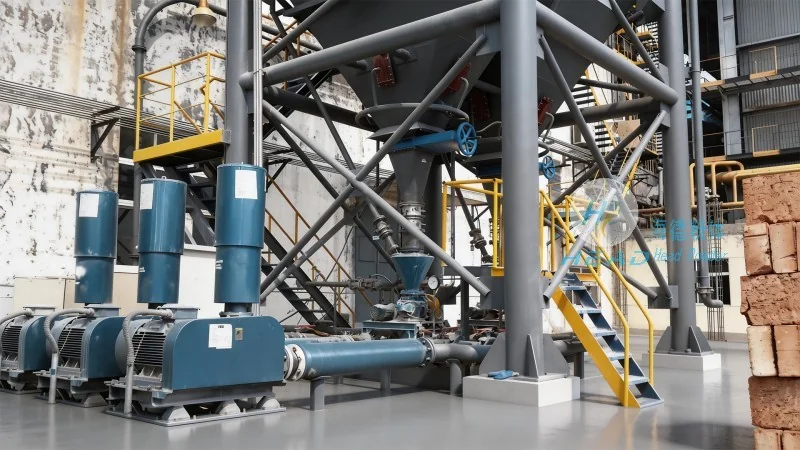
Pneumatic conveying systems utilize air or gas to transport bulk materials like calcium carbonate powder from one location to another. The core principle involves creating a pressure differential that propels the material through a pipeline. There are two primary types of pneumatic conveying: dilute phase and dense phase. Dilute phase systems operate at higher velocities, typically moving material in a suspended state, while dense phase systems use lower velocities and higher pressure to move material in a slurry-like state. For calcium carbonate powder, the choice of system depends on factors such as material properties, distance, and desired flow rate.
The effectiveness of a calcium carbonate powder pneumatic conveying system is determined by its integrated components. These include the material feed hopper, which stores and feeds the powder into the system; the conveyor pipeline, which transports the material; the air compressor or blower, which generates the necessary air pressure; and the control valves and regulators that manage the flow and pressure. Additionally, the system may incorporate dust collection and filtration equipment to ensure compliance with environmental regulations and maintain air quality. Each component is engineered to handle the specific characteristics of calcium carbonate powder, such as its fine particle size and potential for static electricity, to prevent clogging and ensure smooth operation.
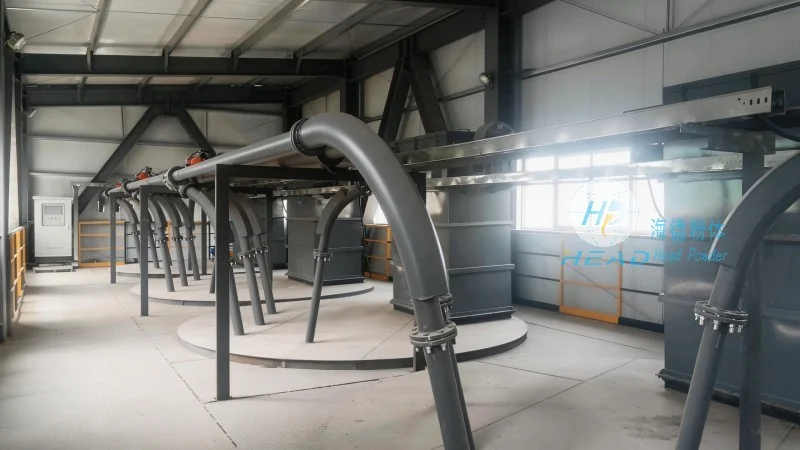
The operational characteristics of calcium carbonate powder pneumatic conveying systems are influenced by the specific industrial environment in which they are deployed. In manufacturing facilities, these systems are often used in continuous production lines for processing and packaging. The systems are designed to integrate seamlessly with existing production workflows, minimizing downtime and maximizing efficiency. For example, in the production of calcium carbonate-based products like coatings or plastics, the conveying system ensures a consistent and reliable supply of raw material to the processing units. The working scene characteristics also include considerations for space constraints, as many industrial facilities have limited room for large equipment. The compact design of modern pneumatic conveying systems allows for installation in confined areas without compromising performance. Furthermore, the systems are built to withstand the abrasive nature of calcium carbonate powder, which can cause wear on components over time. Regular maintenance and the use of wear-resistant materials in critical parts help to extend the system's lifespan and maintain optimal performance.
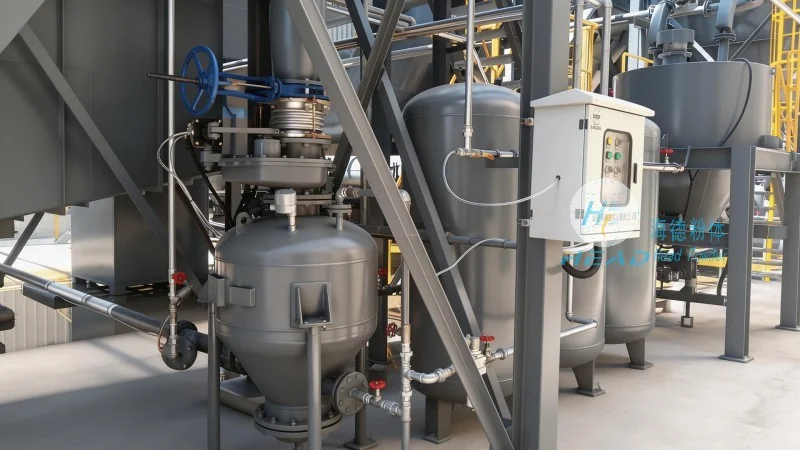
Real-world applications of calcium carbonate powder pneumatic conveying systems demonstrate their versatility and efficiency. In the chemical industry, these systems are used to transport calcium carbonate from storage silos to reaction vessels, ensuring a steady flow of raw material for chemical processes. In the construction materials sector, the systems are employed to move limestone powder for the production of cement and other building materials. The operational efficiency of these systems is measured by factors such as material throughput, system reliability, and energy consumption. Advanced control systems and sensors are integrated into modern pneumatic conveying systems to monitor performance in real-time, allowing for immediate adjustments to maintain optimal operation. This proactive approach to system management helps to reduce downtime and improve overall productivity. The systems are also designed to be energy-efficient, with energy recovery mechanisms that capture and reuse exhaust air, reducing operational costs and environmental impact.
Calcium carbonate powder pneumatic conveying systems represent a sophisticated solution for the efficient handling of fine bulk materials. The principles of pneumatic conveying, combined with specialized components and operational considerations, enable these systems to deliver reliable performance in diverse industrial applications. HeadPowder, with its expertise in engineering and manufacturing, provides tailored solutions that meet the unique needs of clients in the calcium carbonate industry. Based in Shandong, China, HeadPowder leverages its experience to deliver high-quality pneumatic conveying systems that enhance operational efficiency and ensure compliance with industry standards. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the material handling sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top