HeadPowder, a reputable engineering company based in Shandong, China, is dedicated to providing advanced material handling solutions. The company specializes in the design, manufacturing, and installation of negative pressure vacuum material pneumatic conveying equipment, which is widely recognized for its efficiency and reliability in industrial applications. This article delves into the working principle and key features of such equipment, offering insights into how it operates and the benefits it provides to various industries.
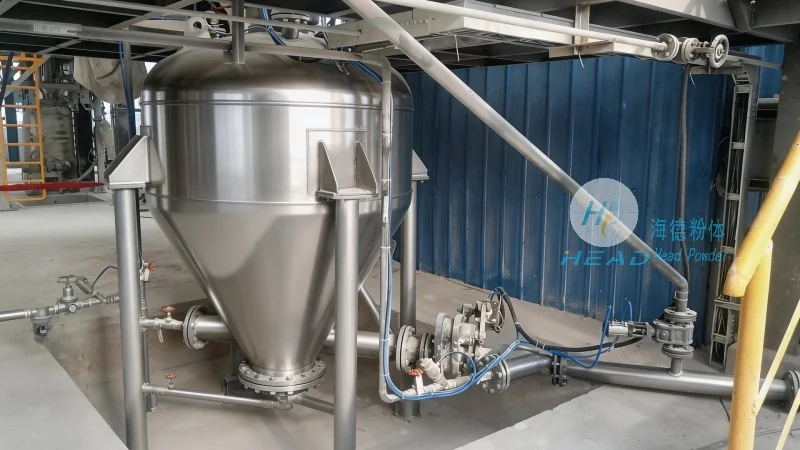
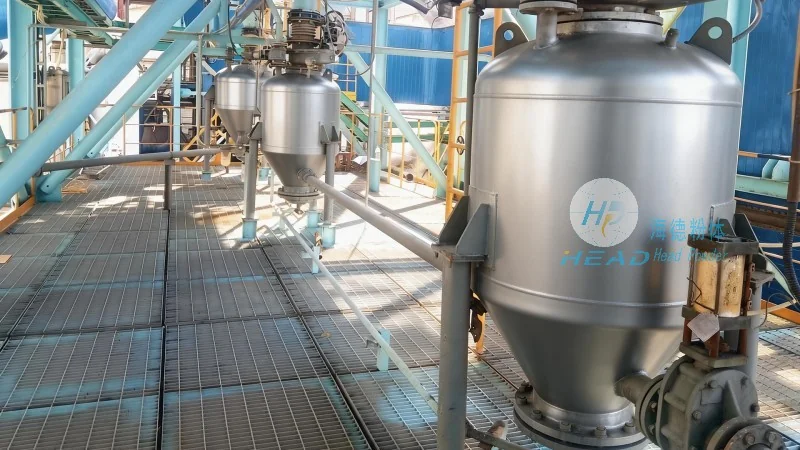
The working principle of negative pressure vacuum material pneumatic conveying systems involves several critical steps. First, the material is fed into the system from a storage hopper or silo. A feeder, often a rotary valve or a screw feeder, controls the flow rate of the material into the conveying line. The vacuum pump, typically a rotary vane or roots blower, is then activated to create a vacuum in the pipeline. This vacuum draws the material particles along with a small amount of air into the pipeline. The material is transported through the pipeline to the receiving hopper or processing unit. At the destination, a filter or cyclone separates the material from the air stream, allowing the material to be discharged and the air to be recirculated or vented. The system operates continuously, maintaining a stable vacuum level to ensure consistent material flow. The key advantage of this principle is the ability to convey materials without the need for positive pressure, which reduces energy consumption and minimizes the risk of dust leakage or material degradation.
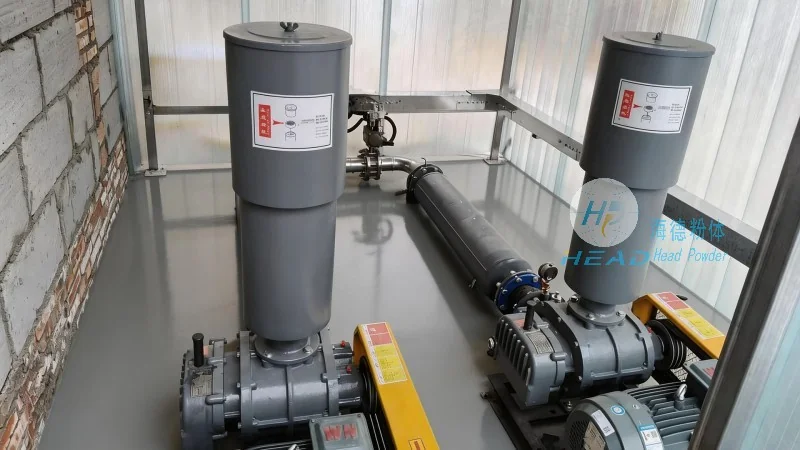
Several key features distinguish negative pressure vacuum material pneumatic conveying equipment from other conveying systems. Firstly, the system operates under negative pressure, which significantly reduces energy consumption compared to positive pressure systems. This makes it more cost-effective for long-term operation. Secondly, the equipment is highly efficient in handling fine and powdery materials, with the ability to transport materials with high moisture content without clogging. The vacuum pump used in these systems is designed for low noise operation, making it suitable for applications in industrial environments where noise control is important. Another important feature is the flexibility in conveying distances, as the system can handle materials over distances of several hundred meters with minimal pressure drop. The equipment also features easy maintenance, with components that can be easily accessed and replaced, reducing downtime. Additionally, the system is designed to be dust-tight, preventing the release of particles into the environment, which is crucial for compliance with environmental regulations.
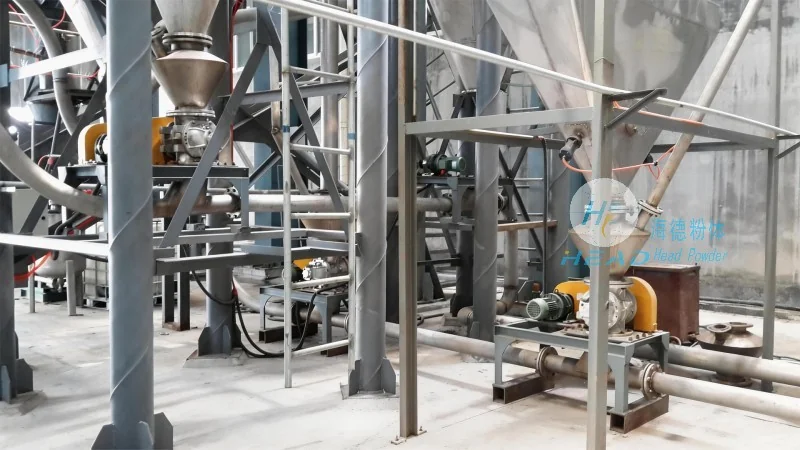
Negative pressure vacuum material pneumatic conveying equipment is widely applied in various industrial sectors due to its versatility and efficiency. In the pharmaceutical industry, the system is used to convey active pharmaceutical ingredients (APIs) and other powders in a sterile and controlled environment, ensuring product purity and compliance with Good Manufacturing Practices (GMP). The food processing industry utilizes the equipment to transport ingredients such as flour, sugar, and spices, maintaining product quality and preventing contamination. In the chemical industry, the system handles corrosive and hazardous materials safely, with the ability to control the flow and prevent leaks. The mining and mineral processing sector benefits from the system's ability to transport bulk materials such as coal, ore, and sand over long distances with minimal environmental impact. The overall advantages of the equipment include high efficiency, low maintenance costs, and compliance with safety and environmental standards. These features make it an ideal choice for industries that require reliable and sustainable material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top