Glucose powder pneumatic conveying technology represents a sophisticated method for transporting bulk materials like glucose powder through a pipeline using air or other gas as the conveying medium. This technology has become increasingly vital in industries where handling fine powders efficiently and safely is critical. The following sections will delve into the fundamental principles of this technology, its practical applications, and the evolving trends that shape its future development.
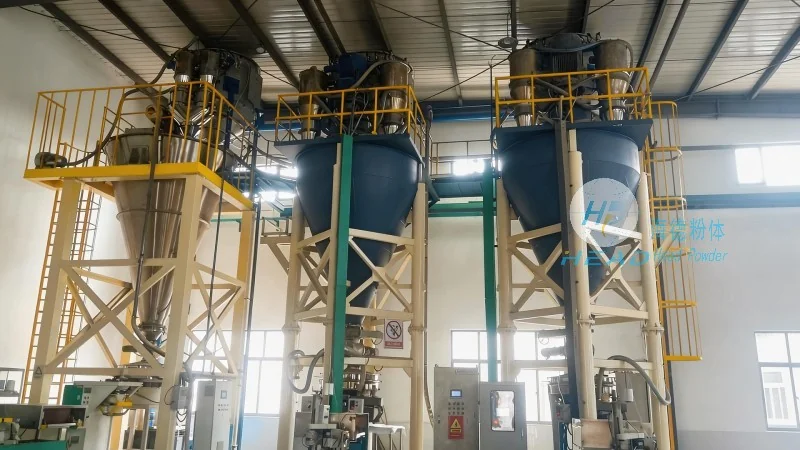
The core principle of pneumatic conveying involves the use of pressure differentials to move solid particles through a pipeline. In the case of glucose powder, which is a fine, hygroscopic material, the conveying system must be designed to maintain material integrity while ensuring efficient transport. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure. Positive pressure systems operate by blowing air into the pipeline, pushing the material forward, while negative pressure systems draw material into the pipeline using a vacuum. For glucose powder, positive pressure systems are often preferred due to their ability to handle abrasive materials and prevent product degradation. The system typically consists of a hopper, a conveyor line, and a receiver. The hopper stores the glucose powder, and a rotary valve or feeder controls the material flow into the conveyor line. The conveying air is introduced at the inlet, creating a flow that carries the powder particles through the pipeline to the receiver, where the material is deposited.
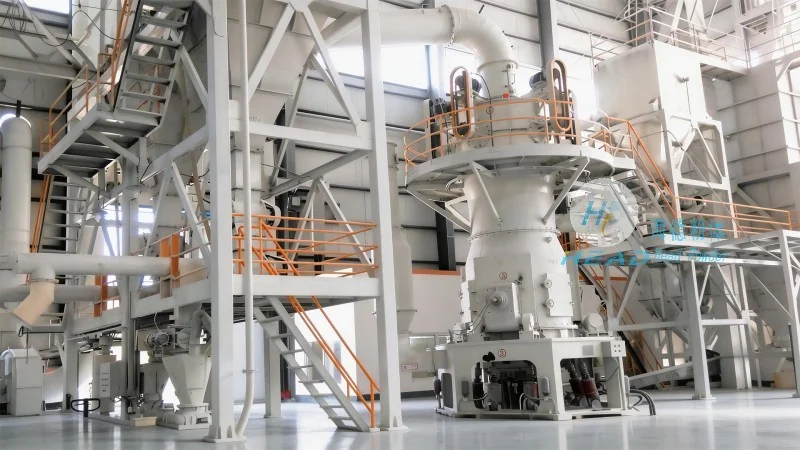
Glucose powder pneumatic conveying technology finds extensive application in the food and pharmaceutical industries, where the purity and consistency of the product are paramount. In food processing, glucose powder is used as a sweetener and energy source in various products, including beverages, baked goods, and dairy products. The pneumatic conveying system ensures that the powder is transported without contamination or agglomeration, maintaining its quality. For instance, in a glucose production facility, the powder is conveyed from storage silos to mixing tanks or packaging lines. The system's ability to handle fine powders without clogging or particle breakage is crucial for maintaining product quality. In the pharmaceutical sector, glucose powder is used as an excipient or active ingredient in drug formulations. The sterile and hygienic design of the conveying system is essential to prevent contamination, making it suitable for GMP (Good Manufacturing Practice) compliance. The technology also enables precise dosing and control over the powder flow, which is critical for pharmaceutical applications where accuracy is non-negotiable.
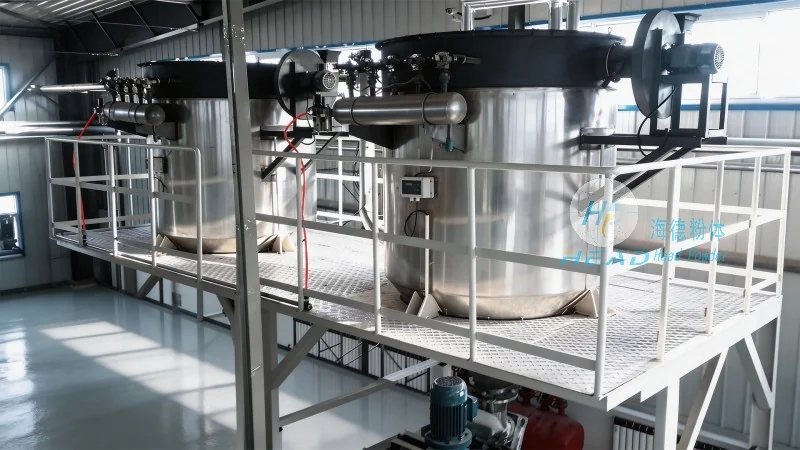
Several key features make glucose powder pneumatic conveying technology a preferred choice for material handling. Firstly, it offers a closed system, which prevents dust contamination and environmental pollution. This is particularly important for glucose powder, which can be hygroscopic and prone to moisture absorption. The closed system also maintains product purity, ensuring that the powder remains free from external contaminants. Secondly, the technology provides high efficiency and flexibility in material transport. It can handle varying particle sizes and flow rates, adapting to different production needs. The system's ability to transport materials over long distances without the need for intermediate storage or manual handling reduces labor costs and improves operational efficiency. Additionally, pneumatic conveying systems are relatively compact and can be integrated into existing production lines, minimizing space requirements. The low maintenance requirements of these systems further contribute to their cost-effectiveness, as they have fewer moving parts compared to mechanical conveyors. For glucose powder, which is a fine and potentially abrasive material, the system's durability and resistance to wear are critical factors that enhance its longevity and performance.
The field of glucose powder pneumatic conveying technology is continuously evolving, driven by advancements in automation, material science, and environmental regulations. One of the prominent trends is the integration of automation and control systems. Modern conveying systems now incorporate advanced sensors and control algorithms that monitor flow rates, pressure, and particle size in real-time. This enables precise control over the conveying process, reducing waste and improving product consistency. The use of IoT (Internet of Things) technology allows for remote monitoring and predictive maintenance, further enhancing operational efficiency. Another trend is the focus on sustainability and energy efficiency. Manufacturers are developing more energy-efficient blowers and optimizing air usage to reduce operational costs and environmental impact. The adoption of eco-friendly materials and processes, such as using less energy-intensive conveying methods, aligns with global sustainability goals. Furthermore, the development of hybrid systems that combine pneumatic conveying with other technologies, such as vacuum-assisted conveying, is gaining traction. These hybrid systems offer improved performance and flexibility, catering to diverse production requirements. The future of glucose powder pneumatic conveying technology also involves the use of advanced materials and coatings to enhance system durability and resistance to corrosion. As the demand for high-quality glucose powder continues to grow, the technology will likely see further innovations aimed at improving efficiency, safety, and sustainability.
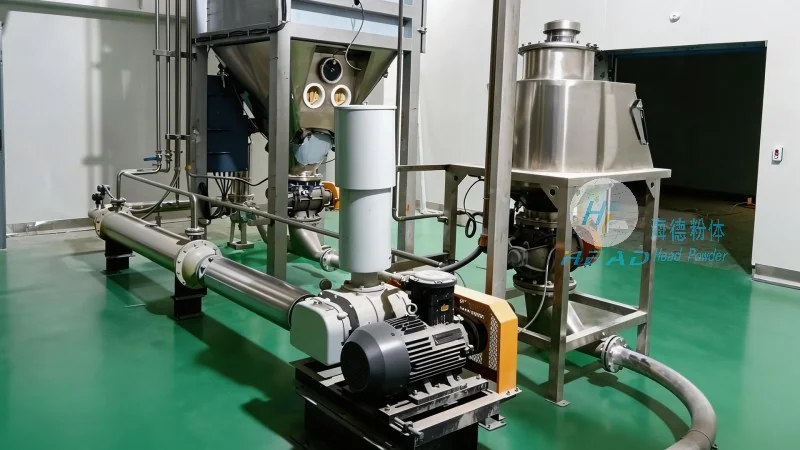
Glucose powder pneumatic conveying technology plays a pivotal role in the efficient and safe handling of glucose powder in various industries. Its ability to maintain product quality, ensure environmental safety, and enhance operational efficiency makes it an indispensable part of modern production processes. As the technology continues to evolve, it will likely integrate more advanced automation and sustainable practices, further solidifying its position in the market. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of glucose powder applications. With a focus on innovation and quality, the company ensures that its solutions meet the highest industry standards, providing reliable and efficient material handling solutions for its clients. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its expertise and experience to deliver cutting-edge pneumatic conveying technologies that support the growth and success of its clients in the glucose powder industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top