Working Principle and Features of Bulk Material Pneumatic Conveying Equipment for Grain Storage
Release time:2026-09-18 05:01:28
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
For businesses in the agricultural and food processing sectors, efficient and reliable material handling is crucial for maintaining productivity and ensuring product quality. This article focuses on the working principle and key features of bulk material pneumatic conveying equipment designed specifically for grain storage applications, provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
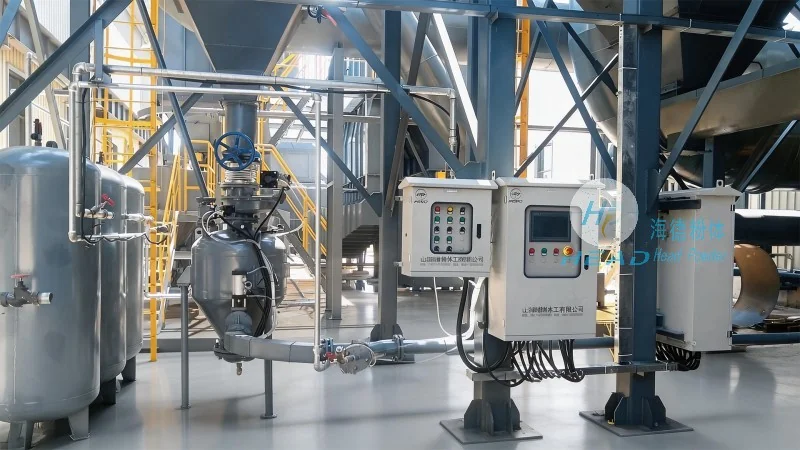
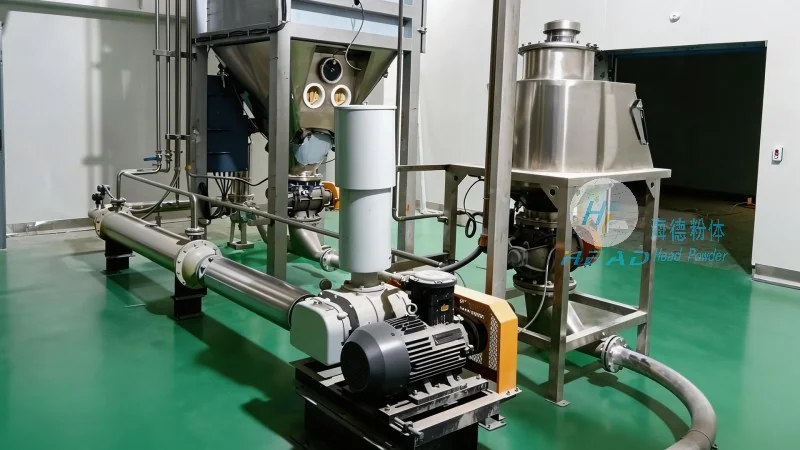
Working Principle of Grain Storage Pneumatic Conveying Equipment
The core function of a grain storage pneumatic conveying system is to transport bulk materials, such as grains, powders, or other dry particulate materials, from a storage silo or hopper to processing equipment or storage containers. The system operates by using compressed air or gas to create a flow of material through a pipeline network. The process typically involves several key components and steps:
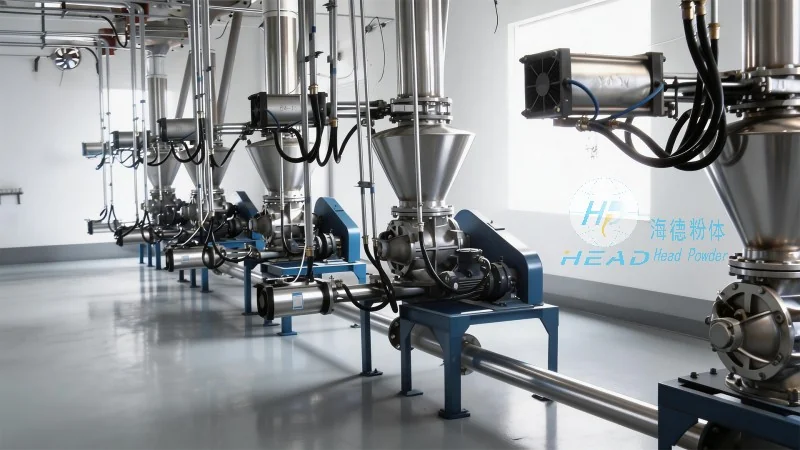
- Material Loading: The bulk material is fed into the conveying system from the storage silo or hopper. A feeder, such as a rotary valve or a screw feeder, controls the flow rate of the material into the system.
- Air Supply: Compressed air is supplied to the system, creating a pressure differential that propels the material through the pipeline. The air velocity is carefully controlled to ensure the material is suspended and transported efficiently without causing excessive wear or degradation.
- Pipeline Transport: The material and air mixture travels through the conveying pipeline. The design of the pipeline, including bends, elbows, and expansion joints, is optimized to minimize pressure loss and maintain consistent flow.
- Discharge and Separation: At the receiving end, the material is separated from the air using a cyclone separator or a filter. The separated material is then discharged into the target container or processing equipment, while the air is typically filtered and recycled back into the system.
Key Features of Grain Storage Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. offers a range of pneumatic conveying solutions tailored to the unique demands of grain storage operations. The equipment is designed with several key features that enhance performance, reliability, and user experience:
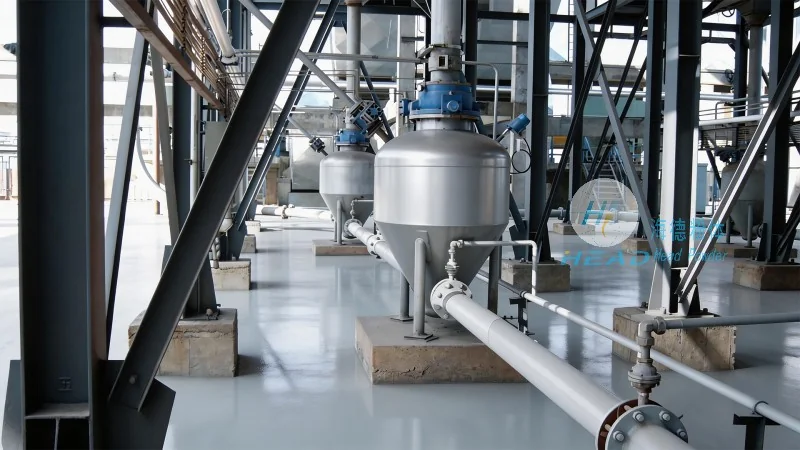
- High Efficiency and Low Energy Consumption: The system is engineered to maximize material throughput while minimizing energy usage. Advanced air control mechanisms and optimized pipeline designs help reduce operational costs and environmental impact.
- Low Maintenance and Durable Construction: The equipment is built with high-quality materials, such as stainless steel and corrosion-resistant components, to withstand the harsh conditions of grain handling. This results in lower maintenance requirements and longer service life.
- Customizable and Scalable Solutions: HeadPowder provides tailored solutions to meet the specific needs of different grain storage facilities. Whether for small-scale operations or large industrial plants, the equipment can be scaled to accommodate varying material volumes and processing requirements.
- Safe and Clean Operation: The pneumatic conveying system operates in a closed environment, preventing dust emissions and ensuring a clean working environment. This is particularly important for maintaining food safety standards and complying with environmental regulations.
- Advanced Control Systems: Modern control systems allow for precise monitoring and adjustment of the conveying process. Operators can easily adjust flow rates, air pressure, and other parameters to optimize performance and prevent system failures.
Benefits of Using Pneumatic Conveying for Grain Storage
Implementing a pneumatic conveying system for grain storage offers numerous benefits that contribute to improved operational efficiency and product quality. By automating the material handling process, businesses can reduce labor costs, minimize material loss, and enhance overall productivity. The closed system design also helps maintain product integrity, preventing contamination and degradation during transport. Additionally, the ability to control the conveying process remotely allows for better management of inventory and processing schedules.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
