Low-pressure continuous powder pneumatic conveying systems are advanced industrial equipment designed to transport bulk powders efficiently and reliably. This technology is widely used in various industries, including food, pharmaceuticals, chemicals, and minerals, where the handling of fine powders requires precise control and minimal product degradation. The system operates on the principle of using air as the conveying medium to move powders through a pipeline network. By maintaining a low-pressure environment, these systems ensure safe and effective material transport without the need for high-pressure components, which can be more complex and costly.
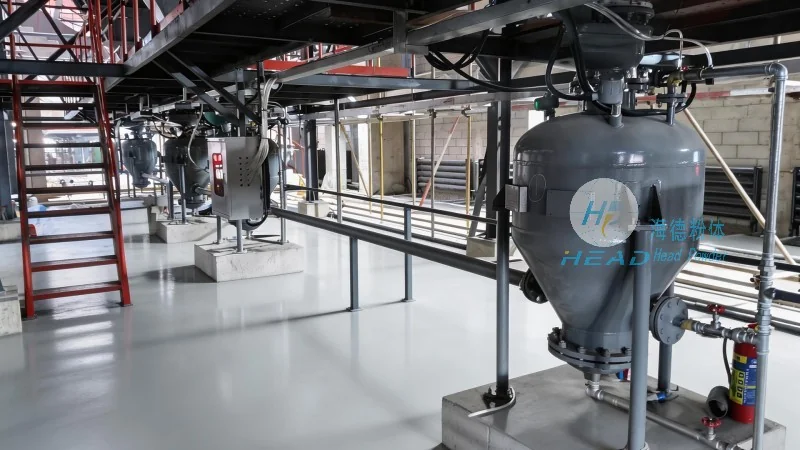
The core working principle of low-pressure continuous powder pneumatic conveying systems involves the creation of a controlled airflow within a closed pipeline system. The system typically consists of a feeding hopper, a rotary airlock valve, a conveying pipeline, and a receiving hopper. The process begins with the powder being fed into the hopper, where it is then metered into the pipeline by the rotary airlock valve. Compressed air, supplied at a relatively low pressure (usually between 0.5 to 2 bar), is introduced into the pipeline, creating a flow that entrains the powder particles. The air-powder mixture travels through the pipeline to the receiving hopper, where the air is separated from the powder, often using a cyclone separator or a filter. The separated air is then discharged back into the system or to the atmosphere, while the powder is collected in the receiving hopper. This continuous operation allows for a steady flow of material, making it suitable for long-distance and high-volume transport applications.
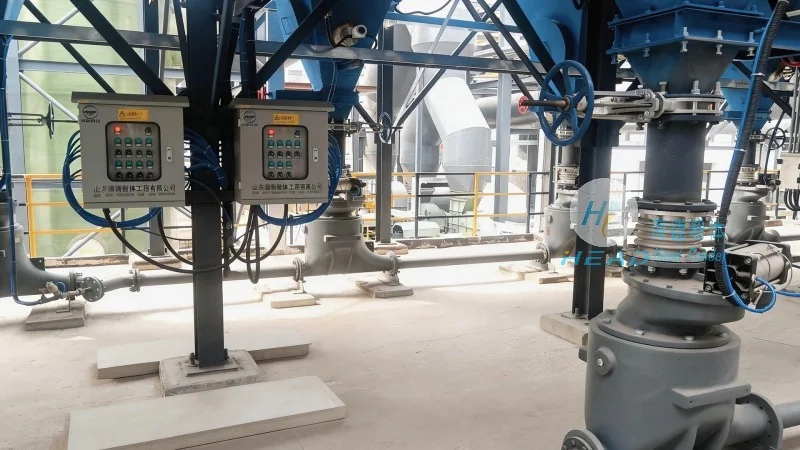
Low-pressure continuous powder pneumatic conveying systems offer several distinct advantages that make them a preferred choice for many industrial applications. Firstly, they provide a clean and dust-free operation, as the entire system is enclosed, preventing dust from being released into the environment. This is particularly important in industries where product purity and environmental compliance are critical, such as pharmaceuticals and food processing. Secondly, these systems are highly flexible in terms of layout and can be easily adapted to different plant configurations. The modular design allows for the addition or removal of conveying sections without major modifications to the overall system. Thirdly, low-pressure operation reduces energy consumption compared to high-pressure systems, leading to lower operational costs over time. Additionally, the continuous feeding mechanism ensures a consistent flow rate, which helps maintain process stability and reduces the risk of material buildup or clogging in the pipeline. The system also minimizes product degradation due to the gentle handling of powders, as the air-powder mixture moves at controlled velocities, preventing excessive friction or impact that could damage the material.
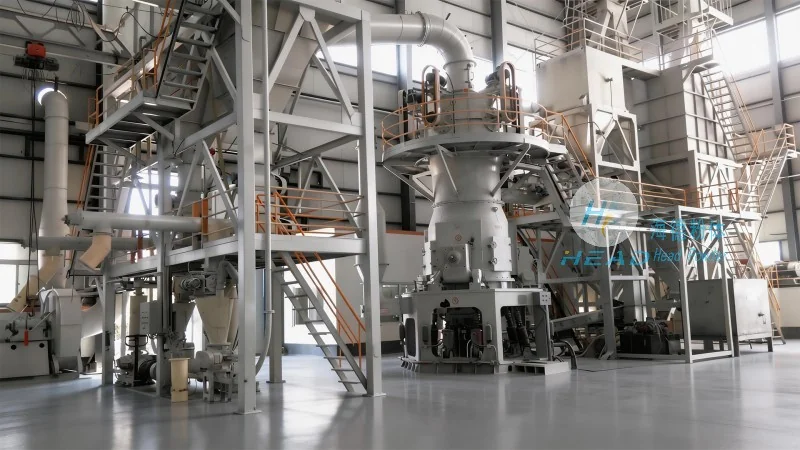
The versatility of low-pressure continuous powder pneumatic conveying systems makes them suitable for a wide range of applications. In the food industry, they are used to transport ingredients like flour, sugar, and spices, ensuring that the products remain fresh and free from contamination. In the pharmaceutical sector, these systems are employed to handle active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict quality control standards. The chemical industry utilizes them for transporting powders such as pigments, catalysts, and other chemicals, where precise dosing and purity are essential. In the minerals and mining sector, low-pressure systems are used to convey raw materials like coal, limestone, and ore, facilitating efficient processing and transportation. The benefits of these systems extend beyond just material transport; they also contribute to improved workplace safety by eliminating manual handling of powders and reducing the risk of dust explosions. The enclosed design and controlled airflow help prevent dust accumulation, which is a significant fire hazard in many industrial environments.
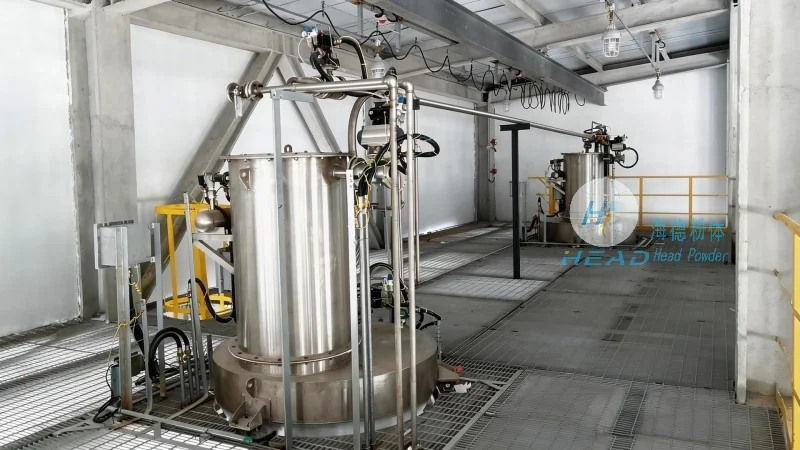
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling equipment. With a strong focus on innovation and quality, the company specializes in designing and manufacturing low-pressure continuous powder pneumatic conveying systems tailored to meet the specific needs of various industries. HeadPowder's team of engineers and technicians leverages years of experience and cutting-edge technology to develop solutions that enhance efficiency, safety, and product quality. The company's commitment to customer satisfaction is evident in its comprehensive after-sales support, including installation, maintenance, and technical assistance. HeadPowder's facilities are located in Shandong, China, where the company operates a state-of-the-art manufacturing plant equipped with advanced machinery and quality control systems. This ensures that every product meets the highest standards of performance and reliability. By partnering with HeadPowder, industries can benefit from reliable and efficient powder handling solutions that contribute to improved operational performance and reduced costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top