Clay ash powder pneumatic conveying systems are critical equipment in industrial processes, especially for transporting fine powders such as clay ash. These systems utilize air as the medium to move material from one location to another, offering a dust-free and efficient alternative to traditional mechanical conveying methods. Understanding the working principle and key features of these systems is essential for selecting the right equipment for specific industrial applications.
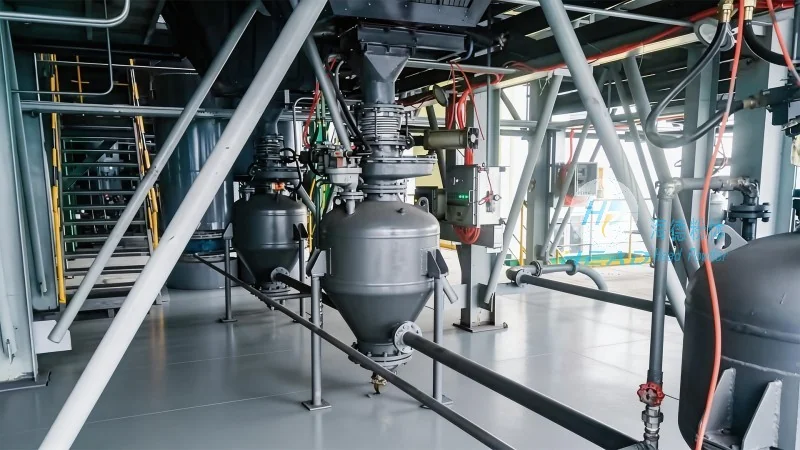
The fundamental operation of a clay ash powder pneumatic conveying system involves using compressed air to create a flow that transports the powder. The process begins with the material being fed into a hopper or storage silo. From there, the powder is drawn into a pipeline by the pressure difference generated by the air flow. Systems can operate under either positive pressure (where air is forced through the system) or negative pressure (where air is drawn out, creating a vacuum). In positive pressure systems, a blower or compressor supplies air to push the powder through the pipeline, while negative pressure systems use a vacuum pump to pull the material. The air velocity is carefully controlled to ensure powder particles are fully entrained and transported without clogging or degradation. Key components include the hopper, feeder, pipeline, and receiving tank, each playing a vital role in the overall operation. The system's efficiency depends on maintaining consistent air pressure and flow rates to prevent material separation or blockages.
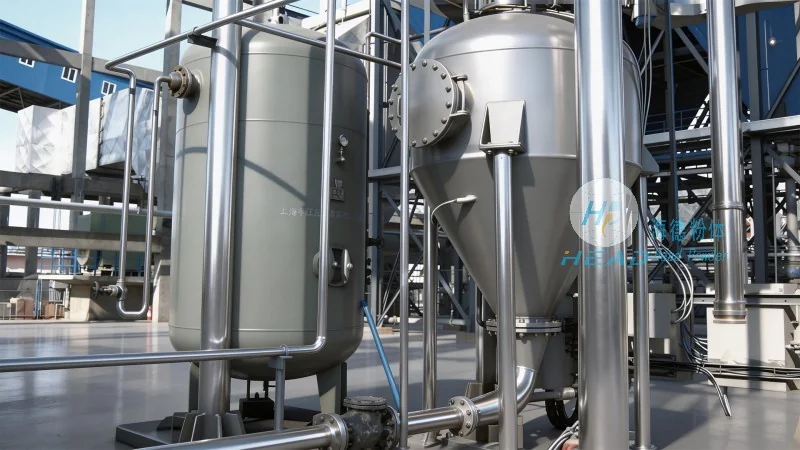
Clay ash powder pneumatic conveying systems offer several advantages that make them suitable for industrial use. One primary feature is their ability to handle fine and abrasive powders like clay ash without causing equipment wear or damage. The enclosed pipeline system minimizes dust emissions, contributing to a cleaner working environment and compliance with environmental regulations. Another significant feature is the flexibility in system design, allowing for horizontal, vertical, or mixed configurations to suit different plant layouts and material handling needs. These systems are also capable of transporting materials over long distances with minimal energy consumption compared to other conveying methods. Additionally, they can be integrated with other processing equipment, such as mixers or classifiers, to form a complete production line. The control systems are often equipped with sensors and automation to monitor flow rates, pressure, and material levels, ensuring smooth and reliable operation. Maintenance is generally straightforward, with components designed for easy access and replacement, reducing downtime and operational costs.
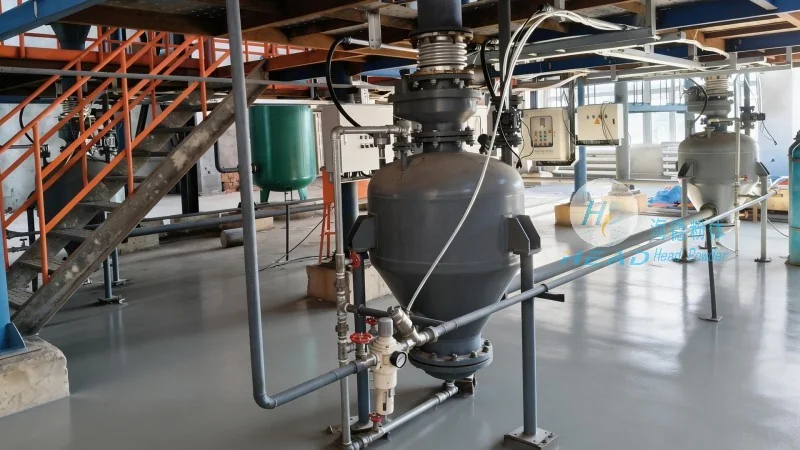
Clay ash powder pneumatic conveying systems are widely used in industries that process and handle fine powders, including cement, construction materials, and chemical manufacturing. In the cement industry, they are used to transport raw materials and finished products, improving production efficiency and reducing labor costs. The construction materials sector benefits from the ability to handle clay ash, a byproduct often used in concrete production, ensuring consistent quality and reduced waste. Chemical manufacturers find these systems useful for transporting various powders, enhancing safety by preventing dust explosions and improving product purity. The benefits extend to environmental sustainability, as the enclosed system reduces dust pollution and helps meet emission standards. For companies like Shandong HeadPowder Engineering Co., Ltd., based in China, these systems represent a reliable solution for efficient material handling, combining advanced technology with practical design to meet the demands of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top