Denitration ash powder conveyors play a crucial role in the industrial sector, particularly in facilities that employ selective catalytic reduction (SCR) systems for nitrogen oxide (NOx) removal. These systems generate large volumes of ash powder as a byproduct, which must be efficiently and safely transported for disposal or further processing. The working principle and features of such conveyors are essential for optimizing operational efficiency and ensuring environmental compliance.
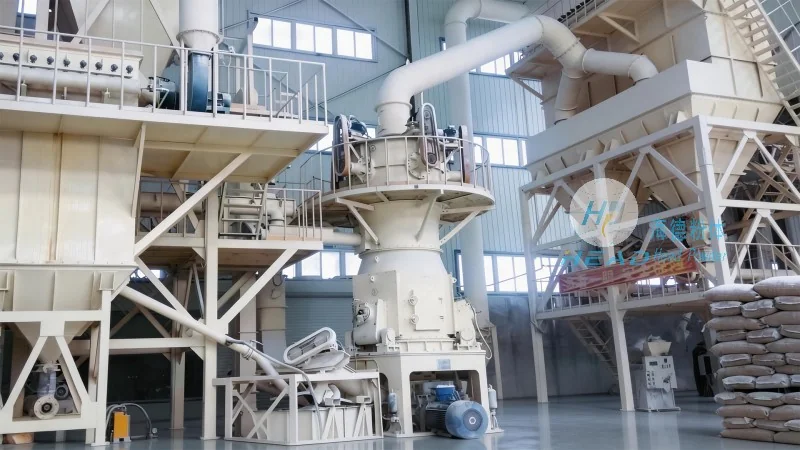
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. With a strong focus on innovation and customer-centric solutions, HeadPowder has developed denitration ash powder conveyors that meet the demanding requirements of modern industrial applications. The company's commitment to quality and reliability has established it as a trusted partner for clients seeking efficient and reliable ash handling solutions.
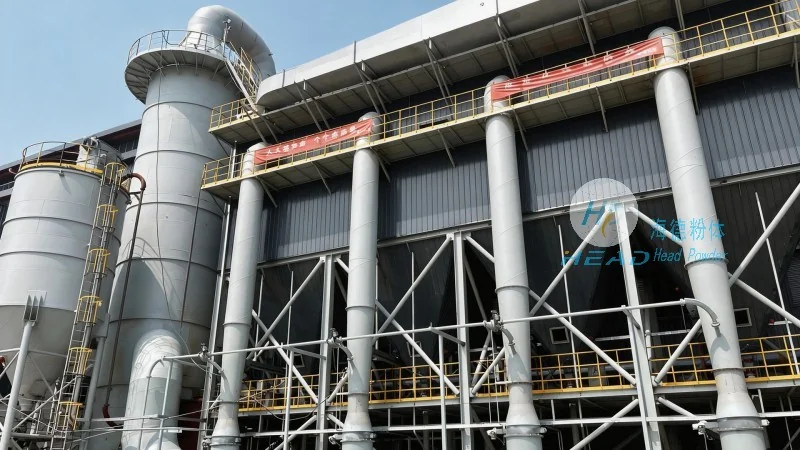
Denitration ash powder conveyors typically operate on the principle of pneumatic or mechanical transport, depending on the specific design and application requirements. For high-volume, low-density ash powders, pneumatic conveying systems are commonly used. These systems utilize a combination of air flow and pressure to move the ash particles through a network of pipes. The process begins with the ash being fed into a hopper or feeder, where it is then introduced into the conveying line. A blower or compressor generates the necessary airflow, which propels the ash particles through the pipeline. The ash is carried as a suspension of particles in the air stream, ensuring a continuous and uniform flow. The system includes components such as a dust collector, filter, and control valves to manage the air flow and prevent dust emissions. Mechanical conveyors, on the other hand, may use screw conveyors or belt conveyors to transport the ash, particularly for applications where the ash has higher moisture content or larger particle sizes. These systems rely on mechanical force to move the material, often with the aid of gravity or motor-driven mechanisms.
Denitration ash powder conveyors from Shandong HeadPowder Engineering Co., Ltd. are characterized by several key features that enhance their performance and reliability. Firstly, these conveyors are designed with robust construction to withstand the harsh conditions associated with ash handling, including high temperatures, abrasive particles, and corrosive environments. The materials used in the construction, such as stainless steel or high-grade alloys, ensure durability and long service life. Secondly, the conveyors feature excellent sealing and dust-proofing capabilities, minimizing the risk of air leakage and dust emissions. This is critical for maintaining environmental compliance and ensuring workplace safety. Thirdly, the systems are equipped with advanced control systems that allow for precise regulation of the conveying rate, pressure, and flow. This enables operators to adjust the system parameters in real-time, optimizing performance and reducing energy consumption. Additionally, the conveyors are designed for easy maintenance and cleaning, with accessible components and minimal downtime. The use of high-efficiency motors and energy-saving technologies further reduces operational costs and environmental impact.
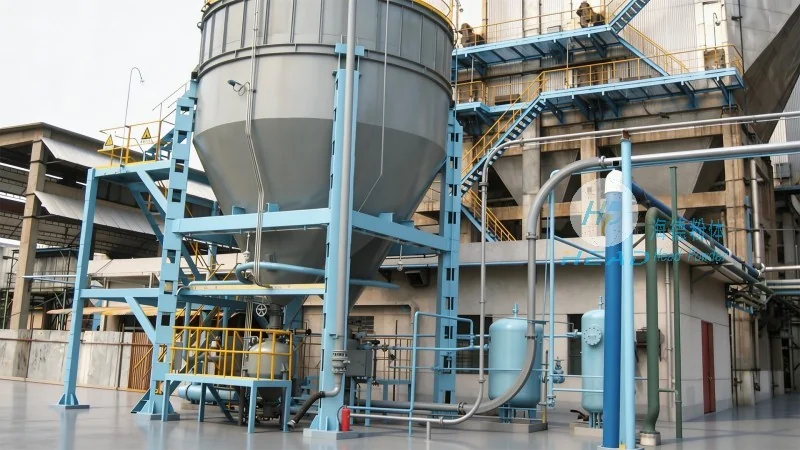
The denitration ash powder conveyors manufactured by Shandong HeadPowder Engineering Co., Ltd. are widely used in various industrial applications, including power plants, industrial boilers, and chemical processing facilities. In power plants, these conveyors are essential for transporting the ash generated from SCR systems to storage or disposal sites. The efficient handling of ash reduces the risk of blockages and ensures the smooth operation of the entire system. In industrial boilers, the conveyors help maintain consistent ash removal rates, preventing the buildup of ash that could lead to equipment failure. The benefits of using these conveyors include improved operational efficiency, reduced downtime, lower maintenance costs, and enhanced environmental performance. By effectively managing the ash output from denitration processes, these conveyors contribute to the overall sustainability and profitability of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top