When it comes to the efficient handling of bulk powders, especially in the fertilizer industry, sulfate ammonium is a key product that requires reliable and effective transportation methods. Traditional methods like belt conveyors or manual handling often fall short in terms of speed, safety, and environmental impact. This is where pneumatic conveying technology steps in, offering a solution that leverages air flow to move powder materials with precision and efficiency. For businesses dealing with sulfate ammonium, understanding the nuances of pneumatic conveying is crucial for optimizing operations and ensuring product integrity.
Pneumatic conveying, also known as air conveying, is a method that uses pressurized or suction air to transport dry bulk materials through a pipeline system. Unlike mechanical conveyors, which rely on moving parts and physical contact, pneumatic systems operate by suspending particles in a stream of air, allowing them to be moved over long distances without the need for frequent maintenance or material degradation. This technology is particularly well-suited for sulfate ammonium due to its fine particle size and sensitivity to moisture, as it minimizes exposure to external elements and prevents caking or agglomeration.
Implementing pneumatic conveying for sulfate ammonium offers several distinct advantages that can significantly impact operational efficiency and cost-effectiveness. First, it provides a high degree of flexibility in material handling, allowing for the transport of powders from multiple sources to various destinations within a facility or across different sites. This flexibility is essential for complex production lines where materials need to be routed to different processing stages or storage areas. Second, pneumatic systems are highly efficient in terms of energy consumption compared to traditional mechanical conveyors, as they use compressed air to move materials without the friction and wear associated with moving parts. This translates to lower operational costs and reduced maintenance requirements over time.
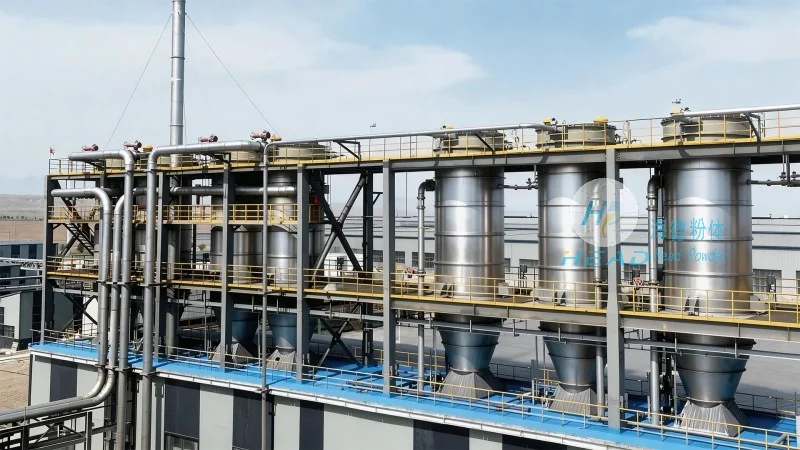
Another critical advantage is the enhanced safety and hygiene that pneumatic conveying provides. By eliminating the need for manual handling or open-air transport, these systems reduce the risk of dust exposure and contamination, which is vital for maintaining product quality and complying with health and safety regulations. Additionally, pneumatic systems can be designed to operate in a closed-loop environment, further minimizing the environmental impact and preventing dust emissions into the atmosphere. This is especially important for sulfate ammonium, which, if not handled properly, can contribute to air pollution and health hazards.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of customized pneumatic conveying solutions tailored to the specific needs of industries dealing with sulfate ammonium and other bulk powders. With headquarters in Shandong, China, HeadPowder has established itself as a trusted name in the field, offering a range of services from system design and installation to maintenance and technical support. The company specializes in developing efficient, reliable, and cost-effective pneumatic conveying systems that meet the unique challenges of handling fine, moisture-sensitive powders like sulfate ammonium.
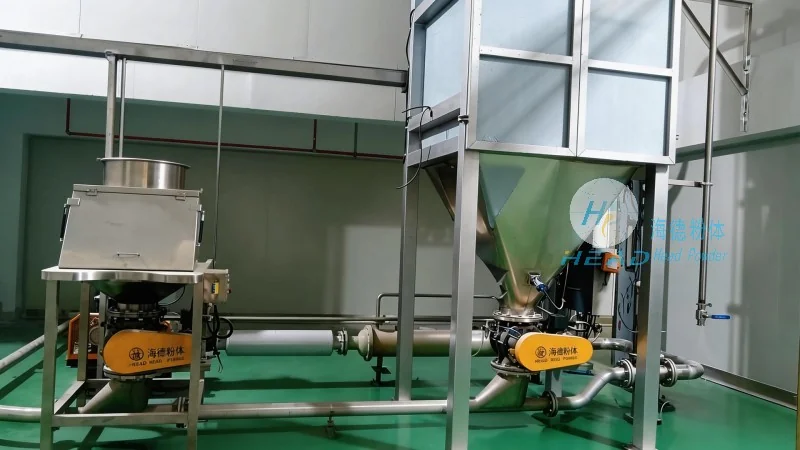
HeadPowder's approach to pneumatic conveying is centered on understanding the specific requirements of each client. By conducting thorough assessments of material properties, production volumes, and operational constraints, the company designs systems that optimize performance while minimizing downtime and maintenance costs. This customer-centric approach has earned HeadPowder a reputation for delivering high-quality solutions that enhance operational efficiency and product integrity. Whether it's a new installation or an upgrade to an existing system, HeadPowder provides comprehensive support to ensure that clients achieve their material handling goals.
At HeadPowder, we recognize that every sulfate ammonium handling operation is unique, and a one-size-fits-all approach is rarely effective. Therefore, our team of experts works closely with clients to develop customized pneumatic conveying solutions that address their specific challenges. This includes selecting the appropriate type of conveying system—such as pressure or vacuum systems—based on the distance, volume, and material characteristics. For sulfate ammonium, which often requires gentle handling to prevent particle degradation, our systems are designed with low-pressure, low-velocity air flow to minimize impact and ensure product quality.
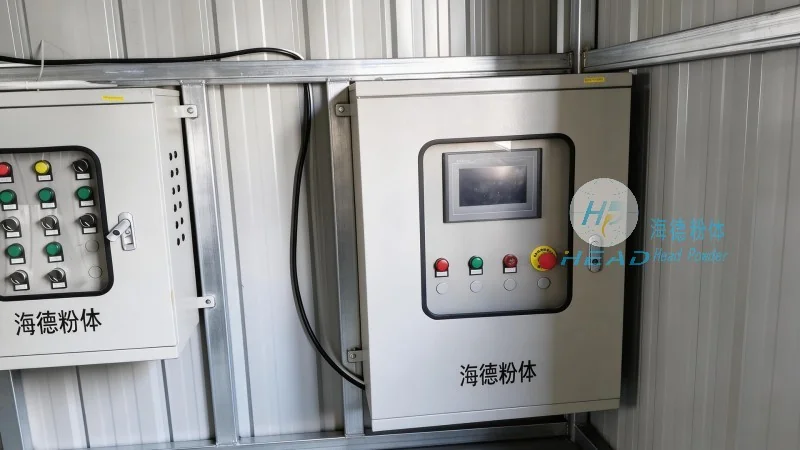
Our customized solutions also incorporate advanced control systems that allow for real-time monitoring and adjustment of conveying parameters. This ensures that the system operates at peak efficiency, reducing energy consumption and minimizing the risk of material blockages or system failures. Additionally, HeadPowder offers maintenance and service packages to keep systems running smoothly, with regular inspections and preventive maintenance to extend the lifespan of equipment and reduce unexpected downtime.
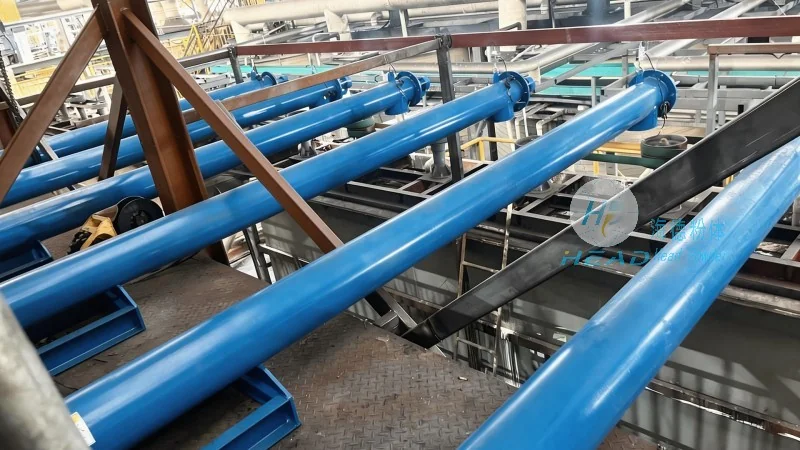
For sulfate ammonium, maintaining product integrity is paramount. Pneumatic conveying systems from HeadPowder are designed with this in mind, using materials that are resistant to corrosion and compatible with the chemical properties of sulfate ammonium. The closed-loop design of these systems prevents cross-contamination and ensures that the powder remains free from moisture and other contaminants, which is critical for meeting quality standards and regulatory requirements. HeadPowder adheres to industry best practices and complies with relevant safety and environmental regulations, providing clients with peace of mind that their operations are both efficient and compliant.
By leveraging the expertise of HeadPowder, businesses can enhance their sulfate ammonium handling processes, improve operational efficiency, and reduce costs. Our customized pneumatic conveying solutions are tailored to meet the specific needs of each client, ensuring that materials are transported safely, efficiently, and with minimal impact on the environment. Whether you are a fertilizer manufacturer, a chemical processor, or a bulk material handler, HeadPowder offers the technology and support needed to optimize your sulfate ammonium operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top