The efficient and reliable transportation of pearl salt granules is a critical aspect of modern industrial operations. Pneumatic conveying technology offers a solution that minimizes material handling issues while ensuring product integrity. This article delves into the nuances of vacuum and positive pressure pneumatic conveying systems, exploring their applications and benefits for handling pearl salt granules.
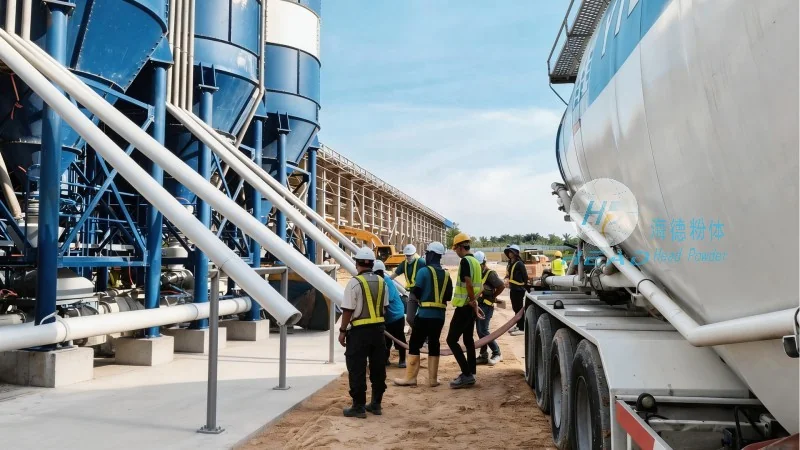
HeadPowder, a leading provider in the field, specializes in engineering solutions tailored to the unique requirements of bulk material handling. With a focus on innovation and precision, the company has developed advanced systems that optimize the performance of pneumatic conveying for pearl salt granules.
Vacuum pneumatic conveying systems operate by creating a negative pressure environment at the material intake point. This draws the pearl salt granules into the conveying line using air as the medium. The system typically consists of a vacuum pump, a hopper, and a conveying line, with the material being transported from a source to a destination under reduced pressure.
For pearl salt granules, vacuum systems are particularly effective when dealing with fine or dusty materials, as they can handle particles with a wide range of sizes and moisture content. The gentle handling of the granules minimizes breakage and ensures that the product remains in its original state. This makes vacuum conveying ideal for applications where product quality is paramount, such as in food processing or pharmaceutical industries.
In contrast, positive pressure systems generate a positive pressure at the material discharge point, pushing the air and material through the conveying line. These systems are often more suitable for longer distances or when the material needs to be transported against gravity. The equipment includes a blower, a hopper, and a conveying line, with the material being forced from the source to the destination under increased pressure.
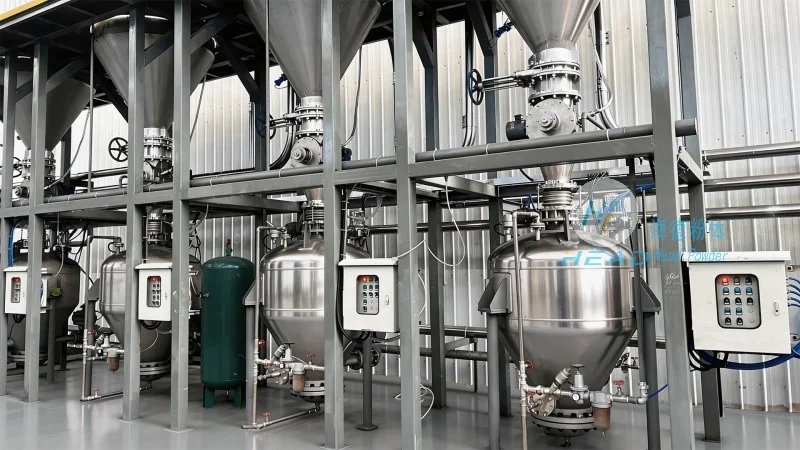
Positive pressure systems are commonly used in industrial settings where bulk material handling is required, such as in mining, construction, or chemical processing. For pearl salt granules, these systems can handle larger quantities and higher flow rates, making them efficient for large-scale operations. The robust design of positive pressure systems ensures durability and reliability, even in harsh environments.
When selecting between vacuum and positive pressure pneumatic conveying for pearl salt granules, several factors must be considered. The distance between the source and destination, the volume of material to be transported, and the required product quality all influence the choice of system. Vacuum systems are generally preferred for shorter distances and when product integrity is critical, while positive pressure systems are better suited for longer distances and higher throughput.
HeadPowder's expertise lies in designing customized pneumatic conveying solutions that address these specific needs. By analyzing the characteristics of the pearl salt granules, such as particle size, density, and moisture content, the company can recommend the most appropriate system configuration. This includes selecting the right type of air pump, determining the optimal conveying line diameter, and ensuring proper filtration to maintain air quality.
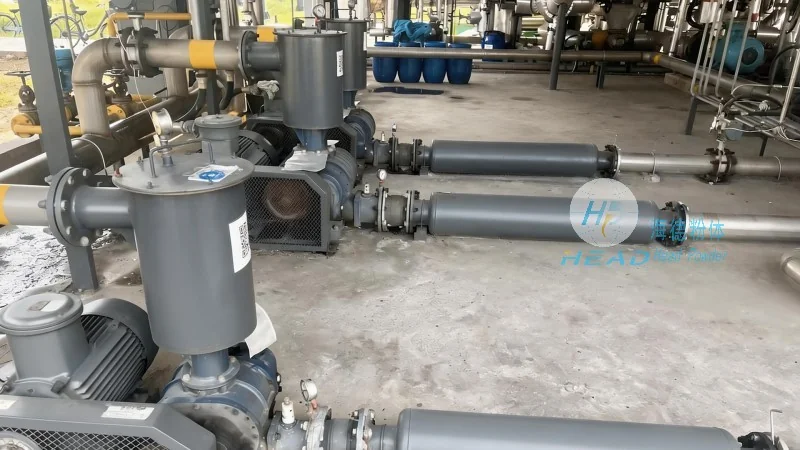
The effectiveness of pneumatic conveying systems for pearl salt granules is demonstrated through various case studies. In one application, a food processing plant implemented a vacuum system to transport fine pearl salt granules from a storage silo to a mixing area. The system successfully minimized product contamination and reduced labor costs by automating the material handling process. The gentle handling of the granules ensured that the product remained free-flowing and free from clumping, which is essential for consistent product quality.
Another example involves a chemical processing facility that used a positive pressure system to transport larger pearl salt granules over a distance of 500 meters. The system's high throughput and reliability allowed the plant to increase production capacity without compromising on material quality. The positive pressure design also provided better control over the material flow, reducing the risk of blockages and ensuring a continuous operation.
Pneumatic conveying technology, whether vacuum or positive pressure, offers significant advantages for the transportation of pearl salt granules. The ability to handle bulk materials efficiently, while maintaining product integrity, makes these systems indispensable in various industries. HeadPowder continues to innovate and develop advanced pneumatic conveying solutions that meet the evolving needs of the market.
By leveraging their expertise in engineering and material handling, HeadPowder provides tailored solutions that enhance operational efficiency and product quality. The company's commitment to precision and reliability ensures that clients can rely on their systems for long-term performance. As the demand for efficient bulk material handling grows, pneumatic conveying systems will remain a key technology in the industry, and companies like HeadPowder will play a crucial role in advancing these solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top