Shandong HeadPowder Engineering Co., Ltd., commonly known as Headpowder, is a professional manufacturer and supplier of industrial conveying equipment based in Shandong, China. The company specializes in the design, development, and production of advanced air-driven conveyors, particularly those tailored for the efficient handling of lightweight aggregate materials. This article delves into the fundamental principles of air-driven conveyors and highlights the key characteristics of their operational scenarios, providing a comprehensive overview for professionals in the construction and material processing industries.
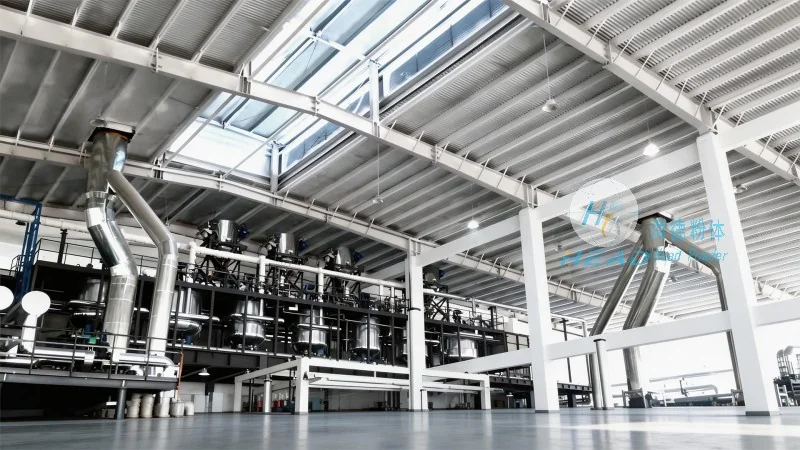
Lightweight aggregate materials, such as expanded clay, perlite, and vermiculite, are widely used in construction for their reduced weight and improved thermal insulation properties. Traditional bulk material handling methods, like belt conveyors or bucket elevators, may struggle with these materials due to their low density and tendency to create dust or clog systems. Air-driven conveyors offer a solution by utilizing compressed air to transport materials through a pipeline system, eliminating the need for mechanical components that can cause wear and tear or contamination. The technology behind these systems is centered on the principle of pneumatic transport, which can be categorized into two main types: positive pressure (or pressure) systems and negative pressure (or vacuum) systems. Positive pressure systems force air and material through the pipeline using a blower at the inlet, while negative pressure systems create a vacuum at the outlet to draw material into the pipeline. Both methods are effective for lightweight aggregates, but the choice between them depends on factors like material properties, distance, and system complexity.
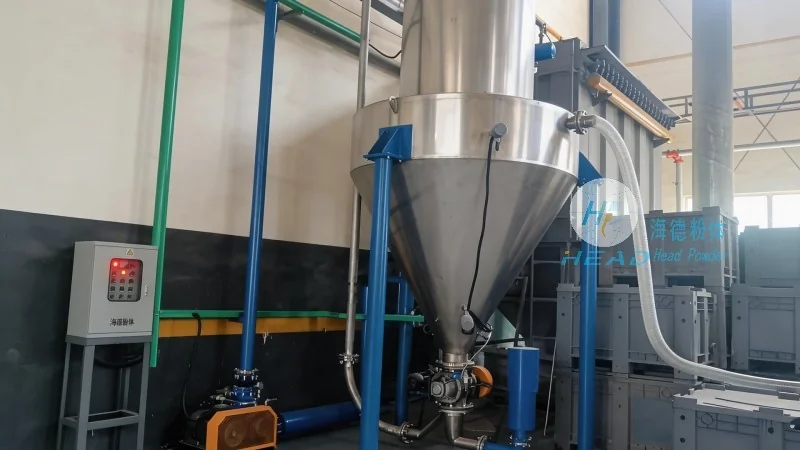
The operation of an air-driven conveyor for lightweight aggregates is based on the interaction between the material particles and the air flow within the pipeline. When the system is activated, compressed air is introduced into the inlet hopper, where it mixes with the lightweight aggregate. The air flow then propels the material through the pipeline, maintaining a consistent velocity to ensure smooth transport. The key to efficient pneumatic transport is achieving a proper air-to-material ratio, which balances the need for sufficient air to keep the material suspended and the energy consumption of the system. For lightweight aggregates, this ratio is typically higher than for denser materials, as the lower density requires more air to prevent settling and blockages. The conveyor system includes components such as a blower, inlet and outlet hoppers, a pipeline network, and control valves. The blower provides the necessary pressure or vacuum, while the hoppers facilitate the loading and unloading of materials. The pipeline is usually made of flexible or rigid materials, depending on the application, and is designed to withstand the pressure and temperature conditions of the conveying process. Control valves are used to regulate the flow of air and material, allowing for adjustments based on operational needs.
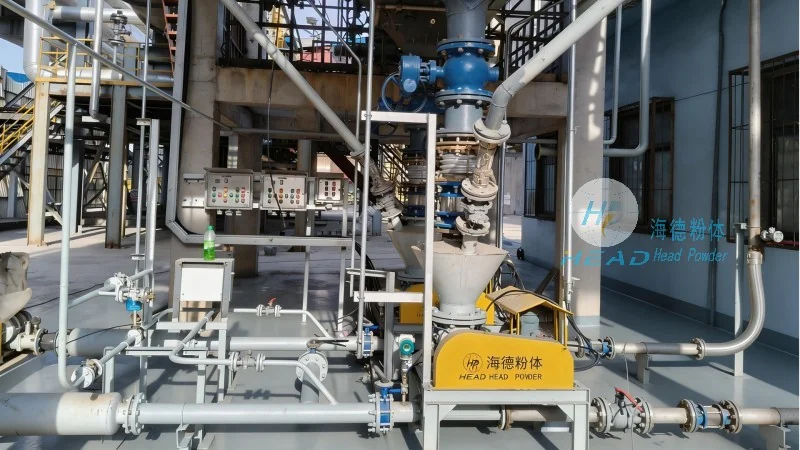
The application of air-driven conveyors for lightweight aggregates is characterized by several distinct features that make them suitable for specific operational environments. One of the primary advantages is their ability to handle materials over long distances without the need for intermediate transfer points. This is particularly beneficial in large construction sites or industrial plants where materials need to be transported from storage areas to processing units or production lines. The system can cover distances of several hundred meters or more, depending on the design and the type of lightweight aggregate being conveyed. Another important characteristic is the system's flexibility in terms of layout. Air-driven conveyors can be installed in various configurations, including straight lines, curves, and even vertical lifts, allowing for integration into existing facilities or new construction projects. This adaptability reduces the need for extensive civil works and minimizes the impact on the surrounding environment. Additionally, the technology is known for its low maintenance requirements compared to traditional mechanical conveyors. The absence of moving parts in the pipeline reduces wear and tear, and the use of durable materials ensures long-term reliability. This makes air-driven conveyors an economical choice for long-term material handling operations.
When used for lightweight aggregate materials, air-driven conveyors offer significant environmental and operational benefits. Unlike mechanical systems that may generate dust or cause noise pollution, pneumatic transport is relatively clean and quiet. The enclosed pipeline system prevents the release of fine particles into the air, reducing the risk of respiratory issues for workers and minimizing the impact on the environment. This is especially important in urban or residential areas where construction activities are common. From an operational perspective, air-driven conveyors can improve overall efficiency by reducing downtime and labor costs. The automated loading and unloading processes eliminate the need for manual handling, which not only increases safety but also speeds up the material transfer process. Furthermore, the system's ability to handle a wide range of lightweight aggregates without modification makes it a versatile solution for various applications. Whether it's transporting expanded clay for lightweight concrete production or perlite for insulation applications, the air-driven conveyor can adapt to different material properties and processing requirements. The integration of advanced control systems, such as variable frequency drives (VFDs) and sensors, allows for real-time monitoring and optimization of the conveying process, further enhancing efficiency and reducing energy consumption.
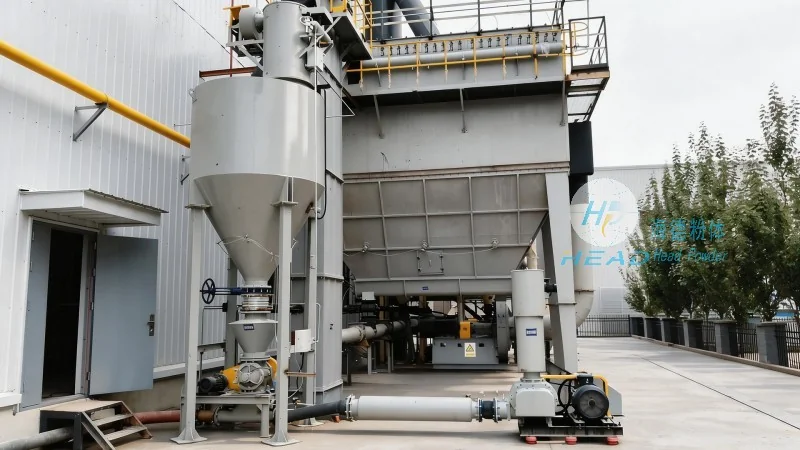
In conclusion, air-driven conveyors for lightweight aggregate materials represent a sophisticated and efficient solution for modern material handling needs. The principles of pneumatic transport, combined with the specific design considerations for lightweight materials, enable these systems to deliver reliable and cost-effective performance. The working scene characteristics, including long-distance transport, layout flexibility, and low maintenance, make them suitable for a wide range of industrial and construction applications. As the demand for lightweight construction materials continues to grow, the adoption of air-driven conveying technology is likely to increase, driven by the need for sustainable and efficient material handling solutions. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technology, providing high-quality air-driven conveyors that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top