What is a Calcium Phosphate Powder Conveying System Equipment? What is its Design Principle?
Release time:2026-09-14 18:59:47
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
Calcium phosphate is a crucial raw material in many industries, including pharmaceuticals, food, and chemical manufacturing. The efficient and reliable transportation of this powder is essential for maintaining production efficiency and product quality. This article explores the calcium phosphate powder conveying system equipment, its design principles, and the key factors that contribute to its optimal performance.
Understanding the Calcium Phosphate Powder Conveying System
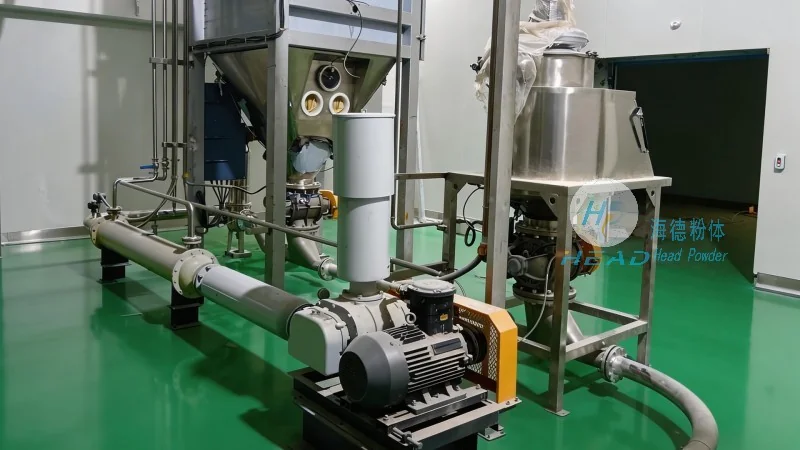
The calcium phosphate powder conveying system is a specialized piece of equipment designed to handle the transportation of calcium phosphate powder from one location to another within a production facility. This system is critical for ensuring that the powder moves smoothly and safely, minimizing the risk of dust generation, clogging, or material degradation. The system typically includes components such as hoppers, feeders, conveyors, and control systems, all working in tandem to achieve efficient material handling.
Key Design Principles for the System
The design of a calcium phosphate powder conveying system is based on several fundamental principles to ensure it meets the specific requirements of the application. These principles include:
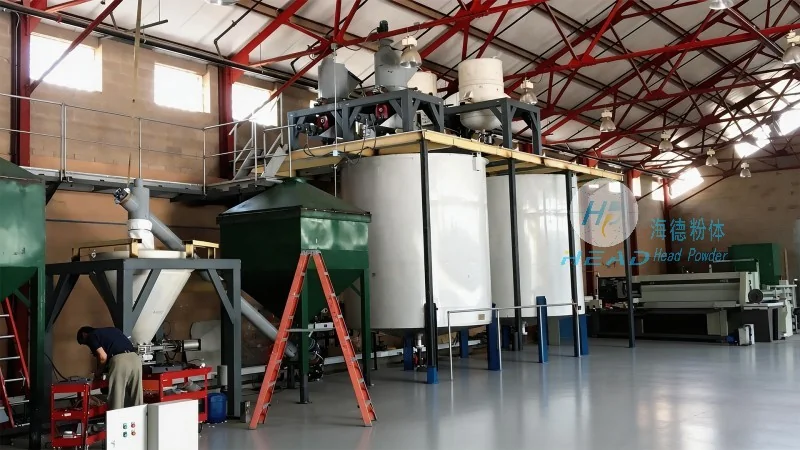
- Material Compatibility: The system components must be compatible with calcium phosphate powder to prevent chemical reactions or material degradation. Materials like stainless steel, PTFE, or specialized coatings are often used to ensure compatibility.
- Flow Control: Proper flow control is essential to prevent overloading or underloading of the conveyor. This is achieved through the use of feeders, such as rotary valves or vibratory feeders, which regulate the flow rate of the powder.
- Prevention of Clogging: Calcium phosphate powder can be prone to clogging due to its fine particle size and cohesive properties. The design incorporates features like angled hoppers, anti-static measures, and self-cleaning mechanisms to minimize clogging and ensure continuous operation.
- Dust Control: Effective dust control is crucial for maintaining a safe working environment and complying with environmental regulations. The system may include dust collection systems, sealed hoppers, and anti-static measures to reduce dust generation.
- Energy Efficiency: The design aims to minimize energy consumption while maintaining high conveying efficiency. This is achieved through the use of efficient motors, variable speed drives, and optimized conveyor designs.
Components of the Calcium Phosphate Powder Conveying System
The calcium phosphate powder conveying system consists of several key components, each playing a vital role in the overall operation:
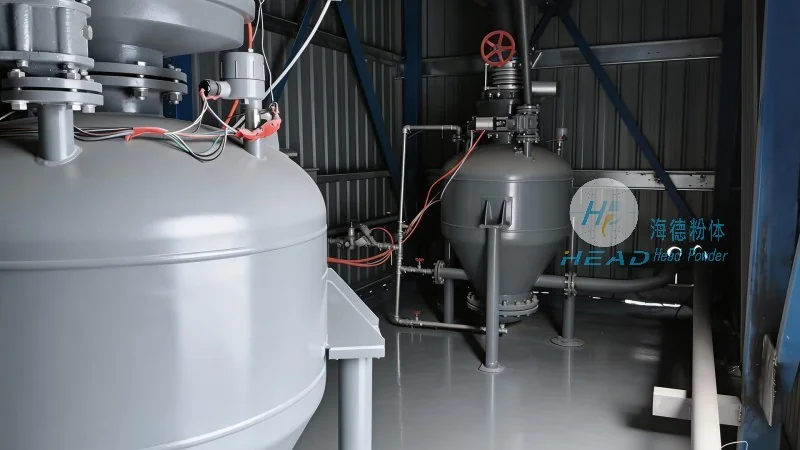
- Hoppers: The hoppers are used to store and feed the calcium phosphate powder into the system. They are typically designed with a conical or hopper shape to facilitate smooth material flow and prevent clogging.
- Feeders: Feeders regulate the flow of powder from the hopper to the conveyor. Common types include rotary airlock valves, vibratory feeders, and screw feeders, which are chosen based on the powder's characteristics and the required flow rate.
- Conveyors: The conveyor is the main component responsible for transporting the powder. Options include pneumatic conveyors (airslide or pressure), mechanical conveyors (belt or screw), or a combination of both. The choice depends on the distance, height, and material properties.
- Control Systems: The control system monitors and regulates the operation of the conveying system. It may include sensors for level, flow, and pressure, as well as control panels to adjust the speed of the conveyor or feeder.
Applications and Benefits of the System
The calcium phosphate powder conveying system is widely used in various industries due to its ability to handle fine powders efficiently and reliably. Some of the key benefits include:
- Improved Production Efficiency: By ensuring a consistent and continuous flow of powder, the system reduces downtime and increases overall production output.
- Enhanced Product Quality: The system minimizes material degradation and contamination, leading to higher quality products.
- Safe Working Environment: Proper dust control and sealed systems ensure a safe working environment for operators.
- Cost-Effective Operation: The design focuses on energy efficiency and minimal maintenance, reducing long-term operational costs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized powder handling equipment. With a focus on innovation and quality, the company designs and manufactures calcium phosphate powder conveying systems tailored to the specific needs of its clients. Headpowder's expertise in material handling technology ensures that their systems are reliable, efficient, and compliant with industry standards. The company's commitment to customer satisfaction and product excellence has made it a trusted partner in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
