Understanding Nitrile Rubber Pneumatic Conveying Equipment and Its Design Principles
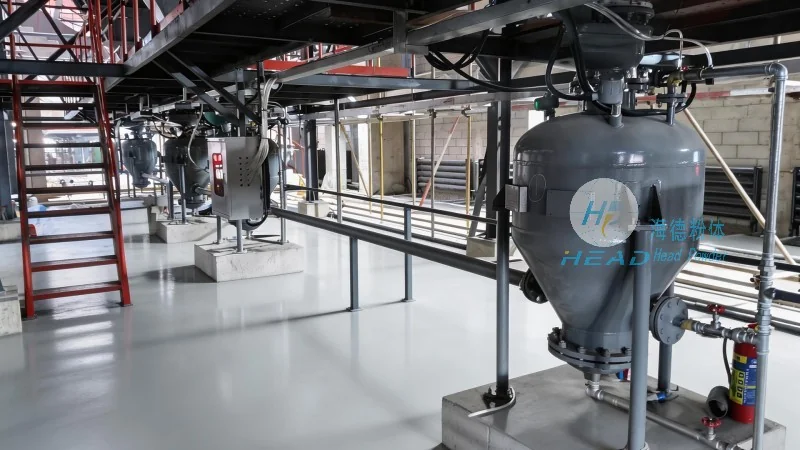
Nitrile rubber pneumatic conveying equipment is a specialized system designed to transport bulk materials through an enclosed pipeline using air or other gases as the conveying medium. This technology is widely used in various industrial applications, particularly where materials like nitrile rubber or similar compounds need to be moved efficiently and safely. The system combines the properties of nitrile rubber, known for its excellent resistance to oil, fuel, and other chemicals, with the pneumatic conveying mechanism to ensure reliable material handling. Such equipment is often provided by companies like Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializing in engineering solutions for material handling systems.
The core components of a nitrile rubber pneumatic conveying system typically include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, a pressure vessel or receiver to collect the material at the end, and a blower or compressor to generate the necessary air pressure. Each component is carefully selected to withstand the chemical and mechanical stresses associated with nitrile rubber and the conveying process. For instance, the hopper and feeder are often constructed from materials compatible with nitrile rubber to prevent contamination and ensure consistent material flow. The conveying pipeline is usually made of corrosion-resistant materials, such as stainless steel or specialized polymers, to maintain the integrity of the nitrile rubber and prevent degradation.
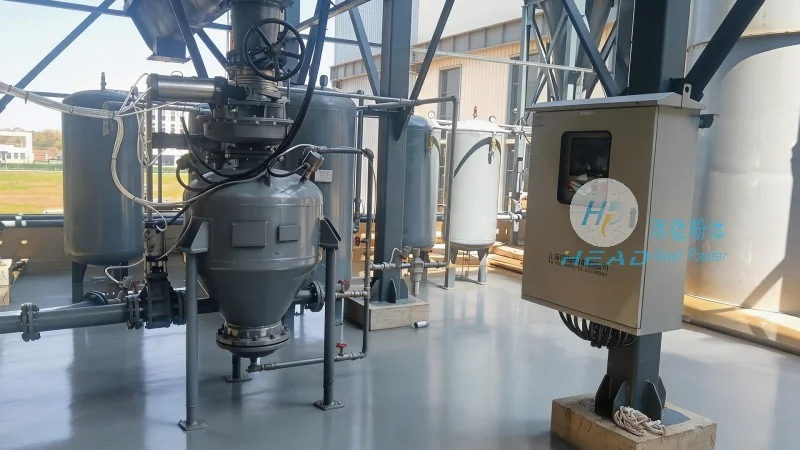
The design principles of nitrile rubber pneumatic conveying equipment focus on optimizing material transport efficiency, minimizing wear and tear, and ensuring safety. The system operates on the principle of creating a pressure differential between the inlet and outlet of the pipeline. By injecting air or gas into the pipeline at a controlled velocity, the material is entrained and transported through the system. The velocity of the air is crucial; it must be high enough to keep the material suspended but low enough to prevent excessive wear on the pipeline and components. The design also considers the material's properties, such as its density, particle size, and moisture content, as these factors influence the required air velocity and pressure.
One of the primary advantages of incorporating nitrile rubber into pneumatic conveying equipment is its exceptional chemical resistance. Nitrile rubber is highly resistant to oils, fuels, and various solvents, making it ideal for handling materials that are otherwise difficult to transport with traditional systems. This resistance ensures that the equipment remains in good condition even when dealing with aggressive chemicals, reducing maintenance costs and extending the lifespan of the system. Additionally, nitrile rubber's flexibility and durability contribute to the overall reliability of the conveying process, as it can withstand repeated flexing and pressure changes without degradation.
Nitrile rubber pneumatic conveying equipment is commonly employed in industries where the handling of rubber compounds, chemicals, and other similar materials is essential. For example, in the tire manufacturing industry, nitrile rubber is used to transport raw rubber materials and additives to production lines. In the chemical industry, it is used to convey various chemical powders and granules, including those that are sensitive to moisture or air. The equipment is also utilized in the pharmaceutical and food processing industries, where hygiene and material purity are paramount. The versatility of nitrile rubber allows these systems to be adapted to a wide range of applications, making them a preferred choice for many industrial processes.
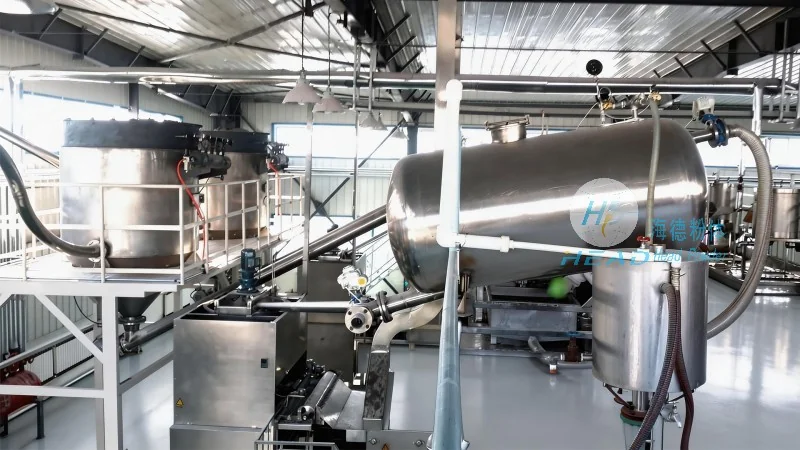
Proper maintenance is crucial to ensure the longevity and efficiency of nitrile rubber pneumatic conveying equipment. Regular inspections of the components, such as the hopper, feeder, and pipeline, are necessary to check for signs of wear, corrosion, or contamination. The nitrile rubber parts, in particular, should be inspected for any cracks or degradation, as these can affect the material's performance and the overall system's integrity. Cleaning the system regularly, especially after handling different materials, is also important to prevent cross-contamination and maintain the quality of the conveyed products. Additionally, monitoring the air pressure and flow rate can help identify any issues early on, allowing for timely repairs and adjustments.
Nitrile rubber pneumatic conveying equipment plays a vital role in modern industrial operations by providing an efficient, safe, and reliable method for transporting bulk materials. The design principles and components are carefully engineered to handle the unique properties of nitrile rubber, ensuring optimal performance and longevity. As industries continue to evolve and demand more efficient material handling solutions, the importance of such equipment will only grow. With proper maintenance and operation, nitrile rubber pneumatic conveying systems can provide consistent performance, reducing downtime and increasing productivity in various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top