For industries dealing with powders and granules, maintaining a clean and efficient production environment is crucial. This is where dust-free closed-loop pneumatic conveying systems come into play. These advanced equipment solutions are designed to transport bulk materials like powders, granules, and other particulate substances in a sealed environment, preventing dust contamination and ensuring product integrity. In this article, we will explore what these systems are, their core design principles, and the benefits they offer to various sectors.
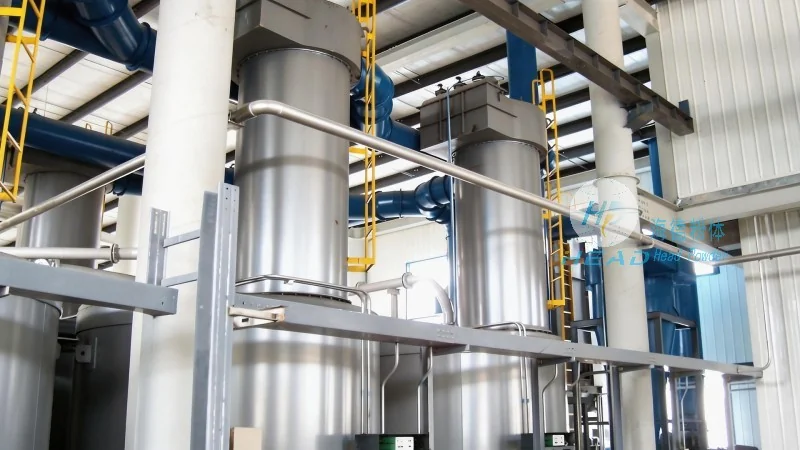
A dust-free closed-loop pneumatic conveying system is a specialized piece of industrial equipment used for the transport of dry bulk materials. Unlike traditional open systems that may allow dust to escape into the environment, these systems operate in a completely enclosed loop, ensuring that all material is contained within the pipeline and returned to the system for reuse or disposal. This design not only protects the workplace from dust pollution but also maintains the quality of the conveyed material by preventing contamination from external sources.
The primary feature of a dust-free closed-loop system is its sealed, closed-loop design. This means that the entire conveying path, from the material inlet to the discharge point, is enclosed in a series of pipes and vessels. The system typically includes components such as a hopper for material storage, a blower or compressor to generate the necessary air pressure, a filter to capture any fine particles that might escape, and a return line to recycle the air back to the blower. The closed-loop design ensures that no air or dust is released into the ambient environment, making it ideal for applications where air quality and product purity are paramount.
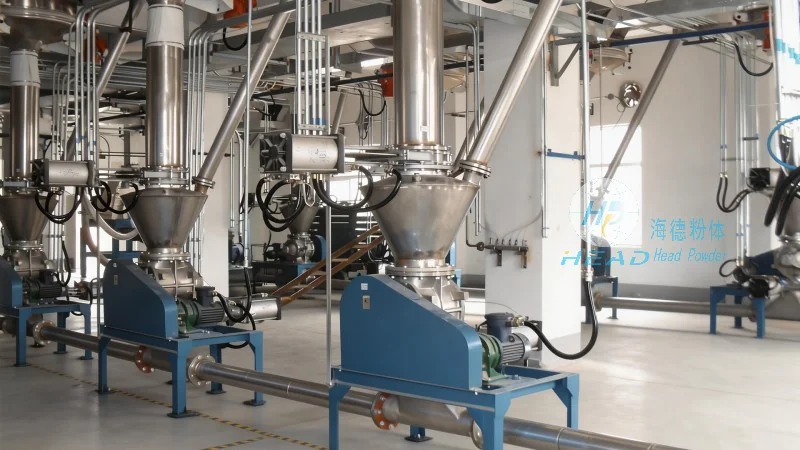
The design of a dust-free closed-loop pneumatic conveying system is based on several fundamental principles. The most critical is the use of positive pressure to move the material through the system. The blower creates a high-pressure air stream that propels the material particles along the pipeline. The system is engineered to maintain a consistent pressure and flow rate, which is essential for efficient material transport. Additionally, the design incorporates features like air filtration and recycling to minimize energy consumption and maintain a stable operating environment. The choice of materials for the pipes and components is also crucial, as they must be resistant to corrosion and wear from the conveyed materials.
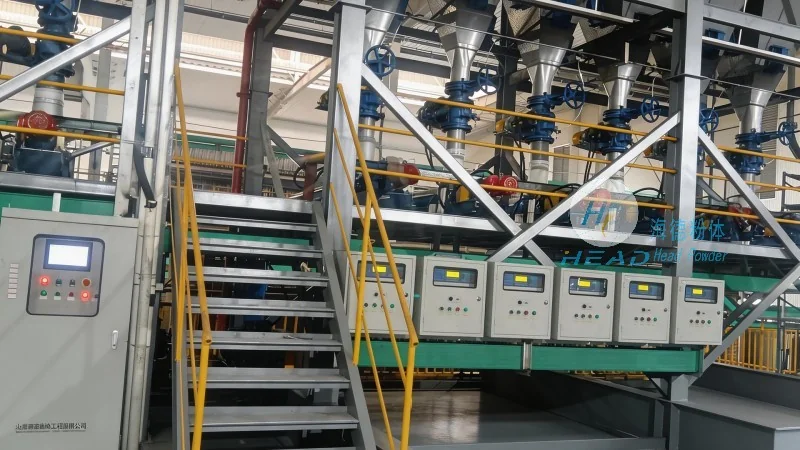
Dust-free closed-loop pneumatic conveying systems are widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and agriculture. In the pharmaceutical industry, for example, these systems are essential for transporting active ingredients and other powders without compromising the sterile environment. In food processing, they help maintain hygiene standards by preventing cross-contamination and dust accumulation. The benefits of using such systems include improved product quality, reduced environmental impact, increased operational efficiency, and lower maintenance costs due to the sealed design that minimizes wear and tear on components.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of advanced powder handling equipment. With a focus on innovation and quality, the company specializes in designing and producing dust-free closed-loop pneumatic conveying systems tailored to the specific needs of various industries. HeadPowder's products are engineered to meet stringent industry standards and are known for their durability, efficiency, and reliability. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge solutions for the global powder handling market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top