Manganese carbonate is a vital industrial chemical widely used in various sectors such as battery manufacturing, steel production, and chemical synthesis. Its handling and transportation require efficient methods to ensure safety, efficiency, and minimal loss. Pneumatic conveying, a technology that uses air or other gases to transport bulk materials, has become a preferred solution for moving manganese carbonate. This article explores the concept of manganese carbonate pneumatic conveying and delves into its fundamental design principles, providing a comprehensive overview for professionals in the field.
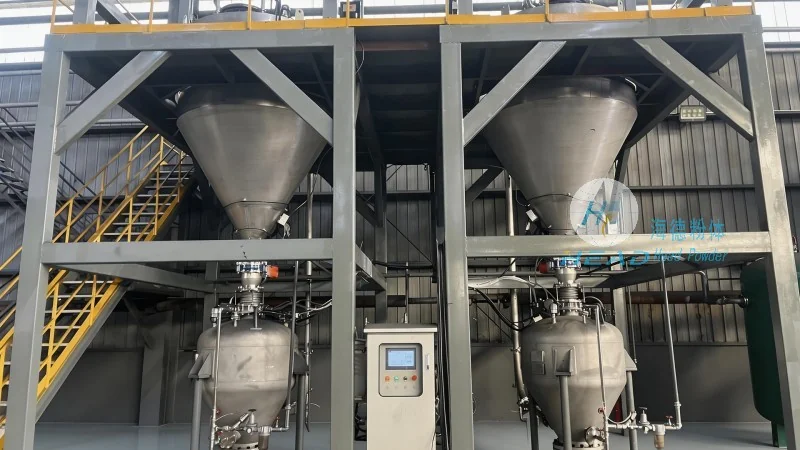
Before diving into the design principles, it's essential to understand the material being conveyed and the technology itself. Manganese carbonate, with its specific physical properties like particle size, density, and moisture content, influences the choice of pneumatic conveying system. Pneumatic conveying systems can be categorized into two main types: dilute phase and dense phase. Dilute phase systems use low air velocity to transport particles in a suspended state, while dense phase systems employ higher air velocity and pressure to move material in a slurry-like state. The selection of the appropriate system depends on the characteristics of the manganese carbonate and the distance it needs to be transported.
The design of a manganese carbonate pneumatic conveying system involves several critical principles aimed at optimizing performance, ensuring material integrity, and maintaining operational safety. The first principle is the selection of the right air velocity and pressure. For dilute phase systems, the air velocity must be high enough to keep the particles suspended but not so high as to cause excessive wear on the system components. The pressure drop across the system is another crucial factor, as it affects the energy consumption and the ability to transport the material over long distances. Engineers must calculate the pressure drop accurately to determine the required power and the overall system efficiency.
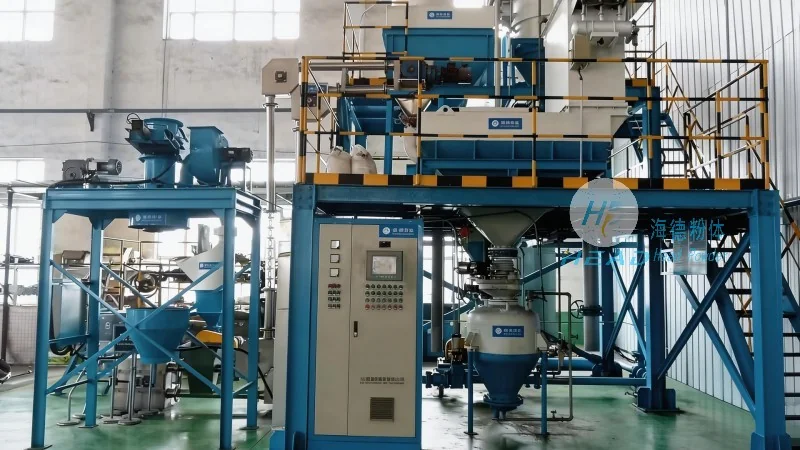
A typical manganese carbonate pneumatic conveying system consists of several key components, each playing a vital role in the process. The first component is the material feed hopper, which stores and feeds the manganese carbonate into the system. The hopper is designed to prevent material buildup and ensure a consistent flow rate. The next component is the air compressor or blower, which generates the necessary air pressure to move the material. The air velocity and pressure are controlled by the compressor, which can be adjusted based on the system's requirements. The conveying line, usually made of stainless steel or other corrosion-resistant materials, transports the material from the feed point to the discharge point. The line is equipped with valves and fittings to control the flow and direct the material to the desired location. The discharge hopper or silo is the final component, where the manganese carbonate is collected and stored. The system may also include filters and cyclones to separate the material from the air, ensuring that the material is not lost and that the air is clean.
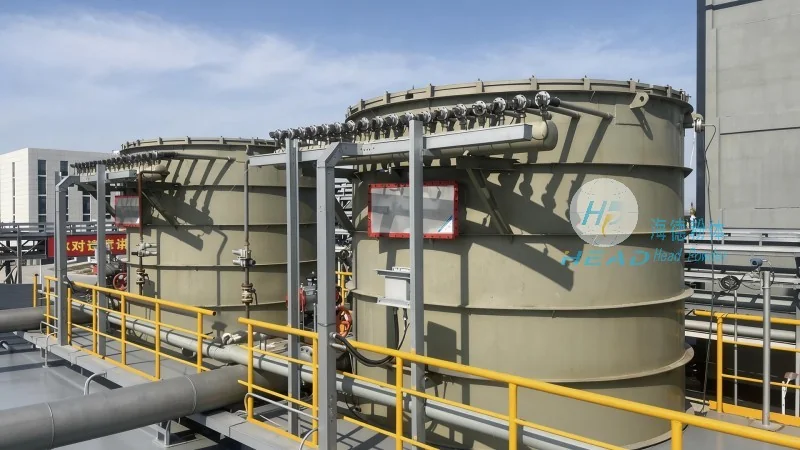
Operational considerations are essential for the efficient and safe operation of a manganese carbonate pneumatic conveying system. One of the primary factors is the particle size distribution of the material. Larger particles may require higher air velocity to remain suspended, while smaller particles can be conveyed at lower velocities. The moisture content of the manganese carbonate also affects the system's performance, as high moisture can cause clogging and reduce the conveying efficiency. Temperature control is another important factor, as high temperatures can affect the material's properties and the system's components. Regular maintenance is crucial to ensure the system operates at optimal efficiency. This includes checking the air compressor, cleaning the filters, and inspecting the conveying line for any signs of wear or damage. By addressing these operational considerations, the system can achieve high efficiency and long-term reliability.
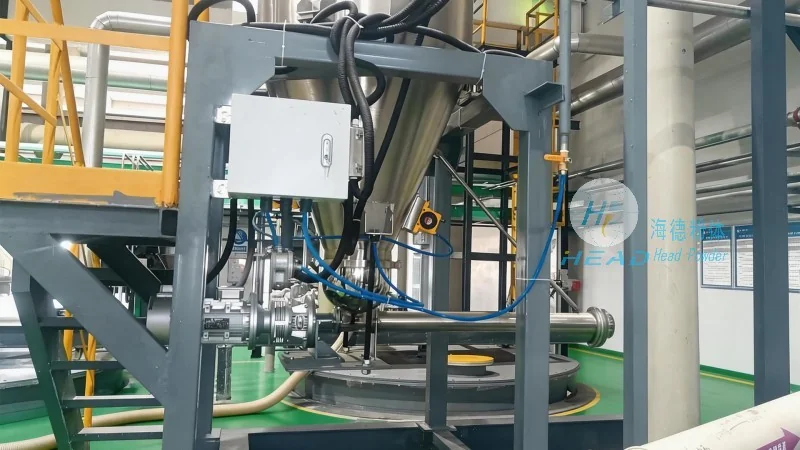
Manganese carbonate pneumatic conveying systems are widely used in various industries where the material needs to be transported over long distances or in hazardous environments. The battery manufacturing industry is a major user of manganese carbonate, as it is used in the production of lithium-ion batteries. The steel industry also uses manganese carbonate as a raw material for steel production, and the chemical industry uses it in the synthesis of other chemicals. The pharmaceutical industry may also use manganese carbonate in the production of certain drugs. The system's ability to transport the material safely and efficiently makes it a preferred choice in these industries.
Shandong HeadPowder Engineering Co., Ltd., a leading company in the field of powder handling and conveying systems, specializes in designing and implementing manganese carbonate pneumatic conveying systems. The company has extensive experience in working with various industrial materials, including manganese carbonate, and has developed a deep understanding of the material's properties and the requirements of different industries. The company's engineers use advanced design software and methodologies to create customized systems that meet the specific needs of their clients. The company provides comprehensive services, from initial consultation and system design to installation and maintenance. By leveraging their expertise and experience, Shandong HeadPowder Engineering Co., Ltd. helps clients optimize their material handling processes and improve their overall efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top