Stone aggregate pneumatic conveying is a sophisticated method used to transport bulk materials like stone aggregates, sand, and gravel through a pipeline using air pressure. This technology has become increasingly vital in construction and industrial sectors due to its efficiency and ability to handle abrasive materials without mechanical wear. The process involves creating a flow of air within a pipeline, which lifts and transports the solid particles. It's a key solution for material handling in environments where traditional methods like belt conveyors or trucks are impractical or inefficient. HeadPowder, a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries.
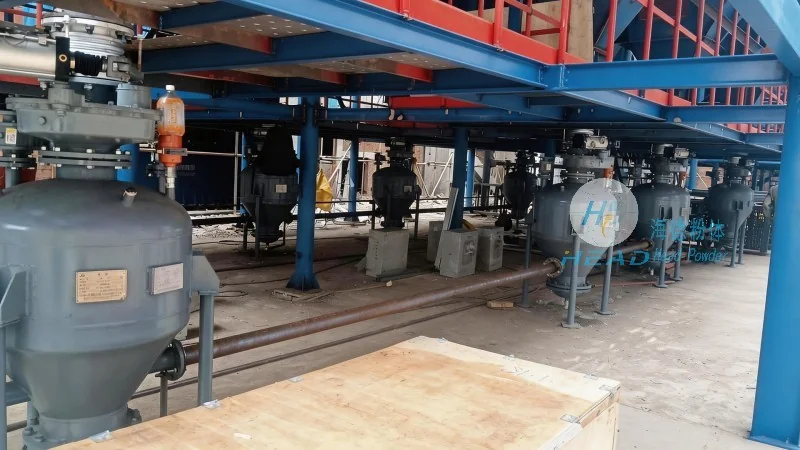
The design of a stone aggregate pneumatic conveying system is based on several critical principles to ensure optimal performance and reliability. First, the system must maintain a consistent air velocity to keep the material suspended and prevent settling. This velocity is typically calculated based on the material's properties, such as particle size, density, and shape. Second, the system's pressure and flow rate are carefully controlled to avoid excessive wear on components and to minimize energy consumption. Engineers use computational fluid dynamics (CFD) and empirical formulas to determine the optimal air volume and pressure required for specific applications. Third, the system incorporates features like cyclones and filters to separate the conveyed material from the air stream, ensuring clean material delivery and preventing dust contamination. The design also considers the pipeline layout, including bends and vertical sections, to minimize pressure losses and maintain material flow. Additionally, safety features such as pressure relief valves and explosion-proof components are integrated to handle potential hazards associated with high-pressure air systems.
A typical stone aggregate pneumatic conveying system consists of several key components that work in tandem to achieve efficient material transport. The primary components include a material hopper, an air compressor, a pipeline network, a conveying line, and a discharge hopper or silo. The material hopper stores the stone aggregates and feeds them into the system. The air compressor generates the necessary air pressure to create the conveying flow. The pipeline network transports the material from the hopper to the discharge point, with bends and vertical sections designed to accommodate the material's trajectory. The conveying line itself is usually made of durable materials like stainless steel or high-density polyethylene to withstand the abrasive nature of stone aggregates. At the discharge end, a cyclone separator or a filter unit separates the material from the air, allowing the material to be collected in a storage bin or silo while the air is either recirculated or vented to the atmosphere. The system operates by first charging the pipeline with air, then introducing the material into the air stream. The air velocity is maintained above the material's terminal velocity to keep the particles suspended. As the material travels through the pipeline, it experiences pressure changes, which can cause the material to accelerate or decelerate. The design of the system ensures that these pressure changes are managed to prevent material blockages or excessive wear on the pipeline.
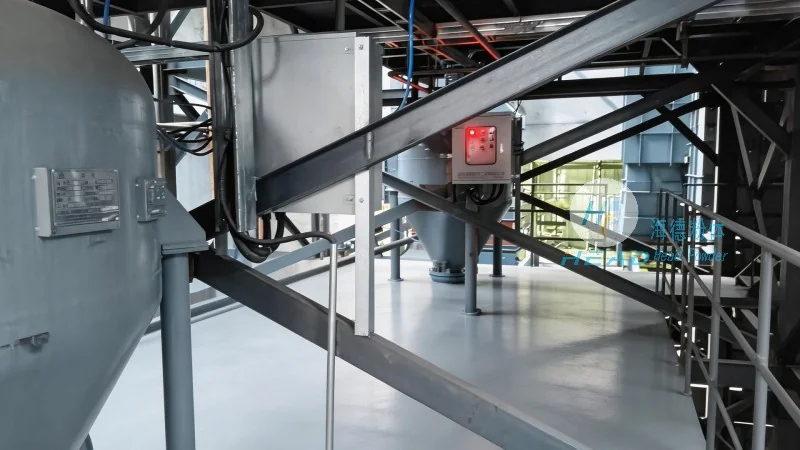
Stone aggregate pneumatic conveying offers several advantages over traditional material handling methods. One of the most significant benefits is its ability to transport materials over long distances without the need for multiple transfer points or intermediate storage. This reduces the overall cost and complexity of material handling systems. Additionally, the system is highly flexible, as it can be easily reconfigured to handle different material types or to adjust the conveying distance. The absence of moving parts in the conveying line minimizes maintenance requirements and reduces downtime compared to mechanical conveyors. Another advantage is the ability to handle abrasive materials without significant wear on the system components. The air pressure and flow rate can be adjusted to match the material's properties, ensuring efficient and safe transport. Furthermore, the system can be integrated with other industrial processes, such as mixing or processing, to create a seamless material handling workflow. The use of pneumatic conveying also reduces the risk of material contamination, as the material is contained within the pipeline and is not exposed to external elements. This is particularly important for applications where material purity is critical, such as in the production of concrete or other construction materials.
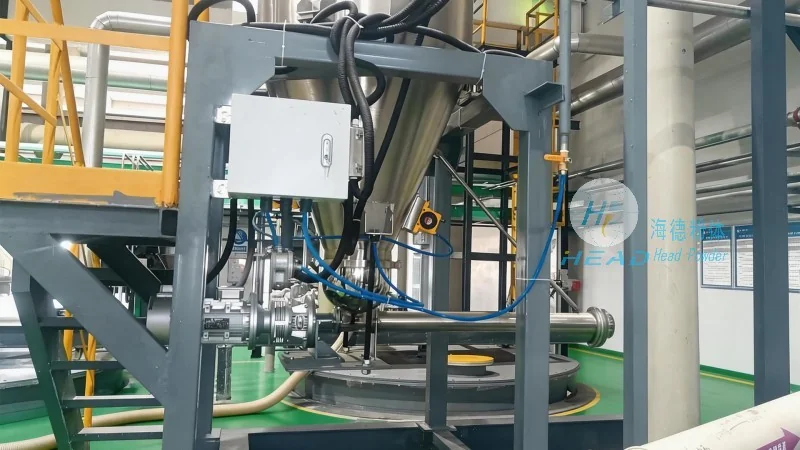
Stone aggregate pneumatic conveying is widely used in various construction and industrial applications. In the construction industry, it is commonly used to transport aggregates from storage silos to concrete mixing plants or to job sites. The system can handle large volumes of material, making it suitable for high-production construction projects. In the mining industry, pneumatic conveying is used to transport crushed stone or ore from processing plants to storage facilities or for further processing. The system's ability to handle abrasive materials makes it ideal for mining applications where other conveyors may wear out quickly. In the chemical and pharmaceutical industries, pneumatic conveying is used to transport raw materials or finished products, such as powders or granules, to processing lines or packaging areas. The system's flexibility and ability to maintain material purity make it a preferred choice in these sectors. Additionally, the system is used in the food industry for transporting grains or other food products, where hygiene and contamination control are paramount. The versatility of stone aggregate pneumatic conveying makes it a valuable solution across multiple industries, providing efficient and reliable material handling solutions.
When designing and installing a stone aggregate pneumatic conveying system, several factors must be considered to ensure optimal performance and longevity. First, the material properties, such as particle size distribution, density, and moisture content, must be thoroughly analyzed to determine the appropriate air velocity and pressure. These properties affect the material's flow characteristics and its interaction with the air stream. Second, the system's capacity must be matched to the production requirements to avoid underutilization or overloading. The system's capacity is determined by the air volume and pressure, as well as the pipeline diameter and length. Third, the system's layout must be carefully planned to minimize pressure losses and to ensure smooth material flow. The pipeline should be designed with gradual bends and minimal vertical changes to prevent material settling or blockages. Fourth, the components must be selected based on the material's abrasive nature to ensure durability. High-quality materials like stainless steel or wear-resistant coatings are recommended for the pipeline and components. Fifth, safety considerations must be addressed, including pressure relief valves, explosion-proof components, and proper ventilation. The system must comply with local regulations and standards to ensure safe operation. Finally, regular maintenance and monitoring are essential to maintain the system's performance and to identify potential issues before they become major problems. Regular cleaning of the cyclone separators and filters, as well as checking for wear on the pipeline and components, are important maintenance tasks.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top