HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of pneumatic conveying systems for various industrial applications. This article delves into the fundamental principles behind the operation of bicarbonate of soda pneumatic conveying equipment, highlighting the technical aspects and practical applications that make such systems efficient and reliable.
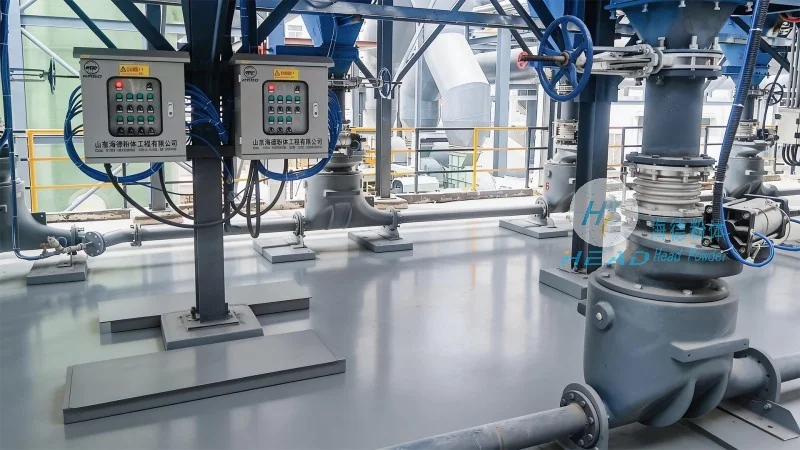
Pneumatic conveying is a method of transporting bulk materials through a pipeline using a gas stream, typically air or a mixture of air and other gases. The process involves creating a pressure differential within the system to move the material from the source to the destination. For bicarbonate of soda, which is a fine, dry powder, pneumatic conveying offers several advantages over traditional methods like belt conveyors or bucket elevators.
The operation of a bicarbonate of soda pneumatic conveying system relies on several key components that work in concert to ensure efficient material transport. These components include the material hopper, the feeder, the air compressor, the conveying line, and the discharge device. Each component plays a critical role in the overall performance of the system.
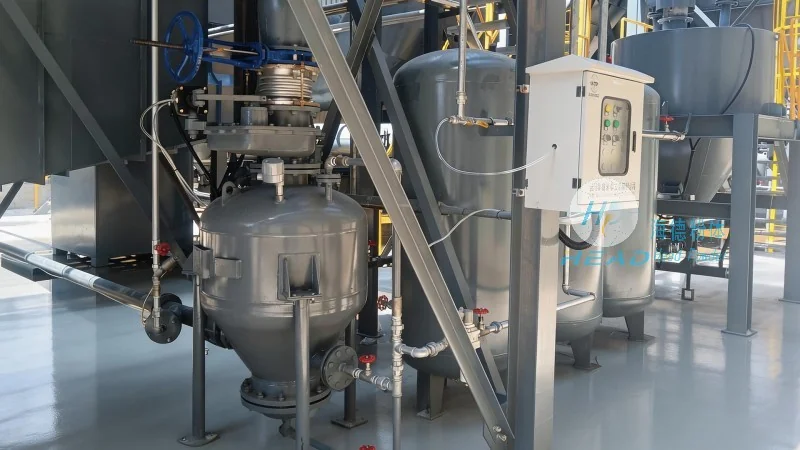
When the system is activated, the air compressor generates a high-pressure air stream. This air is then introduced into the conveying line, creating a flow that pulls the bicarbonate of soda powder from the hopper. The feeder controls the rate at which the powder is released into the air stream, ensuring a consistent flow rate. The conveying line transports the material to the discharge point, where the air is released and the powder is collected.
Compared to other material handling methods, pneumatic conveying offers several benefits for transporting bicarbonate of soda. These include reduced product contamination, as the material is not in direct contact with mechanical parts. Additionally, the system can handle fine powders without causing dust accumulation or clogging, which is a common issue with other methods. The flexibility of the system also allows for easy integration into existing production lines, making it a cost-effective solution for many industrial applications.
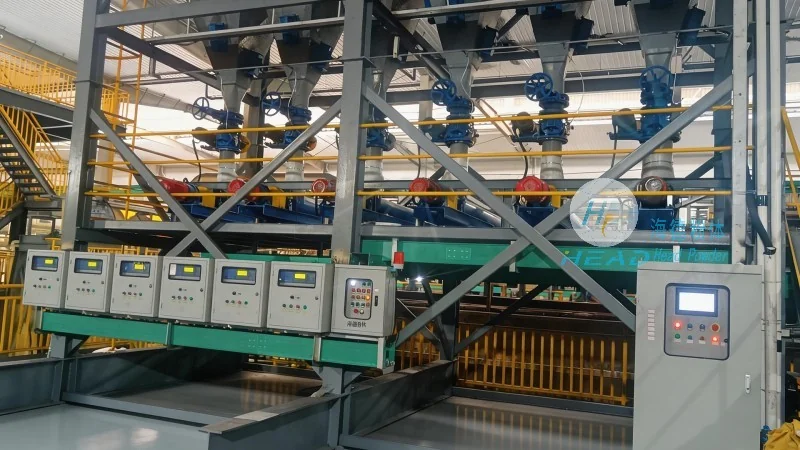
Bicarbonate of soda pneumatic conveying equipment is widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, it is used to transport ingredients for baking and other food products. In pharmaceuticals, the system ensures that the powder is handled in a sterile environment, preventing contamination. In chemical manufacturing, the equipment is used to transport raw materials and finished products, improving overall production efficiency.
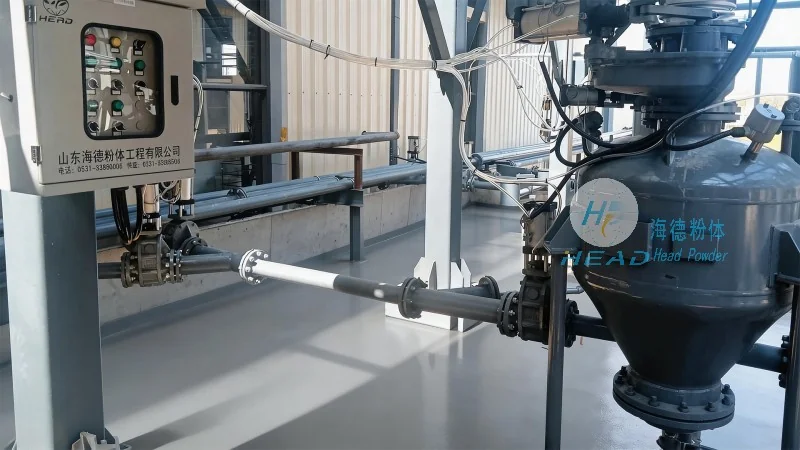
To ensure the longevity and efficiency of the pneumatic conveying system, regular maintenance is essential. This includes checking the air compressor for proper operation, cleaning the conveying line to prevent clogging, and inspecting the feeder for any blockages. Additionally, the system should be operated within the recommended pressure and flow rates to avoid damage to the components. Proper training of operators is also crucial to ensure safe and efficient operation of the equipment.
HeadPowder's bicarbonate of soda pneumatic conveying equipment is a reliable and efficient solution for transporting fine powders in various industrial applications. By understanding the principles behind the operation of such systems, users can make informed decisions about their material handling needs and choose the right equipment for their specific requirements. With proper maintenance and operation, these systems can provide long-term benefits and improve overall production efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top