Alumina, a vital industrial material widely utilized in ceramics, refractories, and chemical industries, demands efficient and reliable transportation methods for processing and distribution. Pneumatic conveying equipment offers a sophisticated solution for handling alumina powder, ensuring safe, clean, and high-efficiency material transport. This article explores the fundamental principles behind alumina pneumatic conveying systems, highlighting the technology's operational mechanisms, key components, and practical applications.
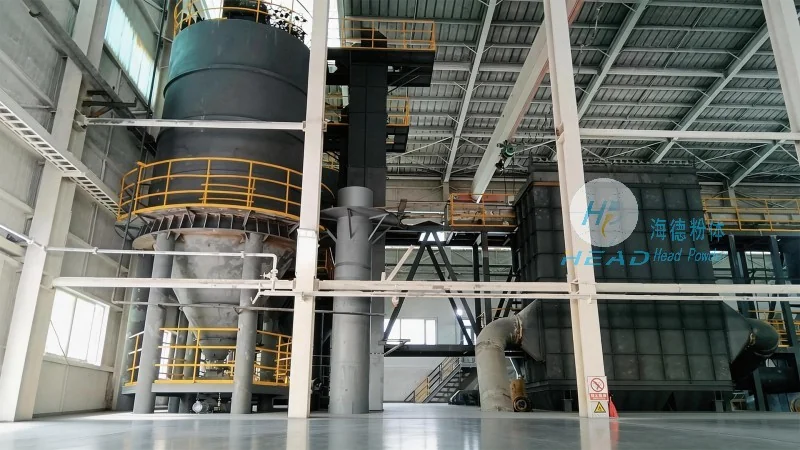
The pneumatic conveying of alumina relies on fluid dynamics and particle transport principles. At its core, the system uses compressed air or gas to generate a flow that propels alumina particles through a pipeline. The process typically involves creating a pressure differential between the inlet and outlet of the conveying line. As air is introduced, it creates a low-pressure zone that draws alumina particles into the pipeline. The air flow then carries these particles along the pipeline, maintaining consistent velocity to prevent deposition or clogging. The system's design—including air nozzle type, pipeline diameter, and air velocity—is critical for optimal performance. For fine, abrasive alumina, the system must be engineered to handle high-velocity air flows while minimizing particle degradation and equipment wear.
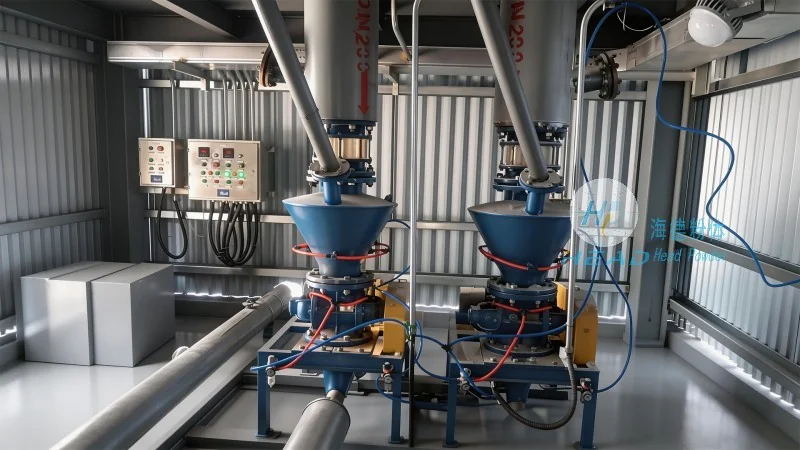
Alumina pneumatic conveying systems consist of interconnected components, each with a vital role. Primary components include the material feed system (hopper or rotary valve), air supply unit (blower or compressor), conveying pipeline (corrosion/abrasion-resistant materials like stainless steel or specialized plastics), and discharge mechanism (rotary valve or cyclone separator). The feed system ensures controlled alumina supply; the air supply unit generates necessary pressure/volume; the pipeline transports particles, with bends/elbows optimized to minimize pressure loss. The discharge mechanism collects alumina at the destination, separating it from the air stream. Each component must be carefully selected and integrated to ensure efficient, reliable operation, especially for fine alumina prone to clogging or degradation.
Compared to mechanical conveying (e.g., screw or belt conveyors), pneumatic conveying offers distinct benefits for alumina handling. A key advantage is the closed system, which prevents dust contamination and environmental pollution—critical for alumina used in high-purity applications like ceramics or refractory production. The system also enables flexible, scalable designs for long-distance or multi-point transport, easily integrating with other industrial equipment (mixers, reactors) to form seamless production lines. Another benefit is reduced material degradation: smooth pipeline surfaces and controlled air velocities mitigate the abrasive nature of alumina. Finally, pneumatic systems are generally more energy-efficient, achieving higher throughput with lower power consumption.
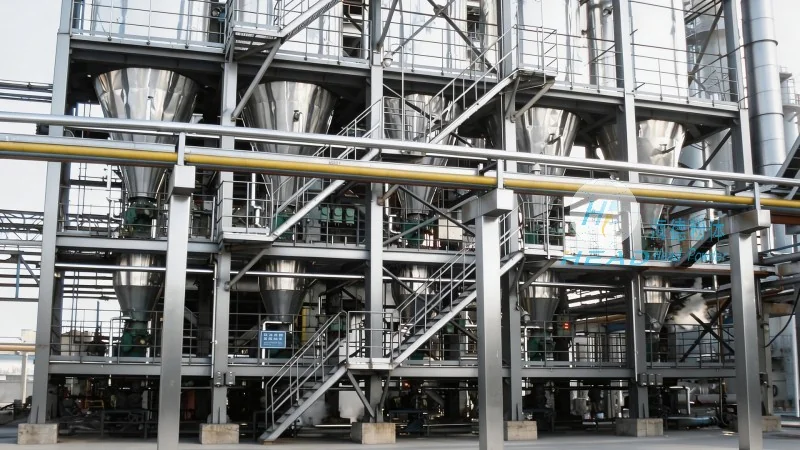
Alumina pneumatic conveying equipment is widely used in ceramics and chemical industries. In ceramic manufacturing, alumina serves as a raw material for high-strength, heat-resistant ceramics; the system delivers powder without contamination to mixing/molding processes. In the chemical industry, alumina acts as a catalyst or adsorbent; the closed system maintains purity. For refractory production, alumina is used to create high-temperature-resistant bricks; the system efficiently transports powder to the production line. These applications highlight the importance of reliable, efficient alumina pneumatic conveying systems in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top