Activated carbon is widely used in various industrial processes for its excellent adsorption properties, particularly in air purification, water treatment, and environmental remediation. The efficient and reliable transportation of activated carbon from storage to processing units is crucial for maintaining system performance and operational efficiency. Pneumatic conveying systems offer a solution to this challenge by utilizing air or gas to transport bulk materials like activated carbon through pipelines. This article explores the fundamental principles behind activated carbon pneumatic conveying equipment, detailing its components, working mechanisms, and key considerations for optimal performance. The equipment is manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions based in Shandong, China.
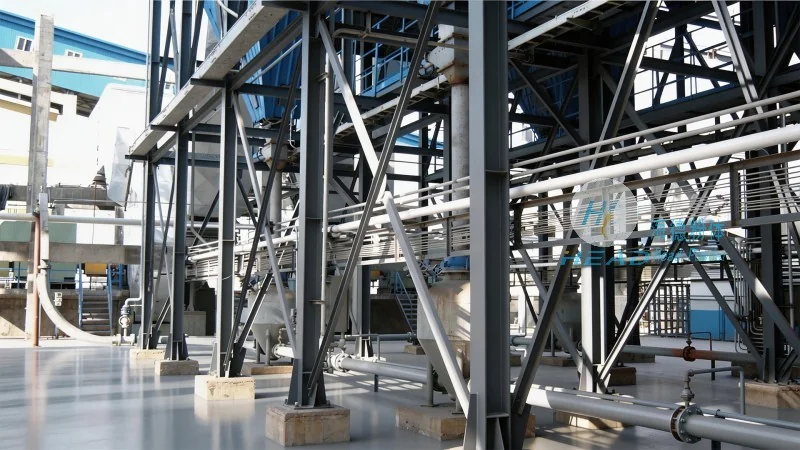
The activated carbon pneumatic conveying equipment typically consists of several essential components that work in concert to achieve material transport. The primary components include a material feeder, a conveying pipeline, a pressure vessel or receiver, a blower or air compressor, and control valves. The material feeder, often a hopper or screw feeder, ensures a consistent flow of activated carbon into the system. The conveying pipeline, made of materials resistant to the abrasive nature of activated carbon, carries the material from the feeder to the receiver. The pressure vessel or receiver collects the conveyed material and may include a discharge valve for downstream processing. The blower or air compressor provides the necessary air pressure to move the material through the pipeline. Control valves, such as check valves and flow control valves, regulate the air flow and pressure to maintain system stability and prevent backflow.
The operation of activated carbon pneumatic conveying equipment is based on the principle of fluidization and drag. In a dilute phase system, the air or gas is introduced into the conveying pipeline at a velocity sufficient to suspend the activated carbon particles in the air stream. The particles are carried along the pipeline by the air flow, moving from the feeder to the receiver. In a dense phase system, the air velocity is lower, causing the particles to form a slurry-like flow, which is more suitable for long-distance or high-pressure applications. The choice between dilute and dense phase systems depends on factors such as the distance to be covered, the material's characteristics, and the required flow rate. The system operates by creating a pressure differential between the feeder and the receiver, with the blower maintaining the pressure to ensure continuous material transport. The control system monitors parameters like pressure, flow rate, and material level to adjust the air supply and prevent system failures.
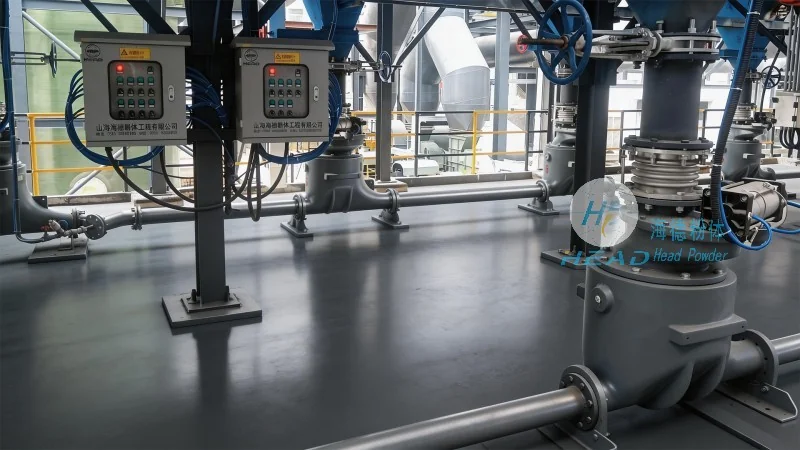
Activated carbon pneumatic conveying offers several advantages over traditional mechanical conveying methods. One of the key benefits is the ability to transport material over long distances without the need for intermediate transfer points, reducing the risk of material loss and contamination. The system is also highly flexible, allowing for changes in the conveying route or flow rate without major modifications. Additionally, pneumatic conveying is less prone to material degradation compared to mechanical systems, which can cause abrasion or breakage of the activated carbon particles. The equipment is also relatively compact and can be integrated into existing industrial facilities, minimizing space requirements. Another advantage is the ability to handle a wide range of material sizes and moisture content, making it suitable for various activated carbon grades and applications.
Activated carbon pneumatic conveying equipment is widely used in industrial applications where activated carbon is a critical component. In the environmental sector, it is used for the transport of activated carbon in air pollution control systems, water treatment plants, and industrial wastewater treatment facilities. The equipment ensures that the activated carbon is delivered to the adsorption units efficiently, maintaining the system's performance. In the chemical industry, it is used for the transport of activated carbon in chemical processing plants, where it is used as a catalyst or adsorbent in various reactions. The food and beverage industry also utilizes pneumatic conveying for activated carbon in filtration processes, ensuring the removal of impurities and contaminants from products. The equipment's ability to handle different material characteristics makes it suitable for a broad range of industrial applications, from small-scale laboratory operations to large-scale industrial plants.
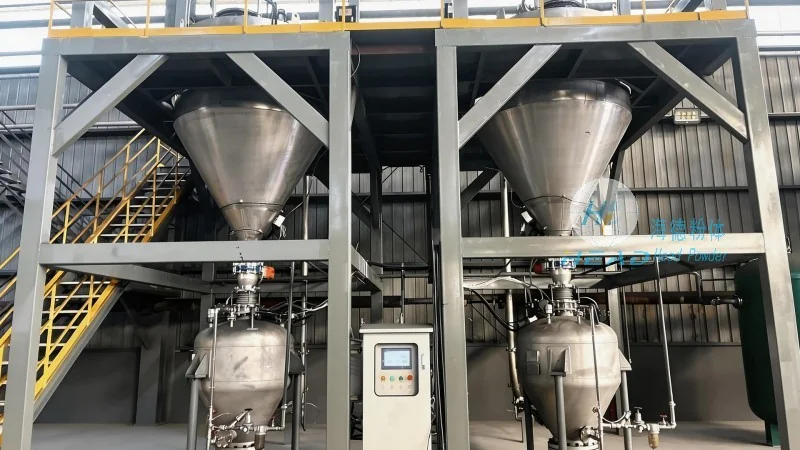
To achieve optimal performance from activated carbon pneumatic conveying equipment, several factors must be considered. The first is the selection of the appropriate conveying system type, whether dilute or dense phase, based on the specific application requirements. The system design must account for the material's properties, such as particle size, density, and moisture content, to ensure efficient transport. The pipeline diameter and length are critical parameters that affect the air velocity and pressure required for conveying. Proper maintenance of the equipment, including regular cleaning of the pipeline and replacement of worn components, is essential to prevent system inefficiencies and downtime. The control system must be reliable and capable of monitoring and adjusting the system parameters in real-time to maintain stable operation. Additionally, the selection of the blower or air compressor must be matched to the system's requirements, ensuring sufficient air pressure and flow rate without excessive energy consumption.
Activated carbon pneumatic conveying equipment is a vital component in industrial processes that rely on activated carbon for adsorption and purification. By understanding the fundamental principles and key components of these systems, operators can ensure efficient and reliable material transport, maintaining system performance and operational efficiency. The advantages of pneumatic conveying, including flexibility, long-distance transport, and reduced material degradation, make it a preferred choice over traditional mechanical methods. With proper design, maintenance, and control, activated carbon pneumatic conveying systems can provide consistent performance, supporting the success of various industrial applications. As the demand for activated carbon in environmental and industrial processes continues to grow, the importance of efficient conveying equipment will remain significant, driving further advancements in system design and technology.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top