Understanding the working principles of pneumatic conveying systems, especially when applied to the transportation of brown sugar, is crucial for industries dealing with bulk powder handling. This article delves into the mechanics and operational aspects of such systems, providing a comprehensive overview for professionals in the field.
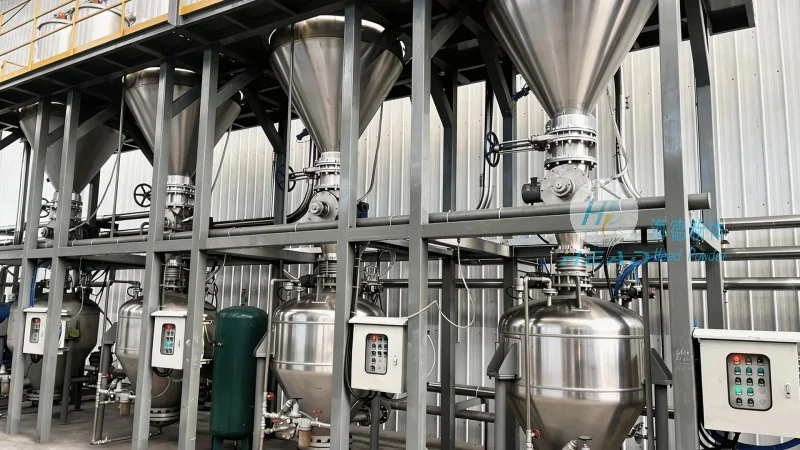
Pneumatic conveying, or air-based powder transport, is a method used to move dry bulk materials like brown sugar through a pipeline using pressurized or suction air. This technology offers several advantages over traditional mechanical conveying methods, including reduced equipment wear, lower maintenance costs, and the ability to handle materials that are sensitive to contamination or degradation. For the food industry, particularly in the processing of brown sugar, maintaining product quality and hygiene is paramount, making pneumatic conveying an ideal solution.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of specialized powder handling solutions. With operations based in Shandong, China, the company has established itself as a trusted partner in the design, manufacturing, and implementation of pneumatic conveying systems tailored to the unique needs of various industries, including food processing. The company’s expertise lies in understanding the specific challenges associated with transporting delicate or high-value materials like brown sugar, ensuring efficient and reliable operation.
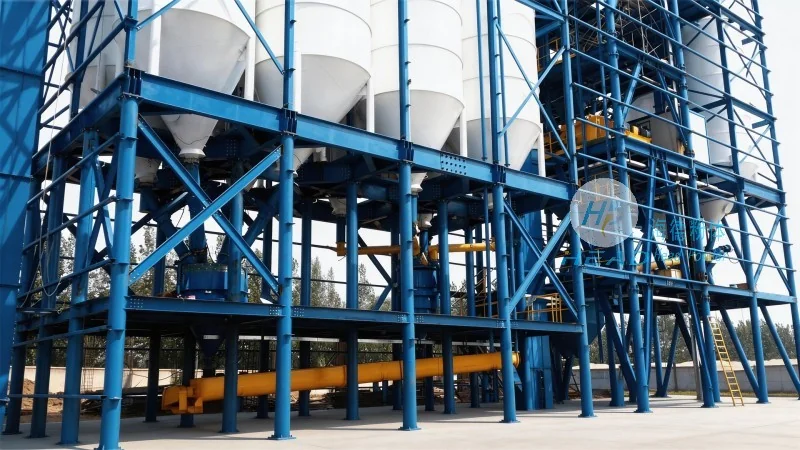
The core of a pneumatic conveying system involves the use of air to create a flow that transports the powder. There are two primary types of pneumatic conveying: dilute phase and dense phase. Dilute phase systems use low air velocities to move particles in a relatively dispersed state, suitable for shorter distances and lower material loads. Dense phase systems, on the other hand, employ higher air pressures and lower velocities to transport materials in a more concentrated form, which is ideal for longer distances and higher material volumes.
In the context of brown sugar, the choice of system depends on factors such as the distance between the source and destination, the volume of sugar to be transported, and the required flow rate. For example, a dilute phase system might be used for short-distance transfers within a sugar processing plant, while a dense phase system could be employed for longer-distance transportation from a factory to a warehouse or distribution center.
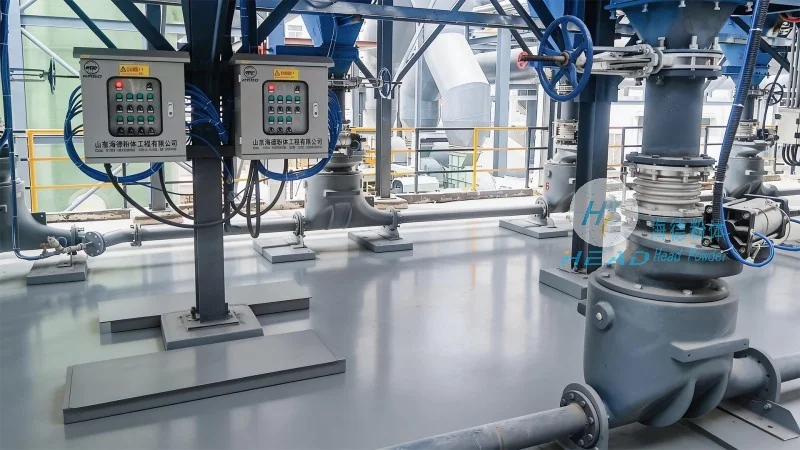
A typical pneumatic conveying system consists of several key components that work in tandem to ensure efficient material transport. These include the material feed hopper, which holds the brown sugar and controls the flow rate; the air compressor or vacuum pump, which generates the necessary air pressure or suction; the pipeline system, which carries both the air and the sugar particles; and the discharge device, which delivers the sugar to the final destination. Additionally, filters and cyclones are often included to separate the air from the powder, ensuring that the air is clean and the powder remains free of contaminants.
Implementing a pneumatic conveying system for brown sugar offers numerous benefits. Firstly, it minimizes product exposure to external elements, reducing the risk of moisture absorption or contamination. Secondly, the system is highly flexible, allowing for changes in the flow rate or direction without significant modifications to the infrastructure. Thirdly, it can handle varying particle sizes and moisture contents, making it suitable for different types of brown sugar, from raw to refined products. Lastly, the system is relatively compact and can be integrated into existing processing lines, saving space and reducing installation costs.
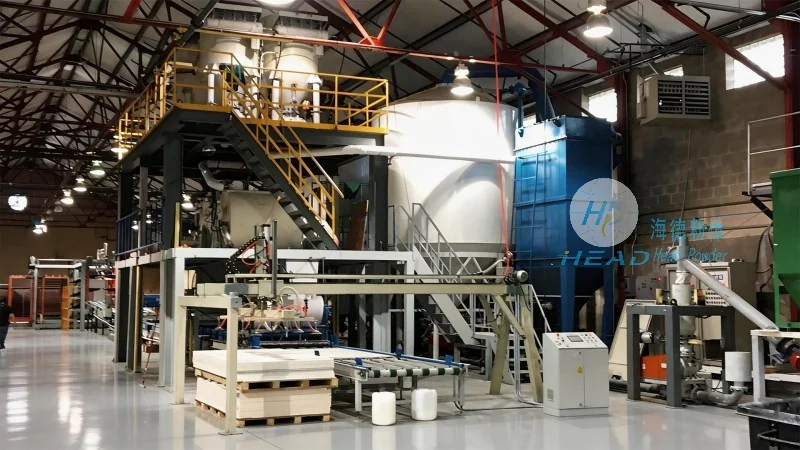
Pneumatic conveying systems are widely used in various stages of brown sugar production and processing. For instance, in a sugar refinery, the system can be used to transport raw sugar from storage silos to processing equipment, or to move finished brown sugar from the production line to packaging facilities. In a food processing plant, the system may be employed to convey brown sugar from a mixing area to a storage silo or to a packaging line for final product assembly. The versatility of pneumatic conveying makes it a valuable asset in optimizing workflow and enhancing operational efficiency in brown sugar handling operations.
Pneumatic conveying represents a sophisticated and efficient method for transporting brown sugar and other bulk powders. By understanding the working principles and components of such systems, industries can make informed decisions about implementing the right technology to meet their specific requirements. With companies like Shandong HeadPowder Engineering Co., Ltd. providing expert solutions, the adoption of pneumatic conveying systems continues to grow, offering significant advantages in terms of product quality, operational efficiency, and cost-effectiveness for the brown sugar industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top