For industrial applications involving maltose, efficient material handling is crucial. Pneumatic conveying systems offer a reliable solution for transporting maltose, with various types and features tailored to specific operational needs. This article explores the different types of maltose pneumatic conveying, their key characteristics, and the diverse applications where they are commonly employed.
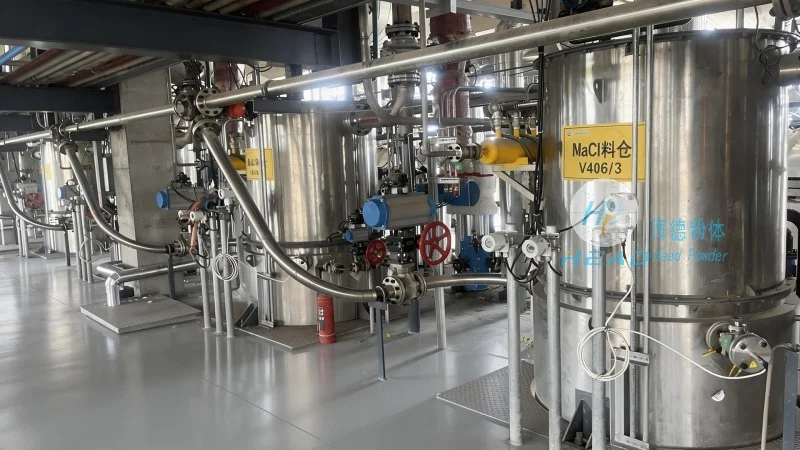
Maltose, a disaccharide sugar derived from starch hydrolysis, is widely used in the food, pharmaceutical, and chemical industries. Its granular or powdered form requires specialized handling to ensure product integrity and operational efficiency. Pneumatic conveying systems utilize air or gas to transport maltose particles, eliminating the need for mechanical components like belts or buckets. This method is particularly advantageous for handling hygroscopic or sensitive materials like maltose, as it minimizes product degradation and contamination.
There are primarily two types of pneumatic conveying systems used for maltose: suction (or vacuum) conveying and pressure conveying. Each type has distinct characteristics and is suited to different operational scenarios.
Suction conveying systems operate by creating a negative pressure at the material inlet, drawing maltose particles into the system. This type is ideal for applications where the material source is at a lower elevation than the destination, or when the material needs to be collected from multiple points. The system typically includes a vacuum pump, a hopper for material storage, and a conveying line that transports the maltose to the processing unit. Suction conveying is often used in situations where the material is light and requires gentle handling to prevent breakage or agglomeration.
Pressure conveying systems generate positive pressure at the material discharge point, pushing maltose particles through the conveying line. This method is suitable for applications where the material source is at a higher elevation or when the material needs to be transported over longer distances. The system consists of a blower or compressor, a hopper, and a pressure line that delivers the maltose to the processing area. Pressure conveying is commonly used for bulk material transport, as it can handle higher material flow rates and is more efficient for long-distance transport.
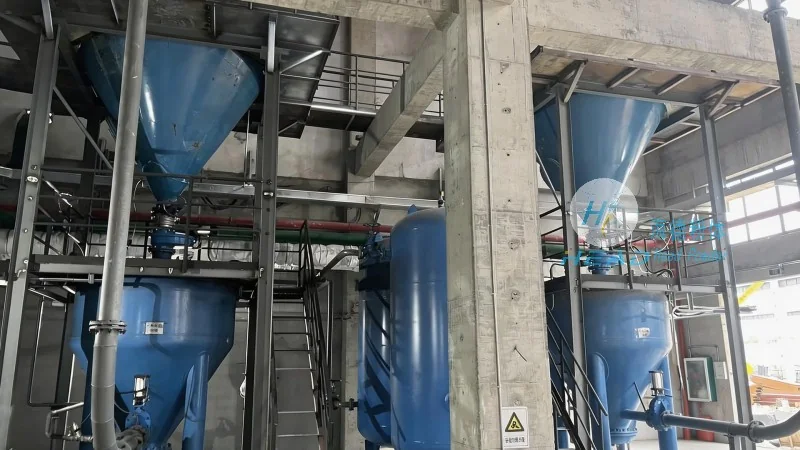
Regardless of the type, modern maltose pneumatic conveying systems share several key features that enhance performance and reliability. These features include:
Maltose is a hygroscopic and sensitive material, making it susceptible to breakage or clumping during handling. Pneumatic conveying systems use air to move particles, reducing the risk of mechanical damage. The low impact and controlled flow rates ensure that the maltose retains its quality and granular structure, which is critical for downstream processing.
Pneumatic conveying systems are enclosed, preventing external contaminants from entering the material stream. This is particularly important for food-grade maltose, where contamination can lead to product recalls or safety issues. The sealed system also helps maintain the product's moisture content and prevents exposure to air, which could cause oxidation or spoilage.
Maltose pneumatic conveying systems can handle a wide range of particle sizes and moisture levels. They are adaptable to different production volumes, from small-scale batch processing to large-scale continuous operations. The flexibility of these systems allows manufacturers to integrate them into existing production lines without significant modifications.
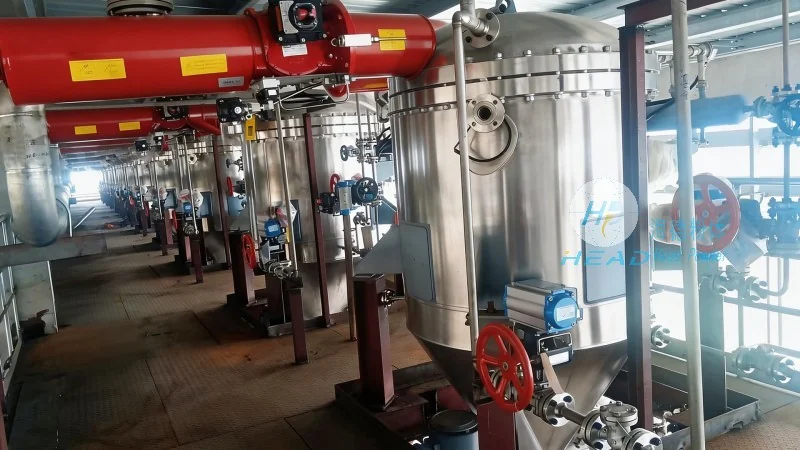
Modern pneumatic conveying systems are designed to be energy-efficient, reducing operational costs. The use of high-efficiency blowers and optimized air flow rates minimizes energy consumption while maintaining effective material transport. This is especially beneficial for large-scale maltose processing facilities, where energy costs can significantly impact overall profitability.
Maltose pneumatic conveying systems are widely used in various industries due to their ability to handle sensitive materials efficiently. The primary applications include:
In the food industry, maltose is used as a sweetener and flavor enhancer in beverages, baked goods, and confectionery products. Pneumatic conveying systems are used to transport maltose from storage silos to mixing and packaging lines. This ensures that the product is delivered in a clean, hygienic manner, meeting the strict quality standards required for food-grade applications.
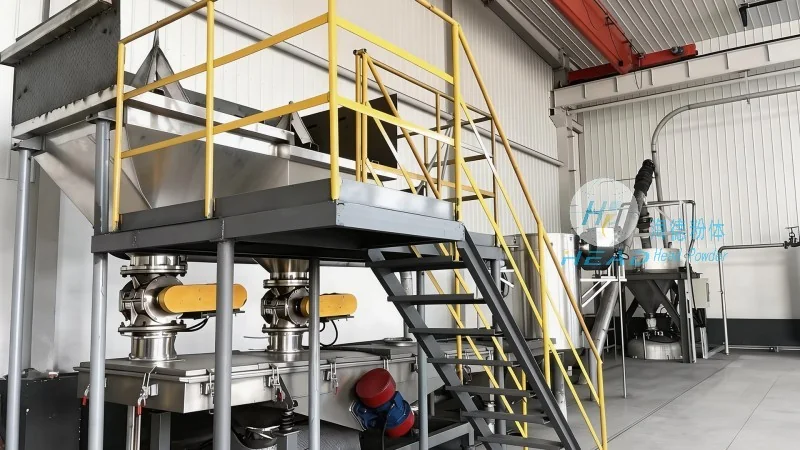
Pharmaceutical manufacturers use maltose as an excipient in drug formulations. Pneumatic conveying systems are employed to transport maltose powders into mixing tanks and granulation equipment. The gentle handling and contamination control features of these systems are essential for maintaining the purity and stability of pharmaceutical products.
In the chemical sector, maltose is used as a raw material in the production of other chemicals or as a feedstock in industrial processes. Pneumatic conveying systems are used to transport maltose from storage tanks to reactors and processing units. The ability to handle bulk quantities and maintain product integrity makes these systems ideal for chemical processing applications.
Maltose is also used in animal feed formulations as a source of energy. Pneumatic conveying systems are used to transport maltose powders into feed mixing and pelletizing equipment. The efficient and hygienic transport of maltose ensures that animal feed products meet nutritional requirements and are free from contaminants.
Maltose pneumatic conveying systems offer a reliable and efficient solution for handling maltose in various industrial applications. The different types of systems—suction and pressure—provide flexibility to meet specific operational needs, while key features such as gentle handling, minimal contamination, and energy efficiency enhance overall performance. By understanding the characteristics and applications of these systems, manufacturers can optimize their material handling processes and improve product quality. As a leading provider of engineering solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique requirements of maltose processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top